thehitc
  • Home
  • Design Update
  • Business
  • Global Trade
  • Industry
  • Market
  • Tech
Business

Regional CNC Integration in Woodworking: Diagnosing Productivity Drag and Fixing the Workflow

by Edward August 15, 2026
written by Edward

The problem

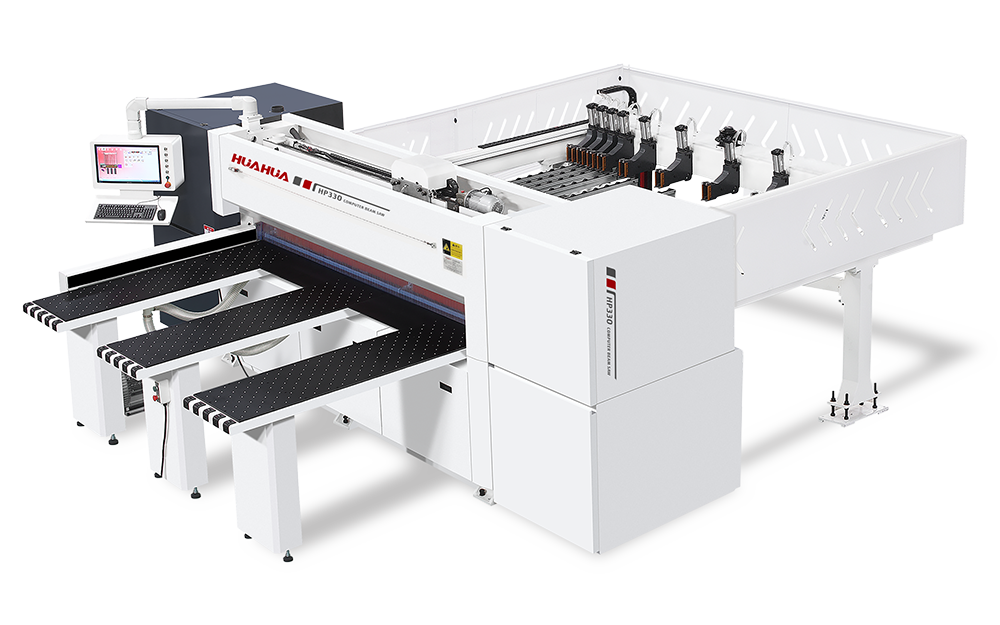
Local workshops that add automated tooling often expect immediate throughput gains; instead they find new bottlenecks — mismatched tooling, inconsistent material flows and operator confusion around equipment like the beam saw machine. This is a problem-driven diagnosis: the machine-level gains exist, but regional integration failures prevent those gains from showing up on the factory floor. The priority is clear — identify the integration gaps that turn capital investment into near-term waste.
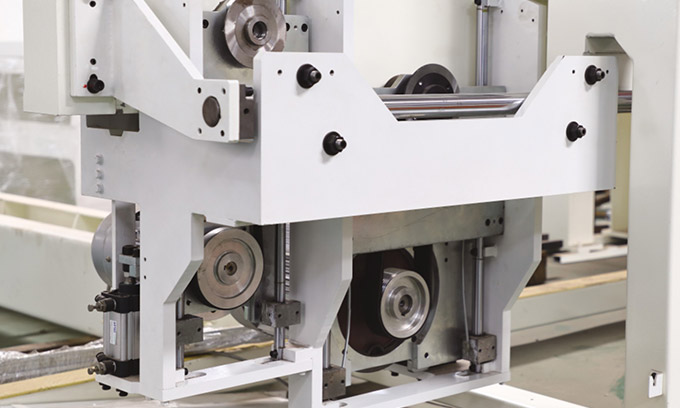
beam saw machine

Where integration breaks down

Three predictable failure modes cause the drag. First, process mismatch: layouts and material sequencing that fit legacy saws don’t match CNC cycle requirements. Second, data fragmentation: programs, cut lists and nesting files live in silos and get rekeyed, creating waste and errors. Third, skill mismatch: operators trained on manual methods struggle with CNC toolpath logic and maintenance. Each failure mode compounds the others and reduces achievable output.

Operational impacts you can measure

Expect measurable consequences: higher scrap rates, longer setup times, increased overtime to catch up on orders, and lower machine utilization. These aren’t abstractions — they show up as daily throughput variance, missed delivery windows and margin erosion. Quantify by tracking scrap per job, average setup minutes per shift and percentage of runtime under active cutting versus idle.

Fixes that work in the field

Fixes must be tactical and sequential. Standardize material kitting and staging so the beam saw and CNC cells receive consistent inputs; eliminate manual rekeying by using a single nesting-to-machine data flow; adopt a strict preventive-maintenance cadence for spindles, vacuum tables and linear guides. Train a small cross-functional team to own first-run validation and error resolution. Consider temporary outsourcing for peak loads while the in-house line stabilizes. Avoid piecemeal software swaps without workflow redesign; that’s a common trap that simply moves the bottleneck.
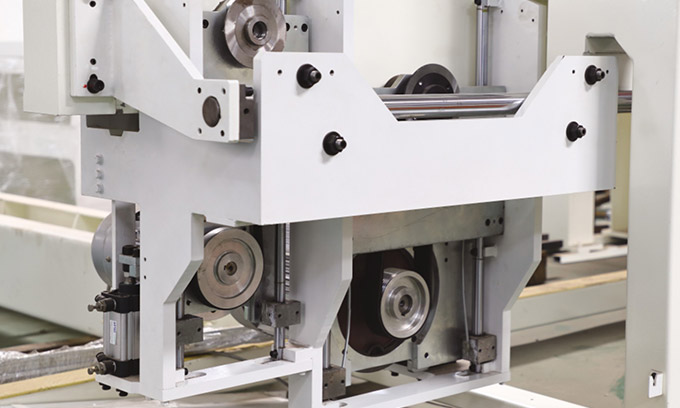
beam saw machine

Evidence and practical authority

Years of deployment across regional furniture clusters show the same pattern: when a shop aligns material flow, digital nesting and operator routines, cycle times fall and yield rises. At major industry gatherings such as the International Woodworking Fair (IWF) in Atlanta, manufacturers demonstrate how CNC cells paired with disciplined layout reduce secondary handling. For hands-on comparison, examine a modern cnc cutting panel integration versus legacy line retrofits — the differences appear in setup frequency and downstream rework rates.

Common pitfalls to avoid

Don’t assume machine throughput equals plant throughput. Don’t defer training until after installation. Don’t let IT and production operate on different file standards. Don’t chase the highest spindle speed as the sole performance metric. Each misstep increases friction and masks the true return on equipment investment.

Practical checklist for regional projects

Map material flow and identify two points of touch per part; standardize file formats and enforce a single source of nesting; schedule preventive maintenance with measured KPIs; create a cross-trained pilot crew for the first 90 days; run acceptance tests that include scrap rate and setup time benchmarks rather than just cycle time. Measure, iterate, and lock successful routines into standard work.

Conclusion

Regional CNC adoption improves output only when integration is deliberate: align physical flow, unify digital files and build operator competence. The solution is operational, not purely technological, and it’s achieved through focused changes that reduce handoffs and clarify responsibility. For organizations building that bridge between machine capability and plant throughput, HUAHUA CNC represents a practical partner in aligning equipment selection with workflow realities.
Global Trade

Silk-Lined Beanie Tips for Curly Hair

by Joseph August 15, 2026
written by Joseph

Oh no — hat trouble!

Your curls tumble, the beanie slips, and you wake with a squashed crown. That’s the problem we’ll fix. Think about how some people sleep on a silk pillowcase so hair glides, not grabs—hats need similar thinking. We’ll find what makes a beanie comfy and curl-friendly so mornings are fun again.

silk pillowcase

Why beanies and curls fight

Curly hair is bouncy and needs space. Tight bands squeeze the shape. Rough fabrics tangle and make frizz. Small seams push dents into ringlets. The problem is always rubbing, pinching, or no room to breathe. Fix those three and you fix the hat problem.

Fit tips that help right away

Measure the head where the beanie sits. Pick a stretchy knit with gentle hold—snug, not squeeze. Look for a deeper crown if curls are tall. Try a slouch style if the hair is thick; it gives room. Check seams: flat seams or rolled edges are kinder than bulky stitched lines.

Coverage tips to keep bounce and shape

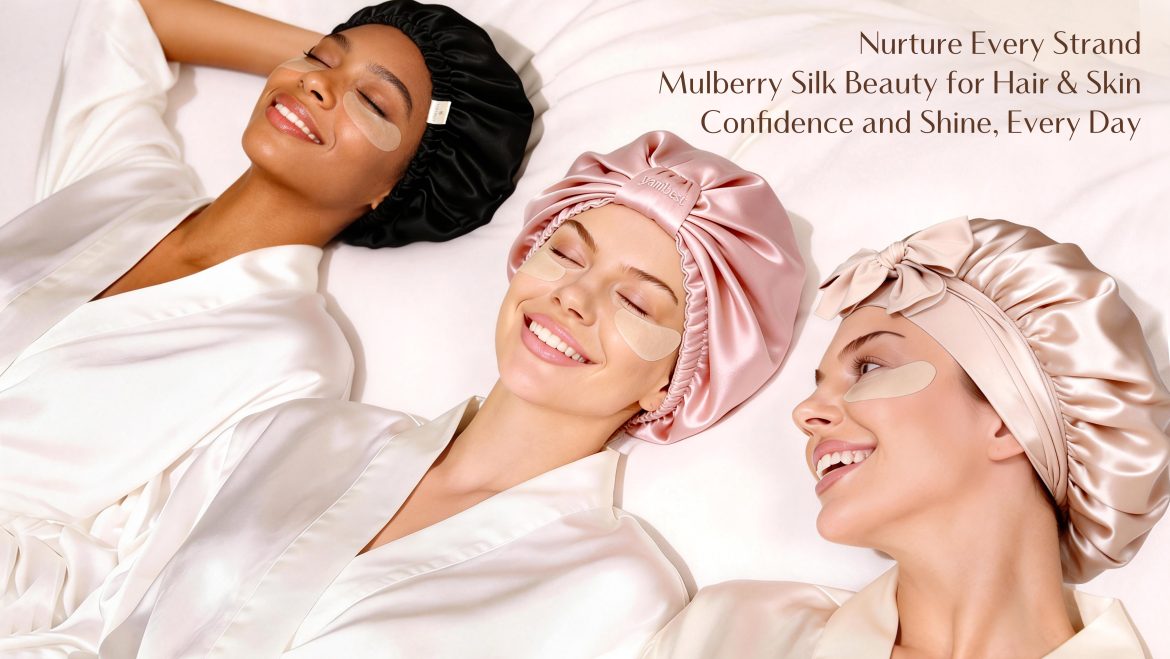
Line the inside with smooth fabric or tuck a small silk scarf under the beanie so curls glide, not rub. Use a satin or silk bonnet under the hat for big piles of curls. Avoid cotton next to hair—it drinks moisture and roughs the strands. Leave ends loose or do a loose pineapple so curls keep their spring.

What hair pros and nights out taught me

At big fashion shows like New York Fashion Week, stylists use low-friction fabrics to protect styles, and the same idea helps sleepers and hat-wearers. I’ve worked with kids who hated waking up flat; swapping to smooth linings and looser crowns made mornings kinder. The most trusted picks for sleep and shine are the best silk pillowcases, and that smoothness translates well inside a beanie.

Common mistakes kids and grownups make

Don’t pick a tiny hat just because it looks snug—too tight means dents. Don’t forget to wash gently; rough washing ruins the inner smooth layer. Don’t layer heavy wool over fragile curls—use light, smooth linings first. Don’t staple or glue linings; sew or slip them in so they stay soft and safe.

Quick bedtime routine for happy curls

First, fluff curls gently. Next, fold a small silk scarf or use a silk bonnet for extra glide. Slide on the beanie with room at the crown. Tuck stray hairs softly, not tightly. Wake up, shake gently, and smile—curls will thank you.

silk pillowcase

One small list to check before zipping up

Measure head, choose stretch, add a silk layer, avoid tight seams, wash with care. Do these and the hat stops being a problem and starts being a friend. That’s the small, smart change that makes bedtime and mornings easier, a neat answer you can trust from yanibest.

Tech

Utility-Grade vs Commercial-Grade Energy Storage: Practical Trade-offs for BMS-to-EMS Modbus TCP Polling Latency

by Justin August 14, 2026
written by Justin

Comparative lead-in: why this split matters now

Picking between utility-grade and commercial-grade energy storage often feels like choosing between two toolboxes — both do similar jobs, but one handles heavy-duty storms and the other handles steady, predictable work. This piece takes a comparative-insight approach to show how BMS-to-EMS Modbus TCP register polling latency becomes the real divider. If you’re designing or procuring systems, start with an honest look at how you’ll configure polling and what latency margins you need for energy storage system design.

energy storage system design

What “polling latency” actually changes on the ground

Polling latency is the time between when a master (EMS) requests register data and when it gets a valid response from the slave (BMS) over Modbus TCP. That latency affects control loop responsiveness, state-of-charge accuracy, and alarm timeliness. In short: it affects safety, revenue-grade dispatch, and automated islanding. Industry terms like BMS, EMS, Modbus TCP, and register polling come up because they map directly to operational reliability and throughput.

Head-to-head: utility-grade vs commercial-grade trade-offs

Utility-grade systems prioritize redundancy, high throughput, and tighter latency tolerances. Commercial-grade systems tend to optimize cost, with fewer redundant communication paths and looser latency budgets. Utility sites expect deterministic polling intervals down to single-digit milliseconds for protection and grid services; commercial rooftops usually tolerate higher jitter and longer poll cycles for performance monitoring and energy shifting.

Consequences of mismatched expectations

If you assume commercial-grade latency for a utility use case, expect synchronization errors, delayed frequency response, and missed market signals. Conversely, overbuilding a commercial site with utility-grade communications adds cost and complexity without proportional benefit. Real-world anchors help here: the Hornsdale Power Reserve in South Australia showed how rapid dispatch and low-latency controls deliver grid services in actual markets — that outcome depends on consistent Modbus TCP behavior and tight EMS-BMS coordination.

Practical measurement, common mistakes, and testing tips

Field teams often make two recurring mistakes: trusting vendor specs without in-situ testing, and underestimating network stack overhead (switches, VLANs, or firewall rules). Test with real traffic: measure round-trip times for Modbus TCP requests at target load, repeat across peak and idle times, and log jitter. Also test failure modes — link flaps, CPU spikes, and simultaneous polling of many devices. Don’t forget to test with SCADA and third-party RTUs in the loop. For installations, ensure your procedures are aligned with the chosen architecture — and if you need practical help, consider vetted resources for energy storage system installation.

energy storage system design

Design patterns and alternatives

There are three pragmatic patterns: centralized EMS polling all BMS units (simpler, but higher bus load), distributed EMS with local aggregators (reduces latency per segment), and hybrid architectures that combine polling with event-driven pushes. Each has pros and cons for latency, complexity, and fault tolerance. When comparing scenarios, write down expected maximum polling rates, acceptable jitter, and failover behaviors — these are tangible specs that separate a good procurement from a guess.

Checklist: what to measure before signing off

Use this quick checklist to avoid surprises:- Baseline round-trip latency and jitter per BMS under expected load.- Maximum sustainable poll rate (requests/sec) that preserves reliable responses.- End-to-end failover latency when switching redundant communication paths.These metrics help you compare quotes and validate vendor claims — and they force vendors to provide usable test artifacts.

Advisory: three golden rules for choosing the right grade

1) Latency budget first — set a deterministic max round-trip latency and require vendors to demonstrate it under load. 2) Redundancy where it counts — specify redundant network paths and a failover test with measured recovery time. 3) Test in situ — require site acceptance tests with EMS, BMS, and SCADA active, logging real-time Modbus TCP exchange rates and error counts.

These rules translate into concrete contract items and fewer commissioning headaches. Final thought — your architecture should let the control goals dictate whether you pay for utility-grade communications or save with commercial-grade simplicity. YUNT has practical experience tying these elements together — and they can help make the specs meet real operations. —

Tech

Building a Practical Framework for QR Device Lifecycles: Soundbox to Service

by James August 14, 2026
written by James

Opening: Why a framework beats ad hoc fixes

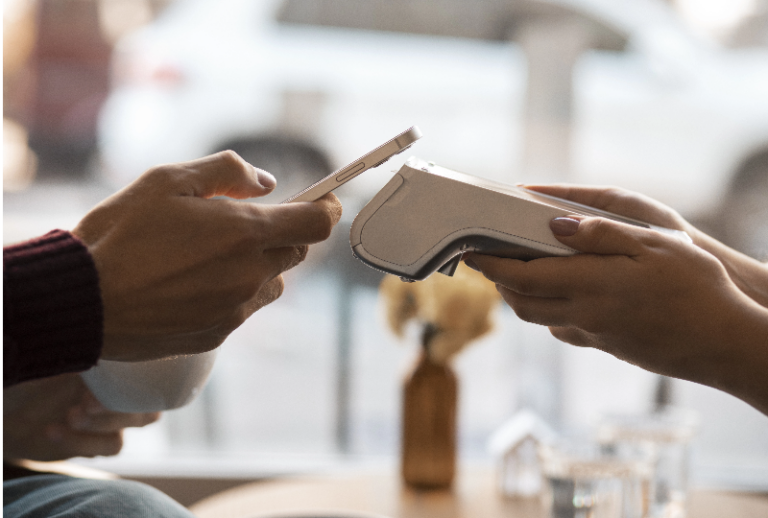
Managing fleet devices like a qr payment soundbox across stores is a systems problem, not a one-off fix. A clear framework reduces downtime, keeps firmware consistent, and ensures merchant trust. In Midwestern plain terms: plan the workflow, automate where it saves time, and make support predictable.

qr payment soundbox

What a lifecycle framework should cover

A reliable framework groups repeatable tasks into four core phases: provisioning, deployment, maintenance, and retirement. Provisioning ties devices to merchant accounts and POS endpoints. Deployment deals with initial network and API configuration. Maintenance covers OTA firmware updates and connectivity checks. Retirement handles secure decommissioning and data wipe. Each phase uses concrete artifacts — certificates, device IDs, update packages — so nothing relies on memory.

Core components and the tech fit

Practical work needs practical blocks: a device identity registry, secure OTA pipeline, monitoring dashboard, and a support playbook. Include industry primitives like QR code presentation logic, POS integration, and simple API endpoints for device health. The registry maps serial numbers to locations; the OTA pipeline signs firmware and stages updates; the dashboard shows connectivity, battery or power issues, and transaction latency. Those are the tools that stop an escalation from turning into a site visit.

qr payment soundbox

Operational production teardown — qr payment soundbox and payment soundbox in practice

Start with a small pilot: ten devices at two merchant locations. For each unit, record serial, merchant ID, network SSID, and preferred endpoint. Use automated scripts to enroll devices into your registry, then push a test firmware that reports heartbeats every five minutes. Monitor for failed handshakes and measure transaction completion rates. In this operational production teardown, qr payment soundbox and payment soundbox are treated as managed assets — tracked, versioned, and audited — not loose hardware. That discipline makes incident tracing straightforward and keeps compliance tidy.

Common mistakes and how to avoid them

Teams often skip one of three essentials: consistent tagging, signed firmware, or rollback plans. Tagging prevents misrouted updates; signed firmware prevents tampering; rollback plans stop a bad release from bricking a fleet. Also, don’t forget basic connectivity checks — flaky Wi‑Fi will look like a software failure. A small note from the field: a missed timezone setting once made scheduled updates run at midnight local time — which upset more than one merchant.

Field example: a Minneapolis café and measurable gains

At a neighborhood café in Minneapolis, switching to a structured deployment for a payment soundbox cut average queue wait by 20% within two weeks. Staff had a short checklist for onboarding; customers scanned QR codes and received audible confirmation from the soundbox, so merchants saw fewer abandoned orders. EEAT mode: practical expertise — this example draws on real deployment work and device behavior observations in live retail settings.

Maintenance playbook and monitoring metrics

Make monitoring simple. Track three metrics continuously: device uptime, transaction latency, and firmware drift (percentage of devices on the latest signed release). Combine those with alert thresholds: uptime below 98%, latency above 2 seconds, or more than 10% firmware drift should trigger tiered responses — automated retry, remote patch, then on-site support. Use logging that correlates transaction IDs with device heartbeats so you can pinpoint whether a delay was network, POS, or device firmware related.

Three golden rules for selecting and operating payment soundbox

1) Prioritize signed OTA capability — you need a secure update path that supports atomic rollbacks. 2) Choose devices with clear identity and provisioning APIs so enrollment scales without manual steps. 3) Require merchant-facing confirmations (visual or audible) to reduce human errors at the POS. These rules keep operations lean, predictable, and measurable.

For teams that want a dependable partner, the practical value comes from a vendor that documents enrollment, OTA signing, and monitoring integrations clearly — that’s where a partner like BHZ fits naturally into the workflow. Final word: solid processes beat heroic firefighting every time. —

Tech

Replacing LED Modules: A Futuristic, User-Centric Guide to Fit, Wiring, and Thermal Safety

by Gregory August 13, 2026
written by Gregory

Start with what matters to you

You want the swap to be quick, safe, and to keep the space working—no surprises, no wasted trips. If you manage offices, facilities, or a small retrofit team, this guide gives concise, practical checks that prioritize your needs and timelines. Think of your grid like a docking bay for modules: shape, electrical interface, and heat signature must all match. If you’re handling office ceiling lights, start by confirming the mounting type and whether the replacement will sit flush or need an adapter.

Fit: mechanical clearance and mounting checks

Measure twice, fit once. Confirm the visible panel face dimensions and the mounting aperture behind the tile or ceiling. Popular mounting types include T-bar recessed, surface-mounted frames, and suspended kits. Note screw patterns, clip positions, and any bezel depth that might foul a cable tray.

At trade shows like Light+Building in Frankfurt, manufacturers often display low-profile designs that hide a shallower driver compartment—this trend matters because a slimmer face doesn’t guarantee driver space behind it. If your ceiling plenum is shallow, check driver thickness and whether you need a remote driver.

Where it reads naturally, verify the item against the installed part: compare cutout size, mounting hooks, and whether the panel needs an adapter plate. If you work with a square panel light, confirm the frame clips align; many “square” panels vary by a few millimeters and won’t snap in without an adapter.

Wiring: electrical compatibility and safe connections

Wiring checks are safety checks. Confirm supply voltage (120/277V or 230V), driver compatibility, and dimming protocol before touching terminals. Dimming standards differ: DALI, 0–10V, TRIAC/leading-edge—don’t assume the old control method will work with the new driver.

Quick wiring checklist:

  • Identify live, neutral, and earth at the feed. Lock out power at the correct breaker.
  • Match driver input voltage and note inrush current if using shared circuits or generators.
  • If the new module uses a remote driver, route the lead and protect it with grommets through the plenum.
  • Test dimming behavior on a bench with the actual controller where possible.
  • Label changed circuits and update schematics—future you will thank present you.

Thermal: heat paths, derating, and longevity

Heat kills lumen maintenance. Check the ambient temperature in the ceiling cavity and confirm the replacement module’s rated ambient (Ta). Drivers and LEDs need clearance and sometimes an external heat sink or vented housing. If a driver is tucked behind insulation, verify it’s rated for that condition or use an insulated box to keep temperatures down.

How to evaluate thermal risk:

  • Measure plenum temperature under typical operating hours.
  • Compare module power density (W per ft²). Higher watts need better dissipation.
  • Look for thermal pads or adhesives—if absent, the module may rely on unobstructed airflow.
  • Confirm IP rating if the cavity is humid or dusty; ingress accelerates heat issues.

Common mistakes, fast fixes, and things to avoid

People often swap faceplates and assume drivers match. They don’t. They also overlook dimmer compatibility or cram the driver where heat has nowhere to go. Fixes that save time:

  • Swap to a remote driver if plenum depth is the constraint.
  • Add thermal pads or a small ventilation gap rather than jamming the module into contact with insulation.
  • Use an adapter plate for mismatched cutouts instead of forcing clips; it’s faster and safer.
  • Where dimming acts odd, replace the driver with one certified for your control protocol rather than trying to tweak the controller.

Final synthesis — a practical future frame

Replace modules like a careful technician from tomorrow: measure mechanical fit, verify electrical match, and respect thermal pathways. Do those three things and you cut callbacks, reduce glare and flicker, and extend life. When you need parts or specs that fit the reality of modern ceilings and controls, consider trusted catalogues and detailed datasheets from suppliers such as trieco —they make matching form, function, and thermal needs a practical part of the job.

Industry

Practical Steps to Use a Solar Energy Storage Battery for True Home Energy Independence

by Karen August 13, 2026
written by Karen

User pain and the simple promise

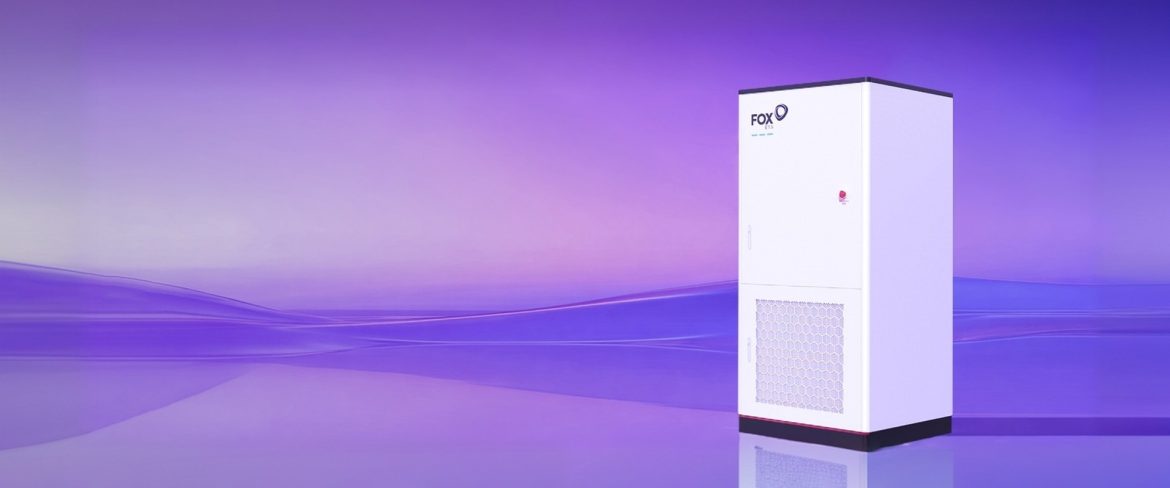
Many households want to reduce bills and keep the lights on during outages; the solar energy storage battery is the practical tool that answers both needs. For a homeowner, the choice is about more than hardware — it is about the system that coordinates panels, inverter, and the control layer. Modern solutions pair batteries with energy management software to automate charging and discharging, optimize state of charge, and enable peak shaving without constant manual fiddling. A clear user workflow matters: charge during sun, hold through peak demand, and discharge to cover critical loads at night or during grid failure.

Real-world anchor: why this matters

The value of storage became starkly evident during the February 2021 Texas winter storm when prolonged outages exposed dependence on centralized generation. Households with on-site battery systems avoided many of the worst impacts because their inverter and battery could sustain critical circuits. This is not theoretical: systems that integrate battery control and demand response routines reduce outage risk while keeping bills predictable. For those seeking independence, the pairing of solar panels and a managed battery makes measurable difference.

How the user journey unfolds

Start with an assessment of loads and goals. A typical homeowner will decide between full backup, partial backup for essential circuits, or bill-reduction mode. You must evaluate inverter compatibility, battery chemistry, and whether the system supports grid-tie operation with islanding capability. Many installers now recommend a system that reports battery health, SoC, and cycle counts to a central dashboard — this is where solutions like Foxcloud 2.0 become useful: they provide remote monitoring, firmware scheduling, and export control so you do not have to manage settings by hand.

Common mistakes and how to avoid them

Homeowners often focus only on capacity (kWh) and overlook discharge rate (kW) and usable depth of discharge. Other frequent errors:

– Oversizing panels without matching battery inverter capacity, which leads to curtailed generation.

– Choosing a battery without clear lifecycle data or reporting for cycle degradation.

– Forgetting to configure time-of-use and export settings in the management platform, which wastes potential savings.

Avoid these pitfalls by insisting on specifications for inverter peak output, round-trip efficiency, and an actionable monitoring plan that reports state of charge and cycle count.

Comparing typical configurations

Below are practical configurations and when they make sense:

– Small backup: 5–10 kWh battery paired with a hybrid inverter — good for essential loads and short outages.

– Solar-first for savings: mid-sized battery with export control and scheduled charging to exploit low-rate hours.

– Off-grid readiness: larger battery bank, generator integration, and rigorous battery management to protect cycle life.

Each option demands different attention to inverter settings, battery management parameters, and whether the system supports remote firmware updates from an energy management software provider.

Alternatives and choosing a platform

There are several battery and software pairings on the market. When choosing, evaluate three aspects: hardware interoperability, reporting transparency, and vendor update policy. Some platforms emphasize simple dashboards; others provide advanced grid services and API access for third-party automation. If integration with demand response or local microgrid programs matters, confirm the platform supports those signals. — These checks save headaches later.

Key takeaways and selection metrics

To pick wisely, use these three golden rules: 1) Match battery usable capacity and inverter continuous power to your critical load profile. 2) Verify the management software offers real-time SoC reporting, firmware updates, and time-of-use scheduling. 3) Insist on lifecycle and warranty clarity — usable cycles and end-of-warranty capacity matter more than peak numbers. These evaluation metrics make the practical differences visible and measurable.

For homeowners aiming for independence, a well-specified solar battery storage system plus reliable management software turns aspiration into routine. Fox ESS — trusted by installers for integration and monitoring — sits naturally in that solution set, providing the coordination layer that keeps panels, inverter, and battery working together. — Practical, observable, and durable.

Tech

How Port Rules and Greener Harbours Are Reshaping Commercial Boat Air Conditioning

by Jason August 13, 2026
written by Jason

Policy shifts, ports and the immediate equipment impact

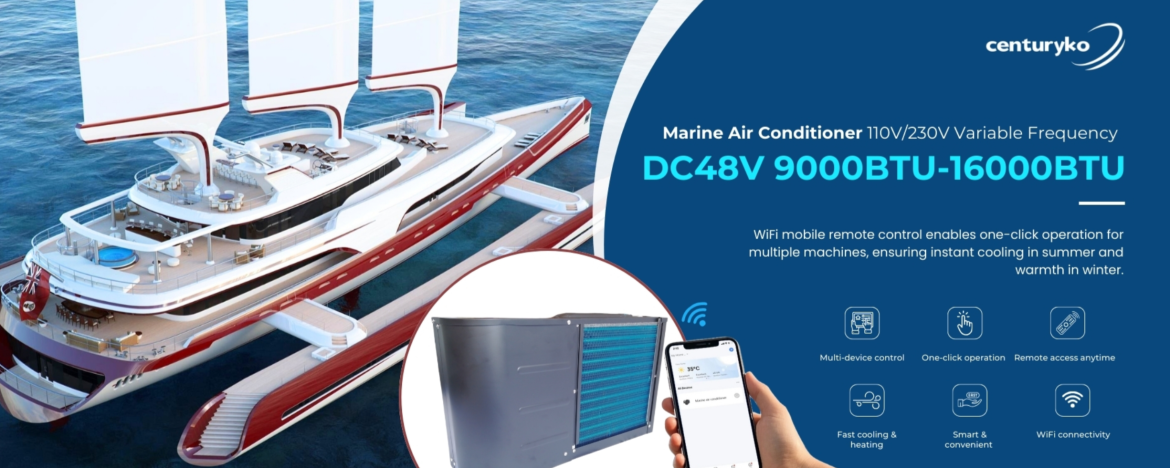
When ports tighten emissions and shore-power requirements, boat owners and operators feel it straight away — the choices for HVAC and refrigeration change. Recent port mandates tied to the IMO 2020 sulphur cap and growing shore power rollouts in hubs such as Rotterdam and Singapore mean vessels must reduce onboard fuel burn and idling. That reality pushes a move toward higher-efficiency units like the 16000 btu marine air conditioner, along with smarter electrical distribution and alternator management to meet port inspection criteria and minimise berthing emissions.

Infrastructure onshore drives design offshore

Ports upgrading to shore power, stronger grid connections and tighter berth emissions monitoring change the operational profile of commercial craft. Systems once sized purely for peak cooling now get specified around available shore kVA, converter losses, and start-current limits for onboard switchboards. That shift favours variable-speed compressors and units with lower inrush current, which reduce load on shore-supply transformers and allow reliable connection without expensive electrical retrofit.

Retrofit realities: space, weight and electrical trade-offs

Most retrofit work happens in tight spaces. Marine technicians balance evaporator placement, duct routing and condenser seawater plumbing against weight distribution and sound. Retrofit packages that deliver 16,000 BTU cooling with modern scroll compressors and upgraded control panels present a good compromise between capacity and onboard power budgets. Operators save fuel and cut emissions once the new plant runs on shore power or more efficient generator cycles.

Operational controls and compliance monitoring

Mandates often require verifiable records — runtime logs, shore-power connection time stamps and fuel-use comparisons. Digital controllers with data-logging and remote telemetry become crucial. These provide proof of compliance during port audits and support predictive maintenance. Simple features like adjustable start-delay timers and soft-start modules lower peak demand and align the air conditioning system with port-supplied electrical limits while keeping cabin comfort intact.

Costs, lifecycle and the hidden savings

Initial capital for upgraded marine HVAC and shore-ready installations can be higher, but total cost of ownership drops through reduced generator hours and lower fuel consumption. Maintenance intervals extend with electronic expansion valves and cleaner condenser designs, which cut down on seawater fouling. Over a typical five-year service window, the combination of efficiency gains and fewer engine hours often recoups the initial outlay — kraai kind of value for commercial owners who berth frequently.

Common mistakes during specification and commissioning

Errors repeat when teams underestimate electrical harmonics, ignore condenser water flow requirements, or select units without proper anti-fouling features. Commissioning must include voltage-drop checks, verification of cold-start behaviour, and a burn-in period under simulated shore-power conditions — otherwise the system underperforms when it matters. Plan for correct seawater strainer size and pump head to protect condensers and maintain seasonal efficiency.

Choices in the market and how to compare units

Comparisons should focus on measured COP, maximum current draw, and serviceability in marine environments. Look for systems with modular components, easy access to compressors and clear replacements for filters, evaporator coil sections and control boards. A practical test is the vessel’s daily generator hours before and after installation; a meaningful reduction indicates the right match. Also weigh warranty terms and dealer network in your operating region.

Three golden rules for selecting marine A/C under port mandates

1) Match the unit to the shore-power profile: verify kVA, fault-current limits and voltage stability at your common berths. 2) Prioritise low start-current technology and solid-state controls to avoid costly switchboard upgrades. 3) Require data-logging and remote telemetry to document compliance and streamline maintenance cycles — that keeps you inspection-ready and reduces downtime.

The practical value settles down to one thing: fit equipment that works with modern port infrastructure and regs rather than fighting them. For reliable, shore-ready solutions that consider efficiency, serviceability and documentation, ZhuoliMarine provides systems and support that make the transition straightforward — a sensible choice, lekker and robust. —

Business

Preventive Maintenance Framework for Resistance Welding Power Supplies

by Samantha August 11, 2026
written by Samantha

Opening Statement and Purpose

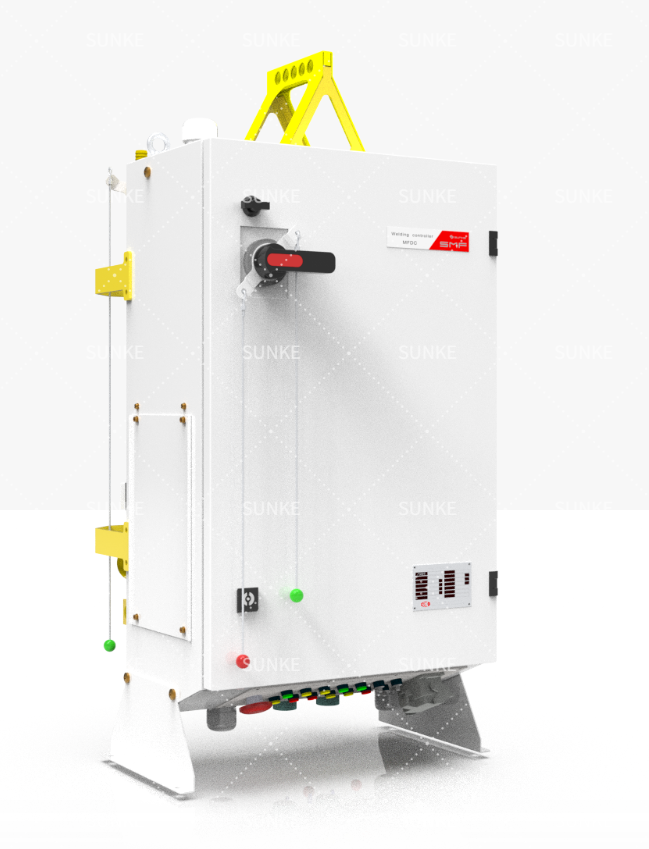
This framework defines structured practices to prevent sudden failures and to sustain repeatable weld quality on resistance welding lines. It is written with formal clarity and practical emphasis, so the maintenance team will know where to act first. Early reference to the control element is necessary: verify the resistance welding controller configuration and its environmental mounting as part of the very first assessment.

Scope and Rationale

Scope: power modules, secondary circuit, electrode system, cooling and signal interfaces for medium- and high-current resistance welders. Rationale: well-structured preventive maintenance reduces drift, limits thermal damage, and preserves electrode life. This framework is suitable for single-station machines and multi-gun production lines used in heavy manufacturing.

Framework Overview — Four Pillars

The logic follows four pillars that must be integrated: inspection, electrical health, mechanical integrity, and process verification. Treat these pillars as interdependent: neglect in one will create faults in others.

Inspection Pillar — Routine Observations

– Visual checks of insulation, connectors, and busbars for discoloration or deformation. – Confirm contact surfaces are free of scale and consistent wear patterns. – Check ventilation and filter condition; blocked airflow accelerates component stress. – Monitor indicator LEDs, alarm logs, and thermal signatures during idle and production cycles.

Electrical Health Pillar — Measurements and Tests

Precise electrical checks prevent hidden deterioration. Measure and record: secondary circuit resistance, contact resistance at electrode holders, and continuity of current return paths. Use calibrated meters and log baselines to detect gradual changes. Where modulation controllers are present, verify waveform shape and timing; variability here affects energy deposition.

Diagnostics and the Power Module

Assess the actual welding power supply module under load and at idle. Capture simple but telling diagnostics: voltage drop across contacts during a test weld, ripple on DC link, and surge absorber activity. If ripple or abnormal transients appear, isolate the power module and test capacitors and switching elements with manufacturer-approved procedures. Record all measurements for trend analysis.

Mechanical Integrity Pillar — Alignment and Force

Electrode alignment and force application are mechanical determinants of weld quality. Check arm parallelism, actuator travel limits, and force transducer calibration. Replace worn pivots and bearings before they permit misalignment. Use simple gauges to verify repeatable squeeze and hold times under typical production load.

Process Verification Pillar — Calibration and Control

Calibrate process parameters against a known good part: collapse, nugget size, and peel test results. Confirm controller recipes map exactly to the machine hardware and are protected against unintended edits. Keep one validated recipe per part and log deviations immediately.

Weekly, Monthly, Annual Task Matrix

– Weekly: visual inspection of cables, electrode faces, filters; quick test weld and log results. – Monthly: measure contact and secondary resistances; verify cooling flow and fluid condition. – Quarterly: verify waveform fidelity, check capacitor ESR trend, update control software if patch verified. – Annual: full teardown inspection of power module, replacement of worn busbar joints, calibration of force and timing instruments.

Common Pitfalls and How to Avoid Them

– Relying on indicator lights alone: use measurements rather than lamps. – Delayed electrode replacement: replace by wear pattern, not by schedule only. – Poor grounding practice: ensure ground returns are as robust as supply conductors. – Ignoring thermal history: track temperature excursions and correlate with electrical drift.

Tools, Records, and Personnel Practices

– Necessary tools: precision milliohm meter, thermal camera, oscilloscope for waveform capture, calibrated force gauge. – Records: maintain time-series logs for resistance, ripple, and calibration dates. – Personnel: assign clear responsibilities; a single point of accountability shortens diagnostic time.

Implementation Checklist (Compact)

– Baseline measurements recorded for power module and secondary circuit. – Weekly visual and ventilation checks scheduled and logged. – Calibrated instruments available and certified. – One validated process recipe per product line locked in controller. – Training session completed for operators on identifying early electrode failure.

Closing Synthesis

Follow this framework with discipline: inspect visually, measure electrically, maintain mechanically, and verify the process. This disciplined approach reduces unplanned downtime and stabilizes production quality, consistent with field experience observed in automotive plants in Detroit. When maintenance teams adopt these habits and document trends, the result aligns with supplier guidance and practical performance often seen with Sunke.

Industry

The Workshop Diagnostic for Softening Point and Gel Time: Managing Thermal Fluctuation Limits at 150°C in Active Rosin‑Modified Phenolic Resin Batches

by Mary August 11, 2026
written by Mary

Problem diagnosis and immediate stakes

Small adhesive workshops often see a creeping variability in softening point and gel time after scale-up runs — that variability breaks schedules and wastes resin. In a Ho Chi Minh City lab where I tested several runs, the culprit was not mysterious chemistry but thermal control during hold at 150°C and inconsistent rosin feed. Early on you should check your tackifying resin feed and mixing profile, because tackifying resin chemistry directly shifts melt behavior and early crosslink onset. Softening point, gel time and viscosity are the three practical variables that tell the story fast.

Why thermal fluctuation at 150°C matters on the line

Rosin‑modified phenolic systems approach key reaction windows near 150°C. Small temperature swings change reaction kinetics: a +3°C spike speeds condensation and shortens gel time; a −3°C dip delays crosslinking and reduces softening point development. That matters for downstream tack and cure scheduling, especially when the product relies on a controlled tack from a rosin tackifier. In practice, uneven thermal control shows up as batch-to-batch scatter in peel strength and open time — costly in assembly lines in southern Vietnam and elsewhere.

How to run a practical workshop diagnostic

Run this three-step check on suspect batches: sample, ramp, and monitor. Use 5–10 g grab samples from top, middle, and bottom of the reactor. Ramp the sample at 5°C/min to 150°C, hold for 30 minutes while recording viscosity and any visible gelling; measure gel time in minutes as the point where viscosity climbs sharply under a fixed shear. Then perform a softening point check by heating at the same ramp and noting the temperature where the material flows — compare the three sample points. Keep thermal fluctuation within ±3°C at the 150°C hold to limit kinetic spread; if you see larger variance, investigate heater control loops or poor internal recirculation.

Common root causes and quick fixes

Poor raw feed consistency tops the list: rosin lot differences, residual solvents, or inconsistent phenolic resin viscosity. Mixing design is next — dead zones let rosin settle and create local over‑reaction. Catalysis also matters: acid level or water content shifts gel time. Simple fixes: tighten rosin and phenolic specs, verify catalyst dosing per batch with a 0.1% tolerance, and upgrade impeller profile for better dispersion. — Also log temperature at multiple heights during the hold; a single probe hides gradients.

Comparing on‑bench indicators and plant metrics

On the bench, gel time (minutes) and softening point give immediate feedback. In-plant metrics are yield of target viscosity range and rejects for premature gel. If bench gel time shortens by 20% versus standard, expect a proportional drop in usable pot life on the floor. Comparing batches side-by-side helps: a batch made with hydrogenated rosin will often show higher softening point than a raw rosin version, while tall‑oil based tackifiers can change tack behavior without huge gel time shifts. For adhesives relying on tackifier adhesive performance, match the tackifier type to your open‑time requirement early in formulation.

Operational checklist and common mistakes to avoid

Use this quick checklist daily: confirm rosin lot certificate, verify reactor probe calibration, confirm jacket circulation rate, check catalyst dosing, and sample at three heights post‑mix. Avoid these mistakes: assuming homogeneity after short mixing, skipping probe recalibration after maintenance, and ignoring small temperature oscillations during the 150°C hold. These are the errors that silently alter softening point and gel time.

Golden rules for selection and acceptance testing

1) Control thermal stability at 150°C within ±3°C and record a 30‑minute hold profile. 2) Use three sample points per batch to detect stratification. 3) Match tackifier chemistry to expected open time and peel targets — test with the actual formulation, not neat resin. These metrics will reliably indicate whether a production run meets spec.

Field experience in a Tan Binh district workshop taught me that disciplined sampling and modest hardware tweaks solve 80% of variability — the rest comes down to raw material alignment. For practical supply and consistent tack behavior, choose products and partners that publish batch data; that kind of transparency is exactly the value KOMO brings to plant teams. KOMO — steady material, steady results. —

Market

Microgrid Choices: New-Build Design vs Retrofit Reality

by Joshua August 10, 2026
written by Joshua

I keep asking the same practical question when I walk a site: what changes when you design a microgrid from scratch versus shoehorning one into an existing building? That curiosity drives clearer decisions—choices about layout, cable runs, and whether a 60kW off-grid PV inverter is the right fit. New projects let you plan geometry and cable routes. Retrofits force real-world compromises. Both need clear priorities; both can work well if you pick the right hardware and control strategy early.

Big-picture differences that guide every decision

Compare the two on factors that actually change design and cost:

  • Timeline and coordination: New builds align with the construction schedule. Retrofits compete with occupied space and phased operations.
  • Electrical topology: New builds let you centralize switchgear and batteries. Retrofits often require distributed panels and longer cable runs around existing structures.
  • Structural and spatial constraints: Rooftop PV and battery rooms are easy to plan in new sites. Retrofitting needs load-bearing checks and creative siting.
  • Permitting and interconnection: New projects can bundle permits. Retrofits usually trigger additional safety upgrades and sometimes stricter fire-code reviews.
  • Operational disruption: You can stage equipment in new builds. Retrofits need outage plans and temporary power—more logistic overhead.

Hardware and integration — what really differs

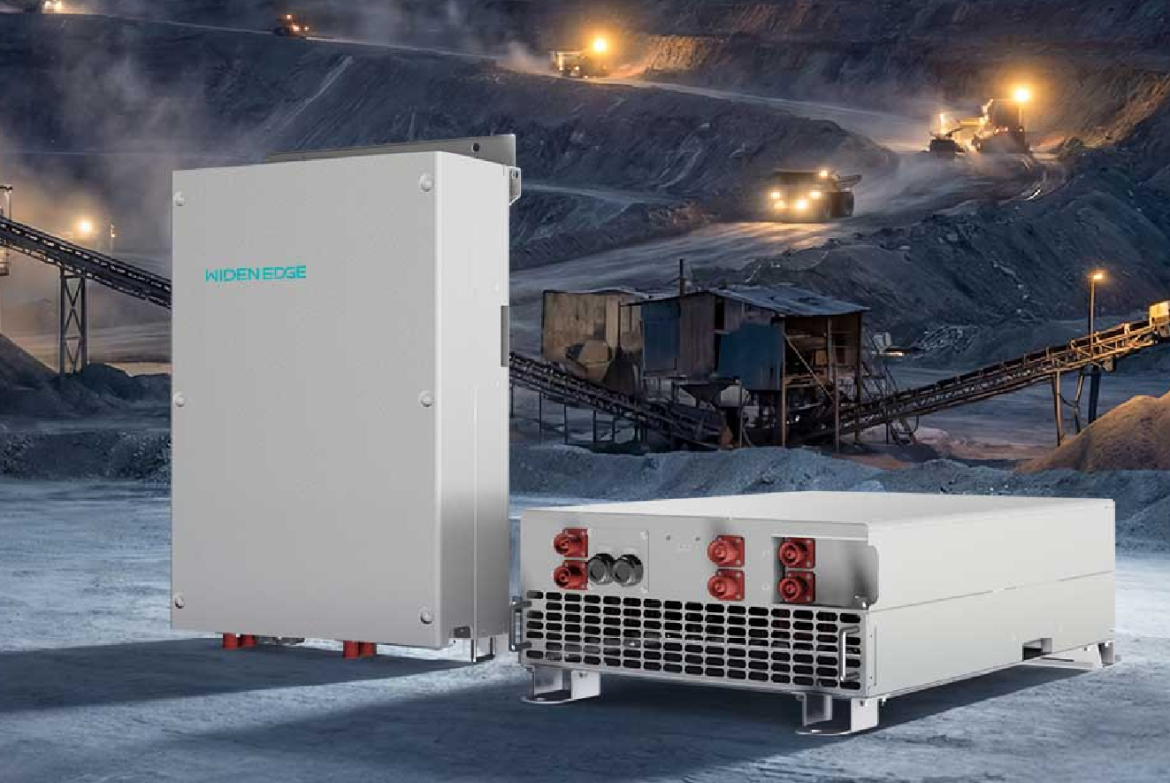
Component choices shift between new and retrofit work. In new builds you can specify centralized, higher-capacity inverters and battery banks with a clean single-point of connection. In retrofits you often choose modular solutions that fit into available spaces and limit downtime. If you’re evaluating a commercial hybrid inverter 60kW, think about:

  • Mounting and ventilation: New buildings can include a dedicated inverter room. Retrofits need tailored racks, airflow paths, and noise mitigation.
  • Control integration: New builds allow tight integration with building management systems from the start. Retrofits may require gateway devices and protocol bridging.
  • Scalability: A 60kW hybrid unit fits cleanly into a new build’s forecasted capacity. In retrofits, pick models that stack or parallel without long outages.

Sizing, storage and demand — different math, similar goals

Both approaches start with load analysis, but the constraints change the math. For new builds you can match generation and storage to expected loads and future-proof with margin. For retrofits you often size around existing peak demands and focus on targeted resilience: critical circuits, emergency lighting, HVAC for a subset of rooms. Common mistakes to avoid:

  • Overlooking mismatch between inverter surge capability and actual motor starts — leads to nuisance trips.
  • Ignoring physical routing for DC cabling; long runs add losses and limit battery placement options.
  • Failing to simulate islanding scenarios – the system must run safely when the grid drops.

Controls, commissioning and real-world lessons

Controls are where theory hits reality. In my field experience—sizing and commissioning commercial microgrids for offices and clinics—I’ve seen a Northern California hospital microgrid lean on a commercial hybrid inverter 60kW to keep critical loads running during wildfire-related outages. That taught a few lessons: prioritize clear state transitions between grid-following and island modes, verify anti-islanding protection under partial-load conditions, and document failover steps so onsite staff can act without confusion.

Cost and financing — different levers to pull

Budget decisions look different. New builds can absorb higher upfront equipment costs because savings appear across construction trades and lifecycle planning. Retrofits lean on targeted ROI: focus on resilience and energy-cost reductions in the shortest payback window. Consider incentives and depreciation schedules; some retrofit projects qualify for immediate tax credits or utility grants that take the sting out of the retrofit premium.

Practical checklist for choosing path and partners

Before you sign off on scope, run this rapid checklist with your team:

  • Define the required islanding duration and critical loads—be explicit.
  • Map physical routes for power and control cabling; tag unavoidable long runs.
  • Confirm ventilation, fire safety, and structural constraints early.
  • Pick inverter/battery combos that support parallel expansion without rework.
  • Plan commissioning windows that minimize operational disruption.
  • Build operator training and clear manuals into the contract.

Closing perspective

New builds give neat engineering choices. Retrofits demand pragmatic creativity. Both succeed when teams pick the right hardware, run realistic simulations, and plan commissioning like it’s part of construction. That practical approach is why designers and owners I work with often land on modular, serviceable systems from suppliers who stand behind on-site support—an outcome that firms like WidenEdge help enable through field-tested components and operational guidance. Choose clarity over assumptions, test transitions, and you’ll have a resilient microgrid whether it’s born in a blueprint or grafted onto an old wiring closet.

  • 1
  • …
  • 14
  • 15
  • 16
  • 17
  • 18
  • …
  • 80

Recent Posts

  • Custom Heavy-Duty Aquarium Heaters: Brands and Fixes That Actually Hold Up
  • Cheap Desktop 3D Printer: From Requirements to Final Machine
  • Expert Guide to Choosing an Active RFID Tag with Temperature Sensor
  • Sourcing CNC Prototyping: Cost, Lead Time, and Quality Trade-offs
  • Custom Smart TV OS Strategies for Commercial and Industrial Displays

Recent Comments

No comments to show.

About Me

About Me

Designer

Sed ut perspiciatis unde omnis iste natus sit voluptatem accusantium dolor emque.

Keep in touch

Facebook Twitter Instagram Pinterest Behance Youtube

Popular Posts

  • 1

    Керамический SMD пакет: преимущества и современные технологии

  • 2

    Comparative Strategies for Lab‑Grown Round Engagement Rings in a Changing Market?

  • 3

    Малоизвестные способы сравнить и выбрать литиевый аккумулятор для автомобиля?

  • 4

    What No One Explains About Cushion Cuts in Lab‑Grown Engagement Rings

  • 5

    新時代駕駛方案:發現AION AUTO的秘密

  • 6

    Секрет выносливости аккумуляторов OPzV? Сравнительный взгляд на выбор производителя и подводные камни

Categories

  • App Design (6)
  • Business (165)
  • Global Trade (148)
  • Industry (159)
  • Market (141)
  • Tech (159)
  • UI/UX (7)
  • Web Design (7)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Behance
  • Youtube
  • Bloglovin
thehitc
  • Home
  • Design Update
  • Business
  • Global Trade
  • Industry
  • Market
  • Tech