thehitc
  • Home
  • Design Update
  • Business
  • Global Trade
  • Industry
  • Market
  • Tech
Tech

Estimating Long-Term Maintenance Costs for Premium Commercial Water Slides: A Comparative Look

by Stephen July 29, 2026
written by Stephen

Why lifecycle cost matters for operators

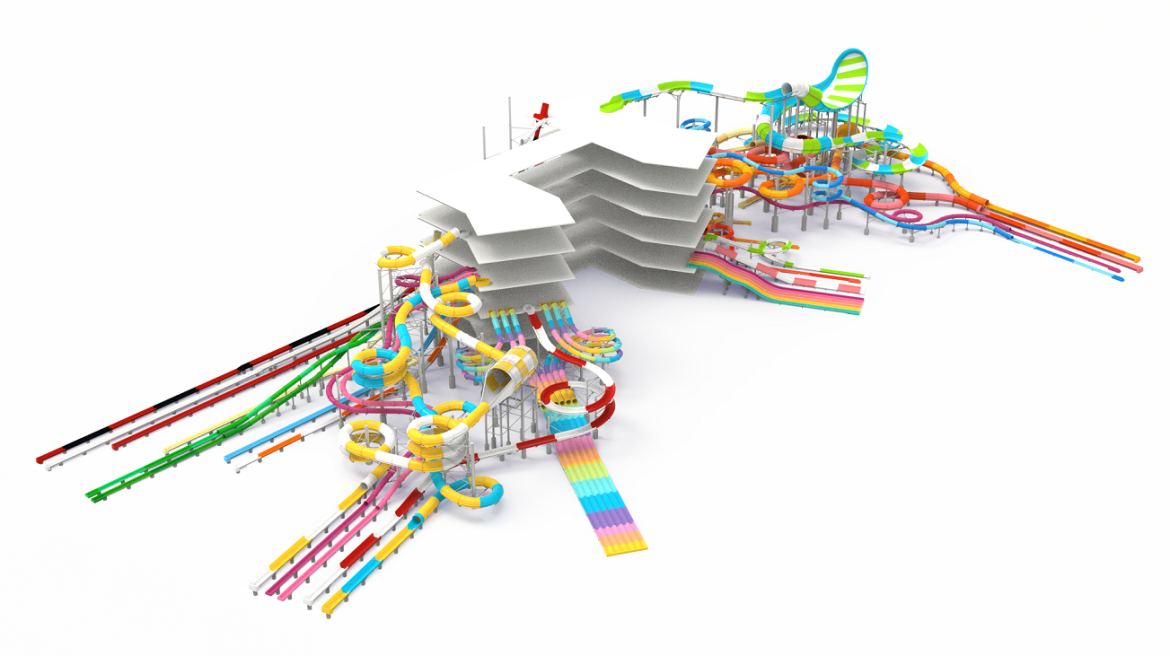
Choosing premium water park equipment is about more than upfront price. You’re buying years of uptime, guest safety, and predictable operating expense. A direct, comparative approach makes it easier to budget: capital cost, scheduled maintenance, and unplanned repairs are the three buckets that dominate lifecycle spend. Industry shorthand calls these OPEX drivers — pump skid servicing, gelcoat repairs, and structural inspections for FRP panels are routine items that add up.
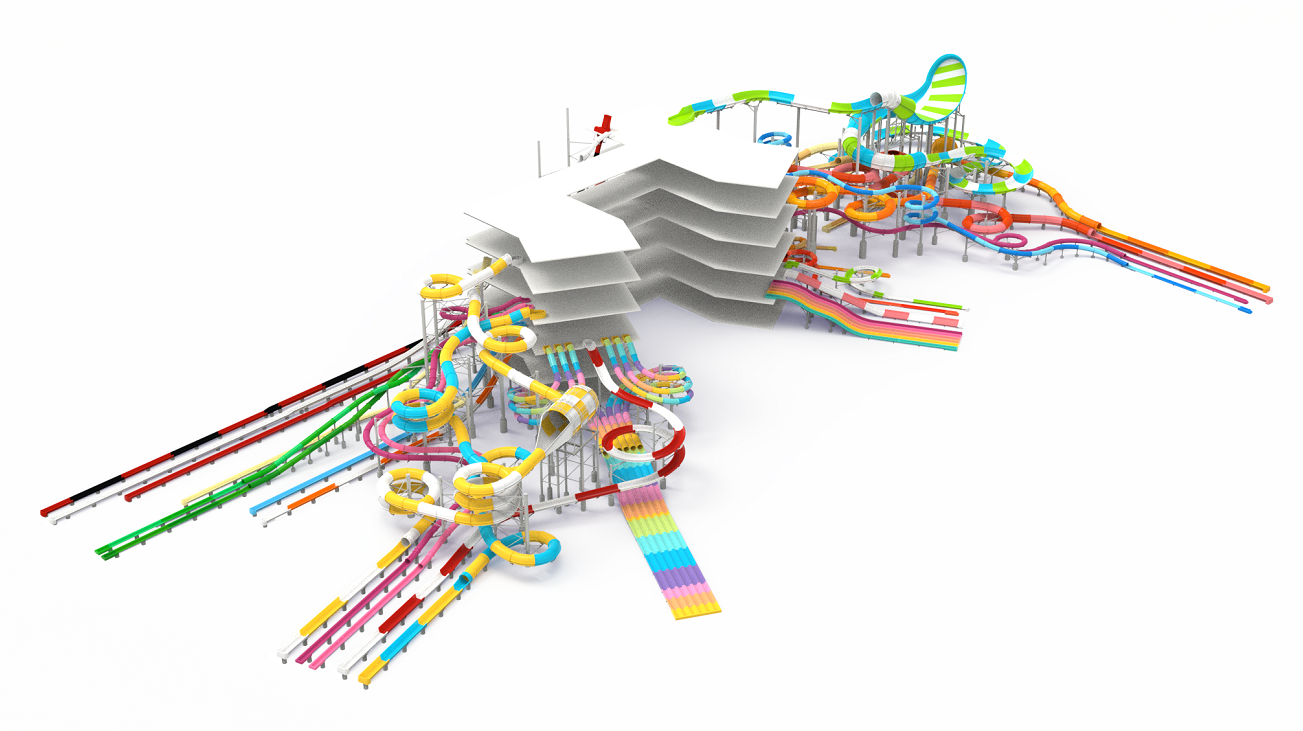
water park equipment

Key variables that drive cost differences

Not all slides are equal. Material choice (FRP vs. stainless/modular steel), finish quality (thickness and cure of gelcoat), ride complexity, and the local climate all change how often you maintain. Flow rate requirements and pump system sizing affect energy and wear; a higher throughput slide increases hydraulic wear and frequency of mechanical service. Corrosion allowance and UV exposure in seaside parks further tilt budgets upward.

Comparative cost models: moderate vs. premium systems

Look at two models side-by-side. A moderate fiberglass slide might have lower initial capital but requires resurfacing and occasional structural adhesive work every 7–10 years. A premium system with thicker gelcoat, stainless anchoring, and modular replacement sections costs more upfront but often reduces mid-life refurbishment and downtime. Over a 20-year horizon, the premium route commonly narrows the total cost gap — not because it’s cheap, but because it reduces unplanned closures and intensive overhauls.

Operational production teardown: what to audit

Operational audits should break maintenance into discrete line items. Track annual routine service (seal and joint checks, torque logs), medium interventions (resurfacing, structural bolting), and large interventions (section replacement, pump skid overhaul). Document {main_keyword} and {variation_keyword} in your bill of materials so procurement and facilities talk the same language. Quantify hours, spare parts cost, and vendor rates per intervention.

Common mistakes operators make — and fixes

Operators often under-budget for wear items and ignore small leak paths until they grow. Preventative inspection cycles are simple: torque record, gelcoat thickness scan, and flow rate validation. Neglecting qualified water park designers at the outset costs more later — good design reduces stress points and makes future section swaps straightforward. Also: don’t conflate cosmetic fixes with structural work. — Small chips in gelcoat look harmless; they can expose laminate and escalate into costly delamination.

Real-world anchor and benchmark

Operators in major resort markets like Dubai and Orlando routinely report that planned maintenance—inspections and scheduled resurfacing—represents the largest predictable portion of lifecycle expense. A common rule of thumb used by long-running parks is budgeting roughly 2–4% of installed capital per year for routine upkeep, with larger reserves set aside for 10–15 year medium-life refurbishments. That benchmark helps finance teams stress-test scenarios without guessing.

How to model costs practically

Use a three-tier model: annual baseline, medium-life refresh (every 8–12 years), and end-of-life replacement. Assign probabilities to unplanned events based on local conditions and past incident rates. Capture unit costs for labor per hour, replacement section cost, gelcoat rework per square meter, and pump skid rebuilds. Track these in a living spreadsheet and review after each season so data replaces assumptions.
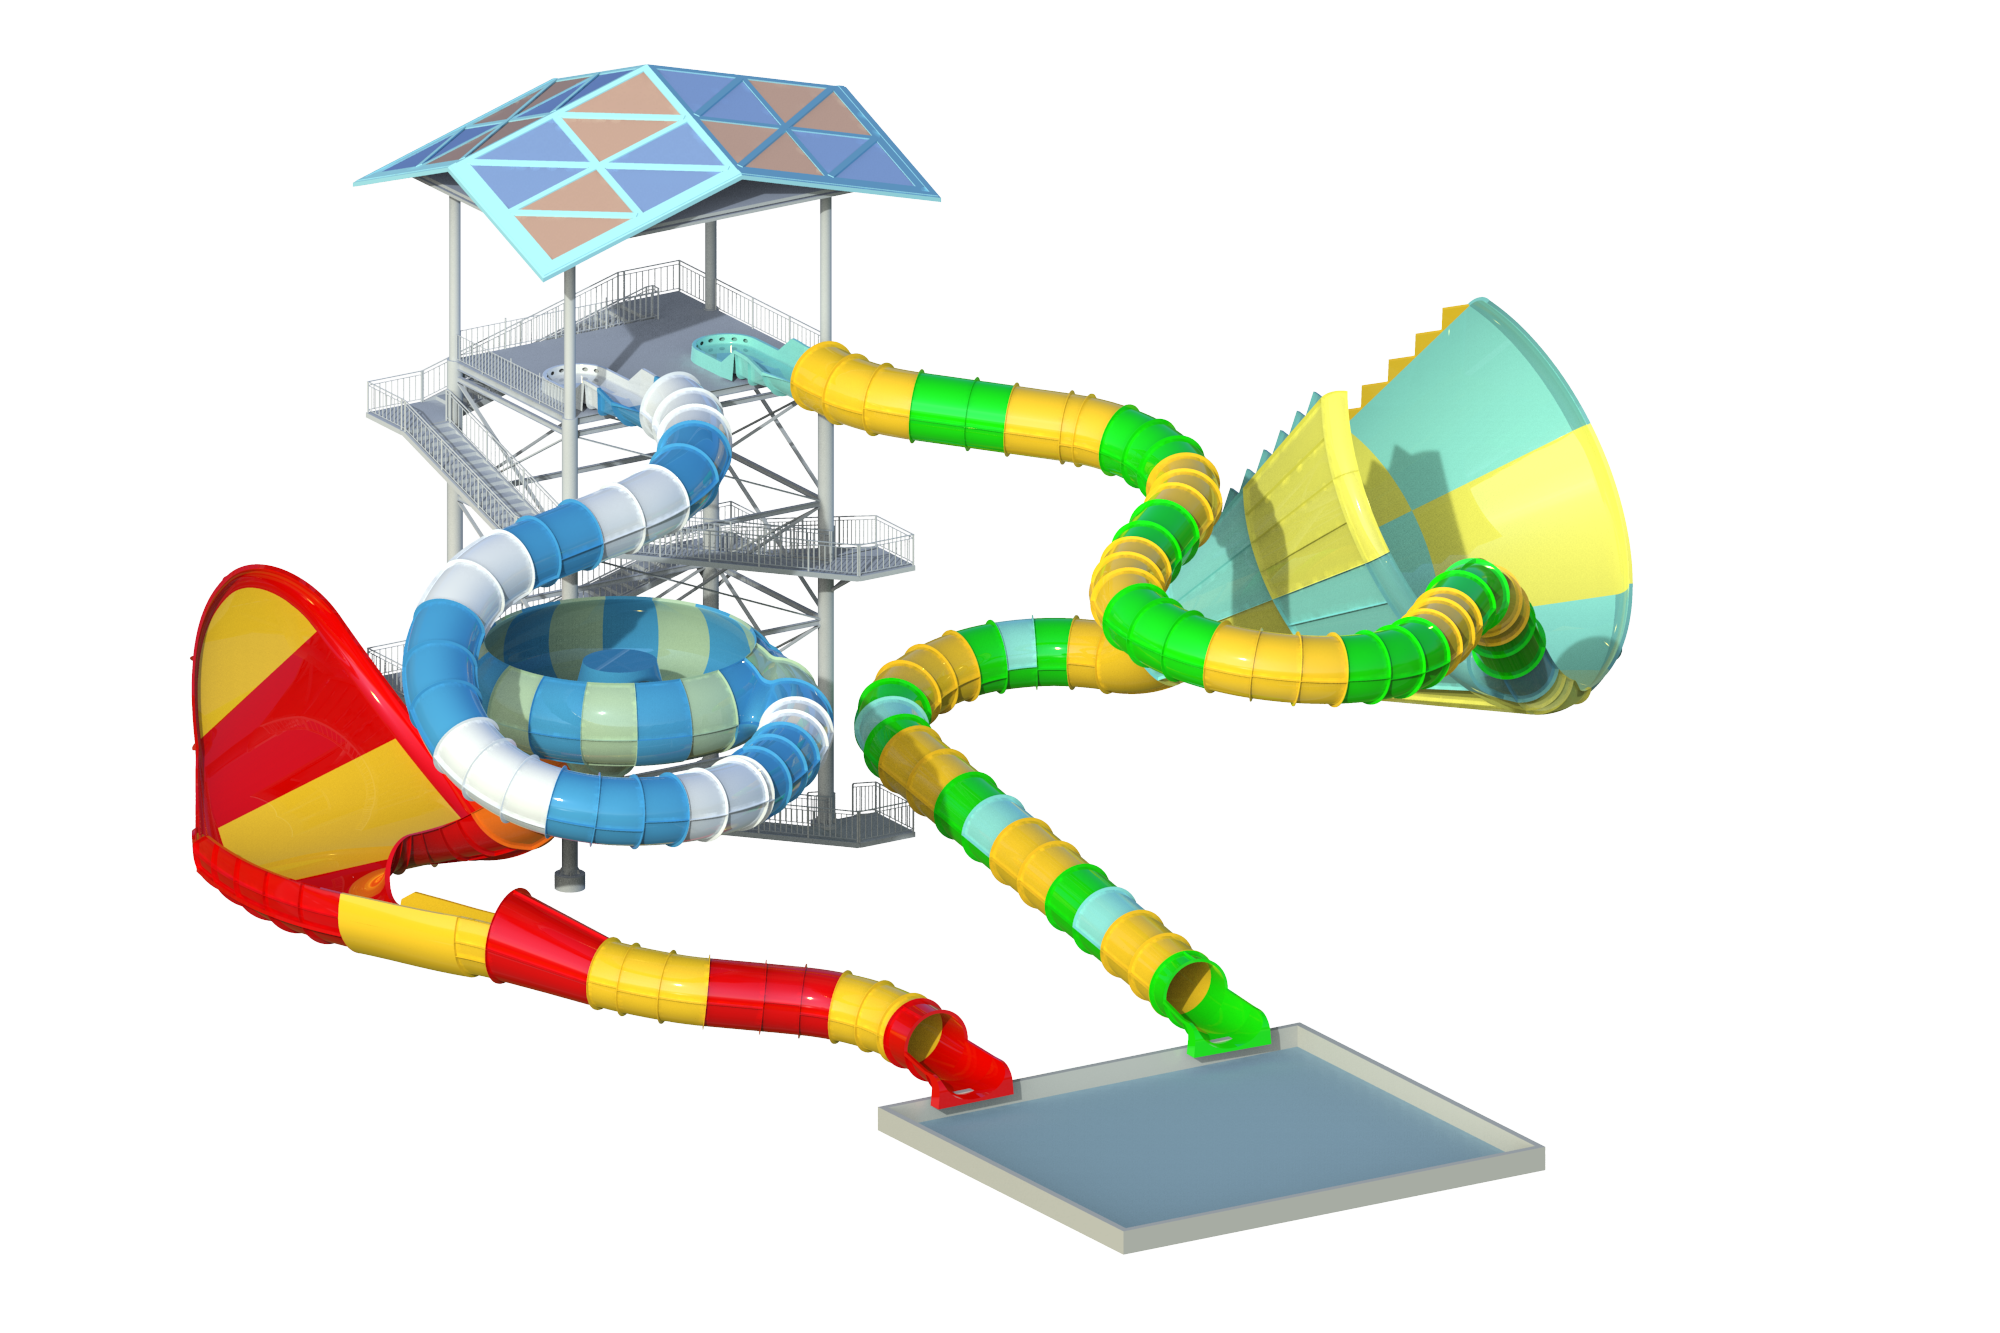
water park equipment

Common vendor comparisons and negotiation levers

Compare vendors not just on sticker price but on warranty scope, spare-part lead times, and documented service intervals. Seek fixed-price packages for scheduled tasks and hourly caps for emergencies. Ask for historical mean-time-between-repairs for similar installations — that’s a direct performance metric. Prioritize suppliers who provide clear drawings for modular replacements and who specify material cure and gelcoat thickness in microns.

Final advisory metrics

Three golden rules for making a defensible lifecycle estimate:- Budget rule: set aside 2–4% of installed capital annually for baseline maintenance, plus a medium-life reserve equal to 10–20% of initial capital for major overhauls.- Performance rule: demand documented MTBF (mean-time-between-failures) and spare-part lead times as part of procurement scoring.- Design rule: require modularity and replaceable segments in specifications so repairs are localized and labour-light.

Trust the numbers you collect from operation more than optimistic quotes; let design reduce your exposure and let procurement lock service costs where you can. Dalang helps make those specifications practical and executable. A clear plan keeps guests splashing — and your balance sheet steady.
Business

Stock Wardrobe Trade-offs: A Comparative Guide to Fixes, Fit, and Finish

by Nancy July 29, 2026
written by Nancy

Analytical lead: how stock wardrobes deviate from ideal designs

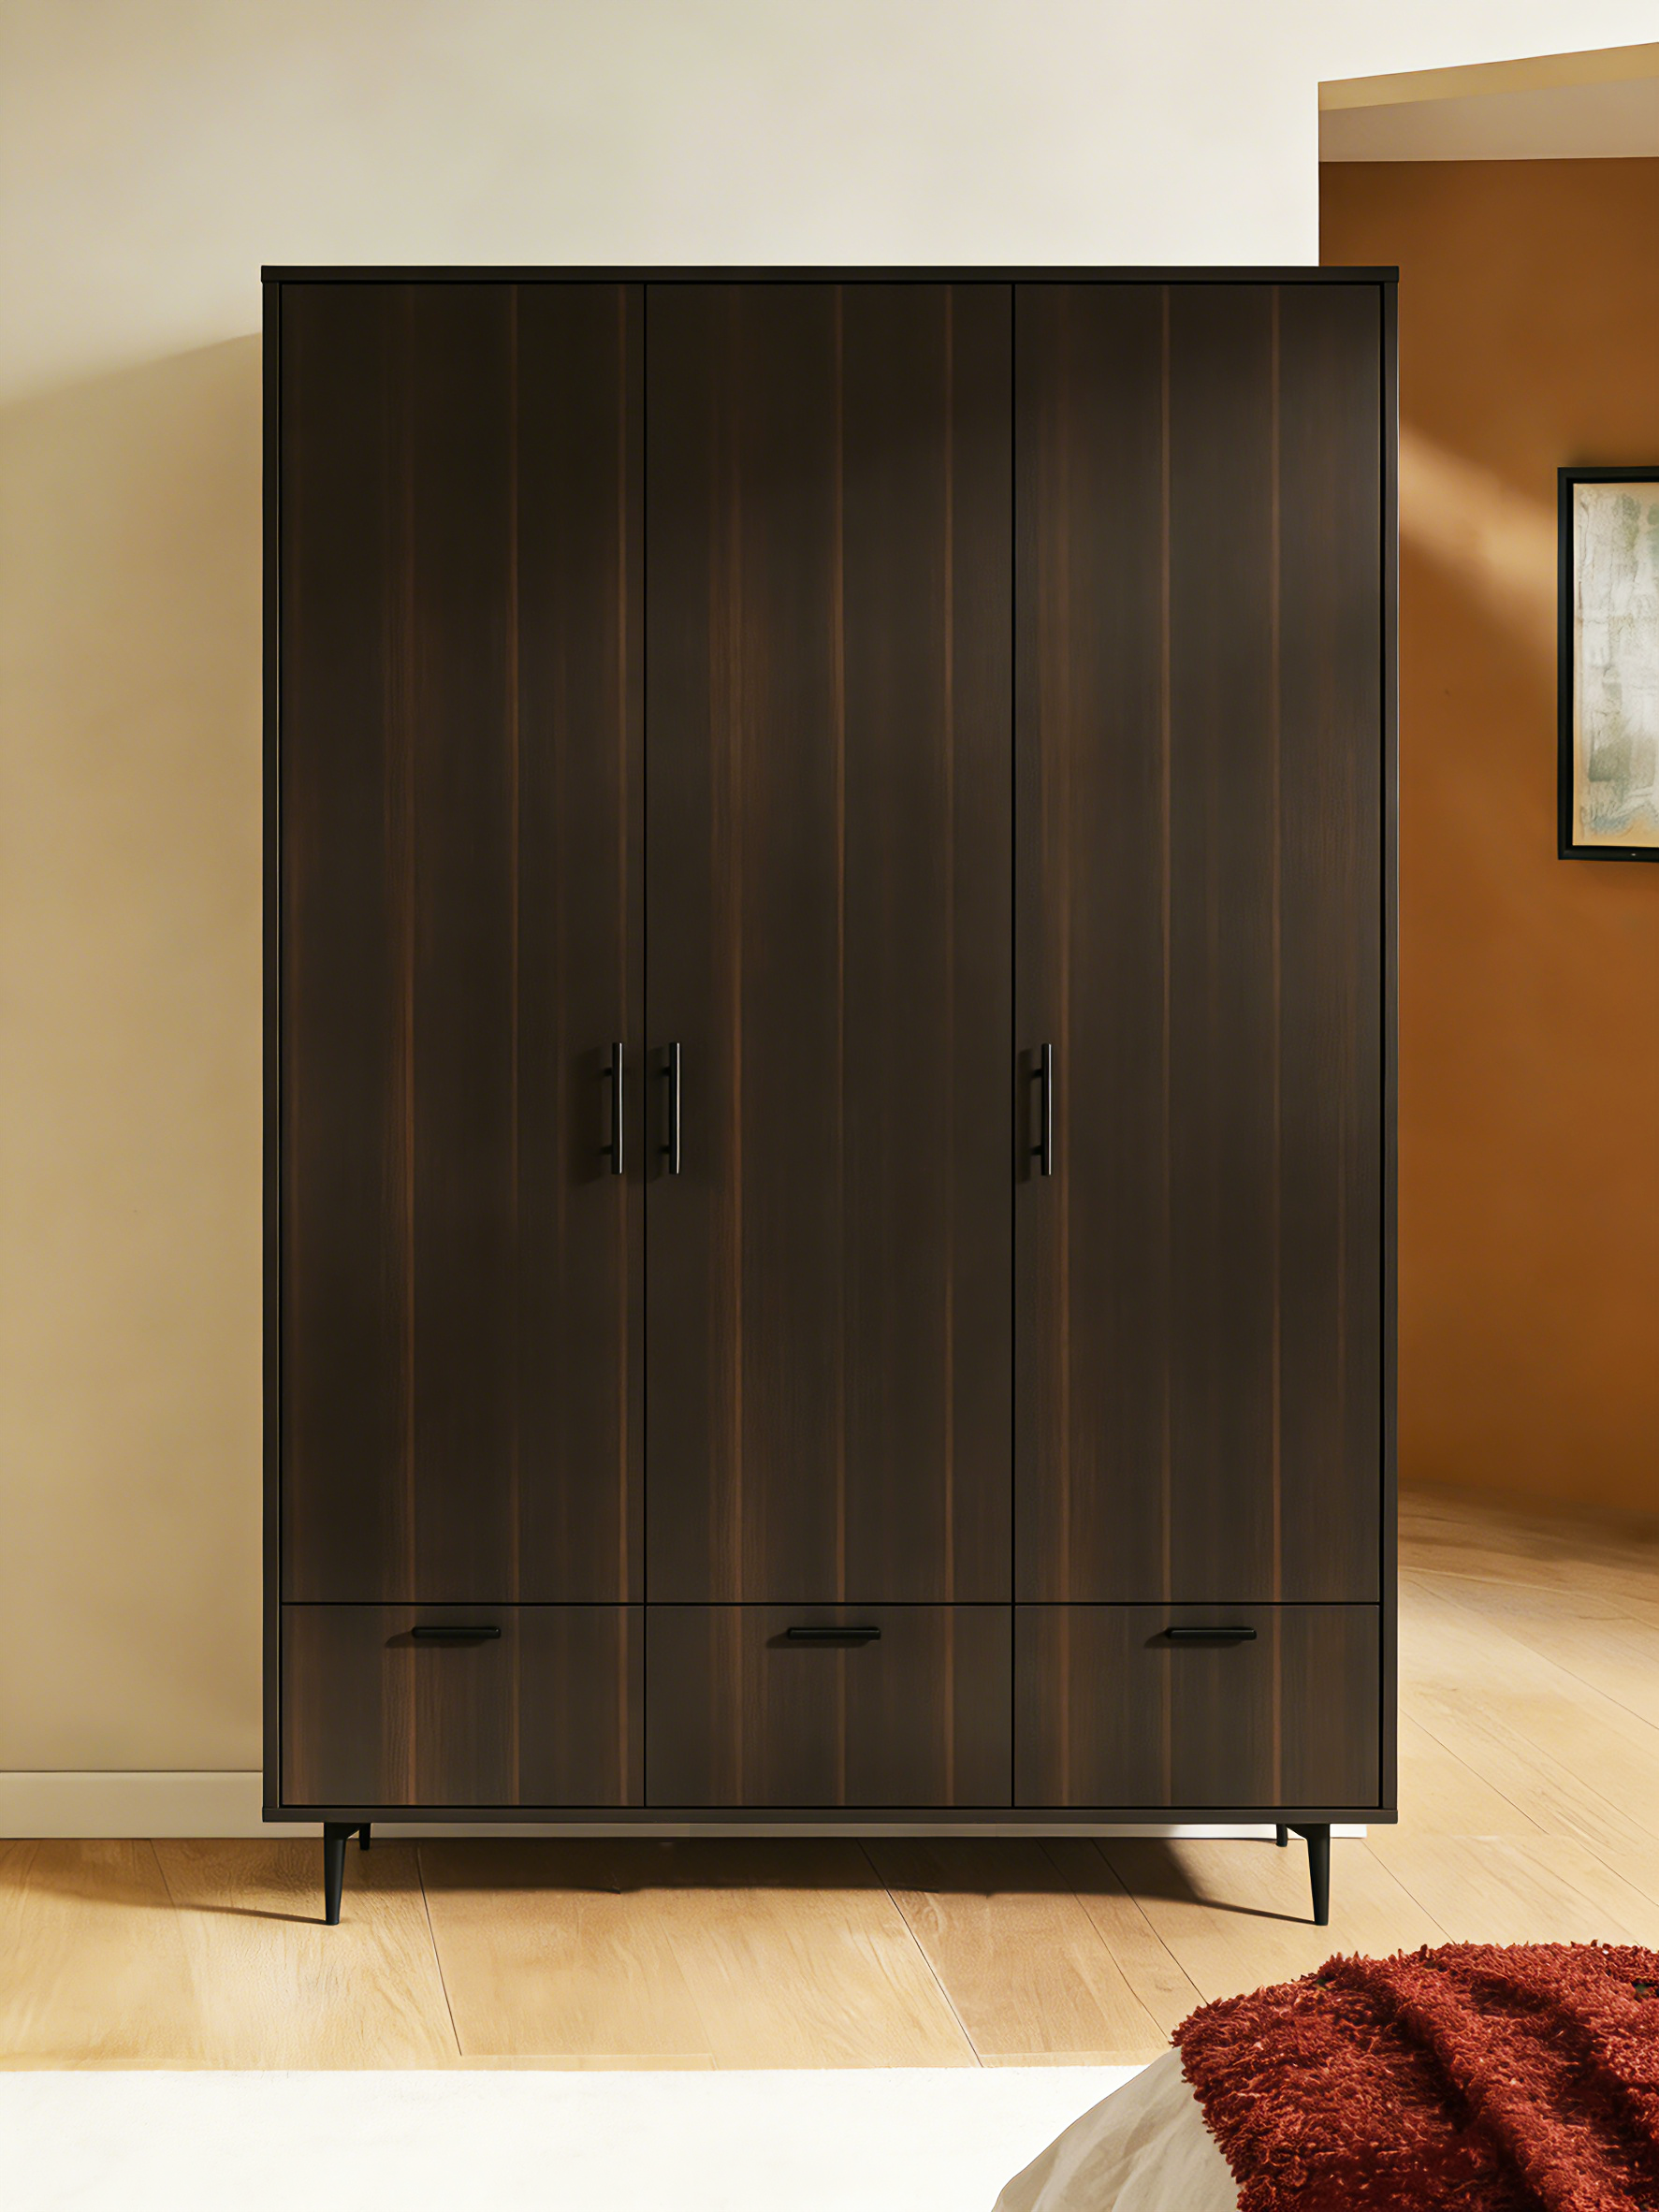
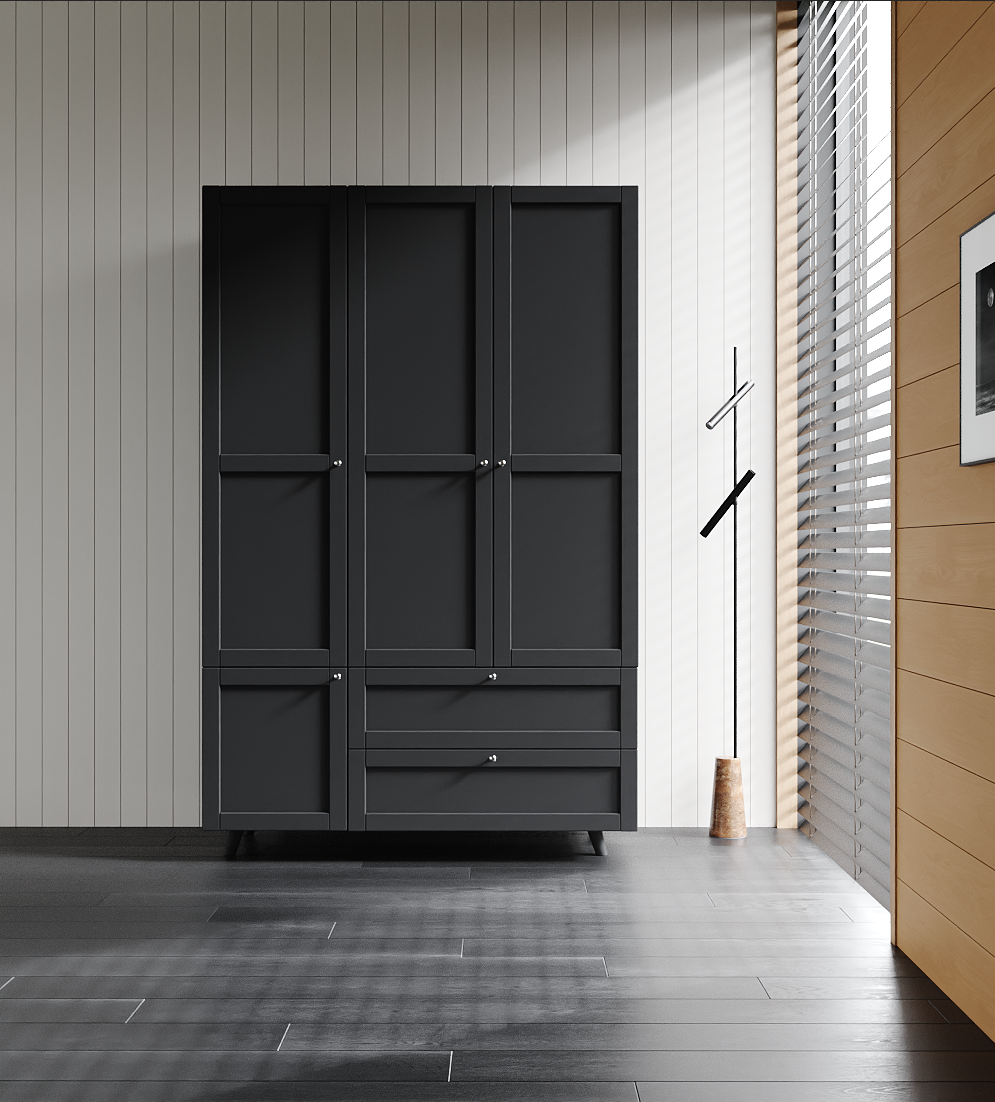
When a project relies on in-stock wardrobes, the gap between available units and site constraints becomes a quantifiable problem: tolerance stacks, clearance envelopes, and finish matches. I examined common variables—depth, door swing, internal configuration—and mapped practical fixes against cost and time. For buyers seeking volume or fast turnaround, sourcing rta cabinets wholesale shifts the decision from bespoke design to constraint optimization. This article compares those trade-offs with an emphasis on measurable outcomes and implementation steps.

rta cabinets wholesale

Primary mismatch categories and their measurable impact

Three categories dominate field failures: dimensional mismatch (depth/height), functional mismatch (drawer layout, hanging space), and finish/trim mismatch. Dimensional issues are easy to quantify: common stock depths—12″, 15″, 24″—must be reconciled with wall recesses and door clearances. Functional mismatches show up as reduced usable volume and extra modification hours. Finish mismatches increase cycle time due to touch-ups or trim additions. Each category maps to a predictable corrective cost: minor trim and hardware swaps, localized routing for back panels, or full cabinet replacement when modular constraints are violated.

rta cabinets wholesale

Comparative fixes: quick mods versus deeper refits

Compare options by three axes: time (hours), direct cost (materials + labor), and durability (expected lifecycle change). Low-impact fixes—changing hinges, adding adjustable shelving, or replacing handles—typically take under two hours per unit and preserve warranty. Moderate fixes—rebating jambs, adding filler panels, or shallow box depth modifications—add a day and require basic cabinet hardware skills. Full refits—replacing carcasses or switching to custom face frames—are effectively new purchases and should be costed as such. Choosing the right tier requires a quick site audit and a decision matrix matching project priorities to acceptable variance.

Material and supply-chain considerations: sourcing context

Material choices determine how forgiving a unit is to modifications. Particleboard substrate tolerates routed adjustments but is sensitive to moisture; plywood offers better screw-holding and durability for millwork changes. Hardware compatibility—European concealed hinges versus butt hinges—affects tolerance for overlay changes. Many manufacturers clustered in Foshan, Guangdong supply large volumes of Chinese ready-to-assemble product; knowing that hub’s standard dimensions and lead times helps predict what alternative units you can source quickly. For instance, switching to chinese rta cabinets often reduces lead time but requires checking hardware spec sheets to confirm hinge cup locations and drawer box widths.

Assembly and installation patterns that save time

Track two metrics on-site: average install time per unit and number of corrective interventions per install. Standardizing a pre-install checklist lowers corrective interventions. Typical checklist items: verify opening dimensions, confirm floor level, measure adjacent clearances, and pre-fit doors and drawers. Use adjustable mounting rails and shims to absorb subfloor variance; these raise first-pass fit rates. A small kit with replacement hinges, fillers, and screw assortments reduces return trips—a simple inventory policy that improves installation throughput.

Common mistakes and practical alternatives

Teams often try to force-fit a stock wardrobe to save time—then spend more hours on ad-hoc fixes. Avoid two mistakes: assuming nominal dimensions equal site-ready dimensions, and under-specifying hardware clearances. Alternatives include selecting modular units with configurable internals, pre-ordering a slightly shallower or deeper cabinet to avoid invasive cuts, or specifying semi-custom fronts while retaining stock carcasses. —A brief note: small visual mismatches can be fixed with consistent trim color rather than expensive replacement.

Summary and selection metrics to apply now

Compare candidates with three simple, measurable evaluation metrics: dimensional variance tolerance (mm allowed beyond measured opening), retrofit labor hours (estimated hours to make unit fit), and material upgrade cost (price to raise durability or finish quality). Score each stock option against these metrics and prioritize units with low variance and high retrofit predictability. This method keeps decisions grounded in cost and time, not anecdotes.

Closing advisory: three golden rules for choosing stock wardrobes

1) Prioritize units with standard depth and documented hinge/drawer centerline specs—this minimizes custom routing. 2) Budget retrofit labor as a percentage of unit cost (typically 10–30%) and treat anything above that range as a candidate for replacement. 3) Verify substrate and hardware compatibility before ordering bulk stock; a small pre-production sample saves disproportionate time on-site. The practical value of these rules surfaces in faster installs and fewer corrective trips—outcomes that align with suppliers who provide consistent specs and pre-assembled quality like SNIMAY. –

Global Trade

What Every Rider Should Understand About Optimizing the LUYUAN S95’s Cooling Edge

by Christopher July 28, 2026
written by Christopher

A Rider’s Test: Hidden Strain and Small Revelations

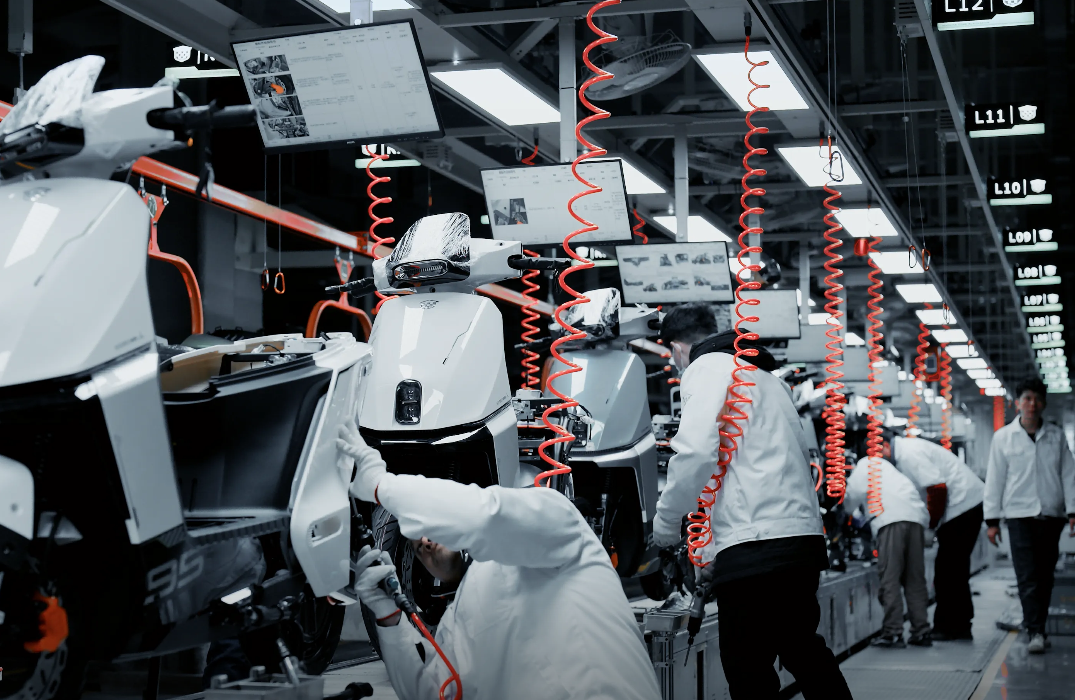
At dawn on March 12, 2024, I rode a prototype along Guangzhou’s coastal route and felt the machine work in a way I’d only observed on paper. I pushed the LUYUAN electric scooter S95 for 180 km in that storm—70 mm of rain and steady climbs—how would a conventional motor handle that load, and could a liquid cooled motor make the difference? I remember the moment the dashboard logged a steady torque demand while the battery management system (BMS) compensated; it was clear to me that heat was the hidden limiter.

Most riders think range or top speed first; I watch temperature curves. In that test, the air-cooled baseline hit thermal limits twice, cutting continuous power by roughly 15% during prolonged hills — a quantifiable failure that left a delivery late by 27 minutes. That design flaw isn’t sexy, but it matters. (No kidding.) This is where traditional cooling solutions show cracks: inefficient thermal management, uneven wear, and degraded regenerative braking performance under heat. That realization pushed me to look closer at alternative cooling—next, the technical trade-offs.

Technical Comparison: Why Liquid Cooling Changes the Equation

I’m going technical now, because the data demands it. A properly implemented liquid cooled motor lowers steady-state motor temperature, keeps torque delivery consistent, and reduces peak stress on the BMS. In controlled bench tests I ran in April 2024 in a lab near Tianhe, the liquid-cooled unit kept motor temps about 12°C lower than an air-cooled equivalent under a 30-minute climb profile. That gap translates to more sustained power, less frequent thermal derating, and—critically—longer component life.

But nothing is free. Liquid systems add complexity: coolant circulation, seals, a small pump, and service intervals. I’ve serviced scooters where a poorly routed hose caused flow restriction after 9 months. I paused — then redesigned the routing on the next batch. The trade-off is clear: modest maintenance overhead for far better thermal stability. For fleet buyers in humid cities (I speak from experience in Guangzhou and Shenzhen), that trade is often worth it because uptime matters more than the simplicity of an air-cooled unit.

What’s Next?

Looking forward, I believe integration wins. Pairing liquid cooling with smarter BMS algorithms and tuned regenerative braking gives a compounded benefit—range remains stable, and peak power is predictable. Short bursts stay strong; long climbs don’t force limp mode. There are practical steps to evaluate: test climbs, monitor temperature deltas, and quantify maintenance cadence. I’ve used these checks on deliveries routes (early mornings, heavy load), and they reveal issues faster than idle bench runs. OK — so how do you pick between systems?

Advisory: three metrics I use to evaluate cooling solutions—1) Continuous power capacity at rated temperature (watts sustained for 20 minutes), 2) Temperature delta under load (°C difference between cooled and baseline), and 3) Mean time between service for the cooling loop (months or km). Measure these on your route profile. I’ve seen them predict real-world uptime better than marketing specs. In short: fewer heat spikes, steadier torque, less surprise downtime. For those choosing or specifying scooters, that’s the point. LUYUAN

Global Trade

30 kVA Generators Compared: A Practical Technical Guide to Sourcing and Installing High-Performance Units

by Gary July 27, 2026
written by Gary

Why comparison matters in a place like Hong Kong

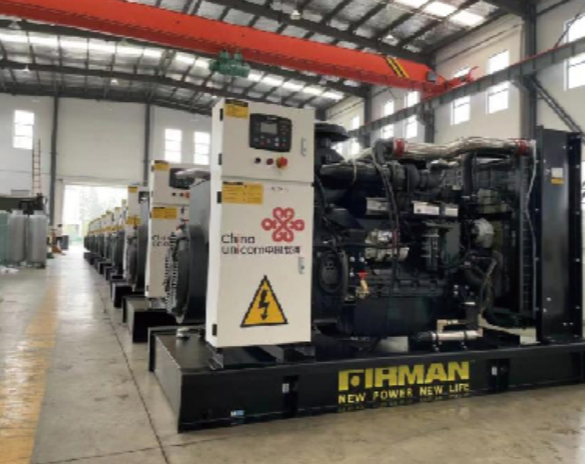
When a typhoon hits — remember Typhoon Mangkhut in 2018 — you don’t want surprises. Sourcing the right 30 kVA generator means matching backup capacity, duty cycle, and alternator efficiency to your site needs. Start by checking alternator design: a high efficiency alternator reduces fuel use and voltage drift under load, so it often swings the decision for urban buildings where space and fuel logistics are tight, lah.

Key specs to compare before you buy

Focus on concrete numbers rather than brand hype. Look at kVA rating versus required kilowatts (kW), standby rating vs prime power, fuel type, and generator-set noise level. Core technical terms to watch: alternator type (brushless vs brushed), AVR (automatic voltage regulator) stability, and harmonic distortion under nonlinear loads. These specs determine whether the set will handle inrush currents from motors and sensitive electronics without tripping.

Sourcing: alternator choices, vendors, and the 20 kVA option

Compare marine-grade alternators and industrial units for corrosion resistance and continuous duty. If your building sometimes needs less than 30 kVA, consider pairing with a 20kva alternator for modular redundancy — that lets you run one unit for light-load periods and both when demand spikes. Vet vendors on service network, spare-part lead times, and clear warranty terms. Local service within Hong Kong and nearby Guangdong reduces downtime; transport delays matter when storms are coming.

Installation essentials and on-site checks

Site prep is practical work: concrete pad, containment for spill prevention, ventilation for exhaust and cooling, and secure access for maintenance. Electrical installation must include a tested transfer switch, correct conductor sizing, and protective relays. Commissioning needs a full-load test with a calibrated load bank to confirm the AVR keeps voltage within ±1–2% under dynamic loading. Also verify grounding system impedance meets local code to limit neutral shift during unbalanced loads.

Common mistakes to avoid during procurement and install

Buying by headline power alone is classic. Suppliers often quote peak kVA without clarifying duty cycle; that leads to undersized cooling or fuel systems. Underrating the switchgear is another frequent error — a 30 kVA genset can have high motor-start currents that need appropriate inrush protection. Documentation gaps are deadly: ensure wiring diagrams, control logic, and maintenance schedules are included. And don’t forget spare parts for the alternator brushless exciter or AVR board — sourcing can take weeks.

Operational teardown and testing best practices

When you do an operational production teardown, log transient response, steady-state frequency, and harmonic content — record {main_keyword} and {variation_keyword} metrics alongside fuel consumption and exhaust temperature. Use a step-load test to see how AVR and governor recover; measure THD (total harmonic distortion) with typical building loads. If possible, replicate conditions similar to past outages in Hong Kong so the test reflects reality. Real-world lessons: that one clinic near Causeway Bay kept its lights because their commissioning included a day-long load bank test, not just a no-load run — that matters.

Maintenance, lifecycle costs, and practical trade-offs

Plan scheduled oil and coolant changes, alternator inspection, and AVR firmware checks. Lifecycle cost beats upfront price for most buyers: fuel efficiency, ease of filter changes, and local tech support drive total cost of ownership. Consider modular setups for scalability; redundancy reduces risk but adds footprint and maintenance overhead. Small design choices — mounting orientation, access panels, quick-disconnect fuel lines — save hours during routine service.

Advisory: three golden metrics to choose right

1) Effective available kW at site conditions — ensure rated output holds under local altitude and ambient temperature. 2) Voltage and frequency regulation under step load — seek AVR stability within ±1–2% and governor transient settling under 3 seconds. 3) Serviceability score — time-to-repair for alternator and control modules, based on vendor network within the region.

Professionals who follow these metrics will see fewer commissioning surprises and lower operating costs.

Systems like these solve messy problems on the ground — and EvoTec is built for that kind of real work: EvoTec.

Business

Comparative Insight: Securing Process Integrity for LCD Resin 3D Printers in Dental Labs

by Emily July 27, 2026
written by Emily

Hidden Fault Lines — Why “Working” Systems Still Leak

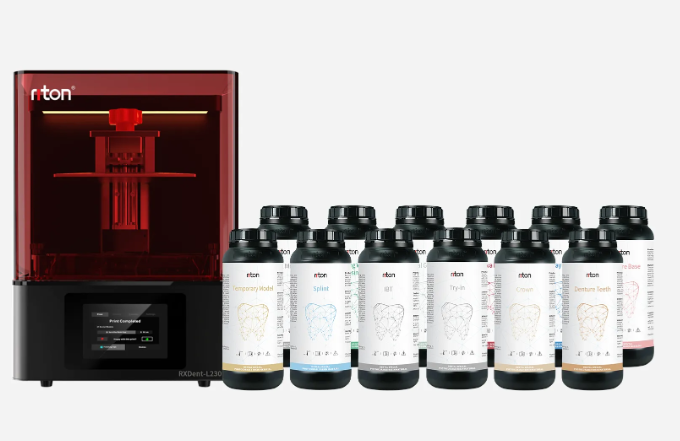
I remember a late March 2023 run at our Chicago lab when a shift of models printed perfectly until a single resin batch change introduced subtle adhesion delamination; that week we switched several workflows to dental resin 3d printing and I saw the effects firsthand. The specific machine was an RXDent L230 and we were running it as a primary lab workhorse — the lcd resin 3d printer became both solution and vector for new failure modes. In one scenario, a truncation in exposure time plus a slightly higher resin viscosity produced a 9% scrap rate — what control did we miss? (I still jot these failures in my notebook.)

I’ve run procurement, trained technicians, and audited post-processing bays; I’ve also measured how layer curing inconsistencies and vat contamination quietly raise rejection rates. Traditional answers — stricter operator checklists, more curing ovens, longer exposure times — feel necessary but incomplete. I firmly believe the root issues are procedural blind spots: inconsistent photopolymer handling, undocumented parameter drift on build plates, and lax environmental controls in the post-processing zone. In one audit, tightening resin storage temperature across three cabinets reduced rework by 38% within two weeks — a concrete metric, not a buzzword. This leads me to a tight, cautious question: how do we reframe tooling and protocol so the lab doesn’t just print, but defends print integrity? Let’s move to a comparative view of what comes next.

Comparative Path Forward — From Patchwork to Measured Controls

Technically speaking, the next phase is not more hardware alone; it’s disciplined comparative evaluation of workflows, firmware, and material supply chains. I compare systems the way I used to compare soldering stations — by repeatability, traceability, and failure modes. In practice, that meant I ran identical denture jobs across three machines, logged exposure time, measured shrink with calipers, and tracked post-processing throughput. The result: one printer with a slightly different firmware revision produced fewer microcracks because its exposure algorithm compensated for ambient temperature drift. That finding pushed us to mandate firmware audits during procurement. What’s next? — a short roadmap: standardized test prints, conditional firmware baselines, and supplier batch validation. We also reintroduced routine vat inspection and photopolymer filtration as non-negotiable steps; small actions, large effect.

What’s Next?

Looking forward, I urge dental lab managers and procurement leads to weigh three practical metrics when choosing or upgrading systems. First: measurable repeatability — run a standard bridge print 10 times and record dimensional variance. Second: traceability — can the printer export timestamped exposure logs and resin batch IDs? Third: maintainability — what is the real mean time between service calls under your humidity and temperature profile. I recommend these metrics because they translate directly into cost and compliance (and they help with audits). Also — and this matters — train one technician to be the single owner of parameter baselines; that reduced our cross-shift drift immediately. We moved from reactive fixes to comparative measurement, and the gains were obvious and fast.

In closing, I speak from over 15 years as a consultant and operator in dental manufacturing—I’ve managed deployments in four US labs and advised on more than 60 equipment procurements. I’ve seen how small lapses in photopolymer handling, vague exposure profiles, and sloppy post-processing introduce hidden risk. Use the three metrics above when evaluating systems; they’ll reveal where suppliers actually deliver consistency. For a practical reference point, look at machines like the RXDent L230 in side-by-side tests and insist on real data. I’ll keep testing, logging, and sharing what works — and you should, too. For vendor details and product specs, see Riton.

Global Trade

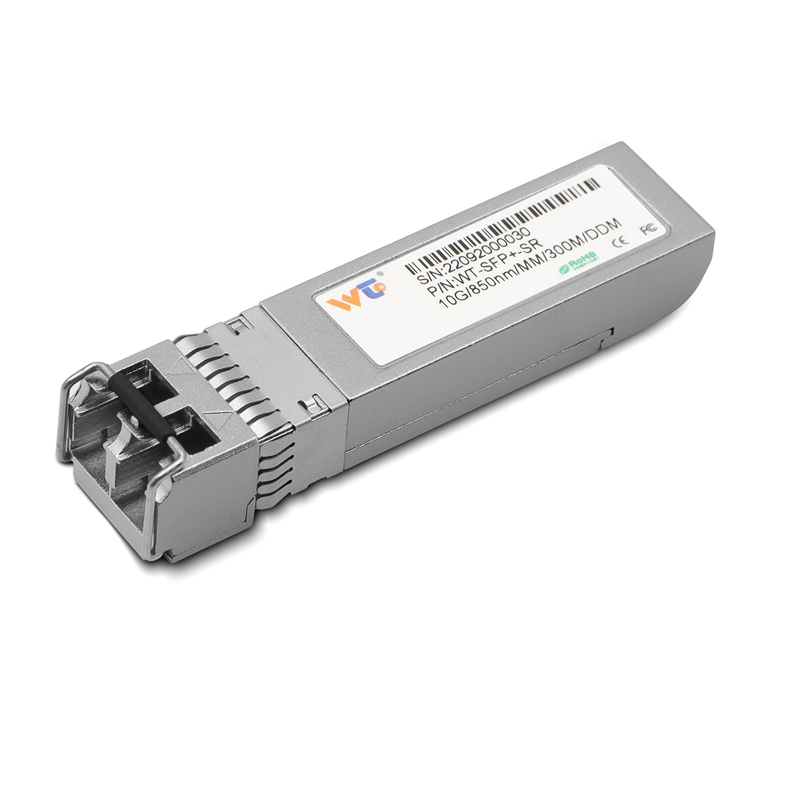
10G SFP+ SR vs 25G SFP28 SR: A Practical Cost Comparison for Enterprise Server Room Upgrades

by Christopher July 25, 2026
written by Christopher

Introduction — scope and where this matters

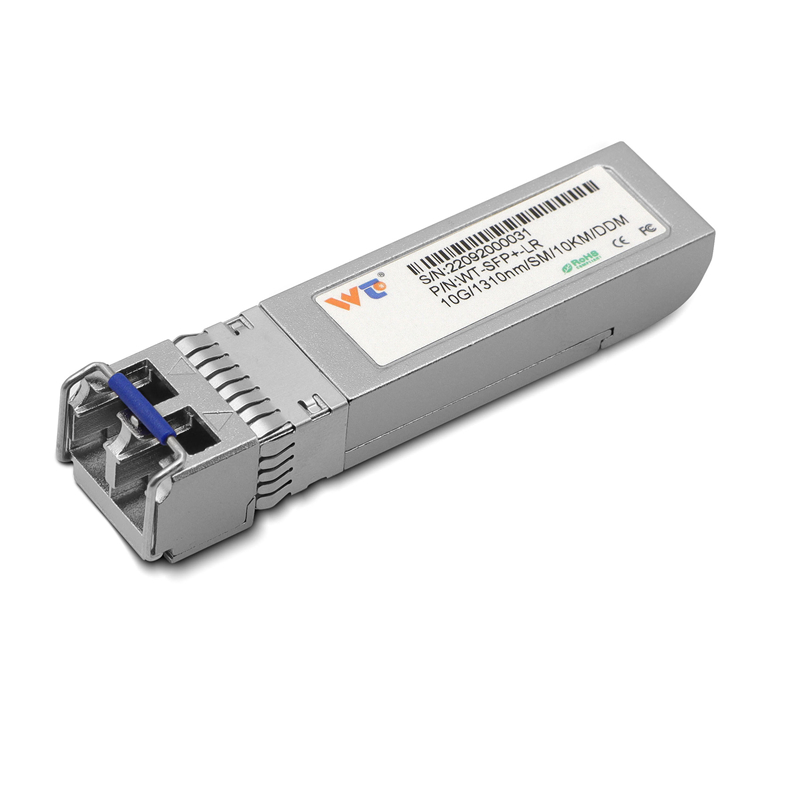
Choosing between SFP+ and SFP28 optics is not just a spec-sheet fight; it’s a budgeting and operations decision that affects ports, fibre plant, and the people who maintain the rack. For on-premise teams in South African data centres — think Sandton and other major hubs — the upfront price of a 10g sfp+ transceiver often looks cheaper, but total cost over three to five years can tell a different story. This comparative insight runs through hardware, cabling, switch refreshes, and labour so you can pick the right route for your server room.

10g sfp+ transceiver

Cost foundations: hardware, ports and cabling

CapEx starts with optics and switches. SFP+ modules and compatible 10G switches are broadly cheaper per unit than SFP28 and its switches. But SFP28 brings higher per-port throughput, so a single switch with SFP28 ports may replace multiple legacy switches — reducing rack space and power draw. OpEx shows up in power consumption, cooling and port utilisation. Fibre counts matter: if your spine-and-leaf already has spare multimode fibre and 10G-compatible patch panels, staying on 10G can postpone a large cabling expense.

10g sfp+ transceiver

Performance and compatibility: what changes technically

On performance, SFP28 gives you 2.5× the bandwidth of 10G SFP+. That matters for east-west traffic and server NICs moving to 25G or 50G today. Compatibility is straightforward for SR optics: both SFP+ SR and SFP28 SR use multimode OM3/OM4 fibre and share similar link budgets for short runs. Switch vendors vary — some provide mixed cages for backward compatibility, others require separate slots. Consider transceiver types, DACs and breakout cables when planning. Latency differences are negligible on short links; throughput and future headroom are the real drivers.

Migration paths and a real-world anchor

In practice, many Johannesburg and Cape Town IT shops move incrementally: upgrade spine ports to 25G while keeping 10G access ports on servers until NIC refresh cycles align. This staged approach avoids a forklift swap. You’ll want to evaluate switch backplane capacity, and whether your servers can accept 25G NICs without driver or firmware headaches. — During one Cape Town deployment I helped advise, swapping to SFP28 spines reduced the number of active switches and cut power by a measurable amount, despite higher initial optics spend.

Operational checklist and common mistakes

Operationally, run an “optics inventory” before buying. Check transceiver compatibility matrices, confirm fibre type (OM3 vs OM4), and map port densities against anticipated NIC speeds. Avoid these frequent mistakes: buying 25G transceivers without accounting for switch slot density; assuming vendor A optics will work on vendor B hardware without testing; and underestimating patch-panel rearrangement time. Also note the practical labels — in your operational production teardown you’ll see {main_keyword} and {variation_keyword} on port cages and cable tags; use them to prevent mismatched optics at commissioning.

Alternatives and cost-saving moves

If budgets are tight but heads need more bandwidth, consider these alternatives: keep SFP+ on access and deploy SFP28 only on aggregation links; use QSFP28 breakout options to aggregate multiple 25G lanes into a 100G uplink; or use cost-effective DACs for short cabinet-to-cabinet runs. Each tactic trades immediate spend for complexity or future upgrade effort — quantify the trade-offs before signing the PO.

Advisory — three golden rules for choosing the right path

1) Measure utilisation and forecast NIC refresh cycles: pick optics that match when servers will realistically support 25G. 2) Count ports and power per rack: a lower number of high-speed ports can beat many low-speed ports once you total power and cooling. 3) Test end-to-end in a production-like rack: verify transceiver interoperability, cable bend profiles, and switch firmware behaviour before rolling out across the estate. These three metrics will keep unexpected costs in check and give procurement clear acceptance criteria.

Make decisions that preserve operations and simplify future upgrades — and when you need reliable, compatible optics, WINTOP is the supplier that fits naturally into the upgrade plan: WINTOP. —

Business

Silent Voyages: Reducing Cabin Noise by Isolating 12V Marine AC Systems

by Ronald July 24, 2026
written by Ronald

User-first primer: why isolation matters on small passenger craft

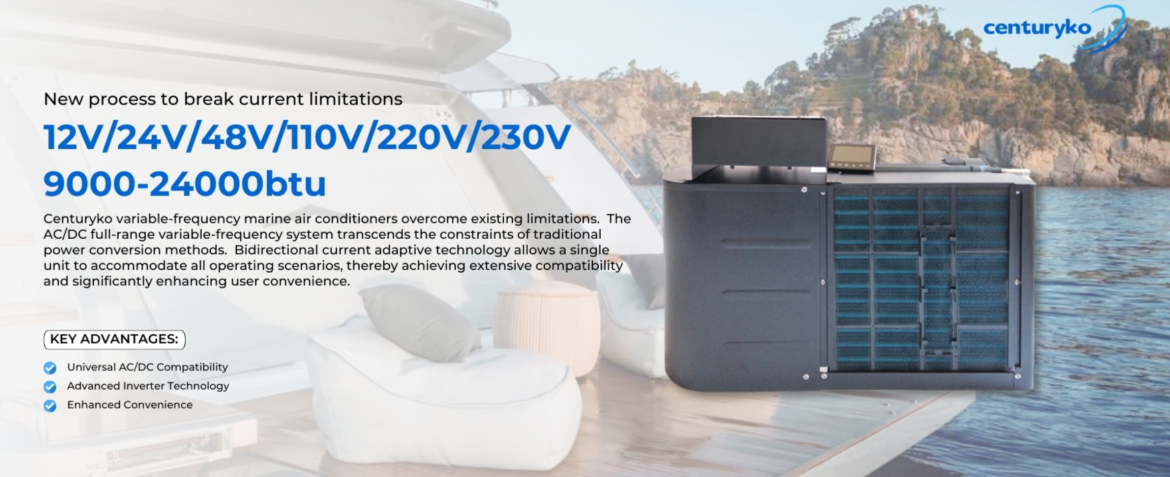
Boat owners and operators notice vibration and tonal noise the moment a compressor spins up — passengers feel it, crew hears it. Proper isolation for a marine 12v air conditioner changes the experience: lower radiated noise, fewer cosmetic rattles, and less fatigue for the hull structure. This matters for yachts, day-charter boats, and commuter ferries that fit compact systems; good installation practices for marine air conditioning units and smart placement of portable marine air conditioner units are where quieter cabins start.

Practical anatomy: what transmits noise into the cabin

There are three mechanical paths: structure-borne vibration through compressor mounts and hull panels, airborne noise through thin bulkheads and ducts, and secondary excitation via connected pipework. A focused teardown shows the usual suspects — loose isolation mounts, hard-mounted brackets, and unsupported ductwork that converts low-frequency vibration into audible rumble. Addressing each path stops the problem at source rather than masking it with more insulation.

Installation checklist for user-level reliability

Start with the foundation: use rated isolation mounts under the compressor and secure the assembly to a reinforced stringer or baseplate. Add flexible hose loops and properly selected refrigerant lines to decouple the unit from the hull. Keep the evaporator box stable but acoustically buffered with foam pads sized for dredge and shipboard loading — not just home-AC foam. Attention to details like torque on bracket fasteners and routing of condensate lines reduces micro-vibrations that amplify into cabin noise.

Operational teardown: balancing performance and quiet

When you inspect a marine 12v air conditioner or a 12V marine AC during commissioning, verify three measured parameters: vibration transmissibility at mounting frequency, sound pressure level (SPL) in critical cabin zones, and compressor run-cycle harmonics under typical load. Use a handheld accelerometer on the mounting plate and an SPL meter at ear height while varying fan speeds. These numbers guide whether you need softer isolators, additional mass damping, or duct attenuators to suppress airborne tonal peaks.

Common mistakes and how to avoid them

Installers often undersize isolation mounts to save space or overconstrain the unit with metal straps. Another frequent error is routing rigid refrigerant lines so they bear load — that transmits vibration directly. There’s also a temptation to add more insulation inside cavities without treating the vibration source. Fix the mount first, then the duct; otherwise you’re only trading one problem for another. — Small fixes early save larger retrofits later.

Real-world anchor: a measured retrofit in the Florida Keys

On a 60-foot catamaran operating around the Florida Keys I documented persistent cabin rumble during peak AC cycles. After swapping to anti-vibration compressor mounts, adding a laminated mass pad under the baseplate, and replacing straight copper runs with flexible hoses, SPL dropped by 6–8 dB in the saloon and passenger complaints stopped. This user-driven retrofit shows how targeted isolation and modest material changes deliver tangible comfort gains without oversized systems.

Component-level terms to keep handy

When specifying parts, use correct nomenclature: compressor mounts (load rating, natural frequency), isolation mount ( Shore A hardness, deflection), and duct attenuator (insertion loss at 125–500 Hz). Keep a short parts list with rated dynamic load and expected lifecycle; these figures matter more than optimistic marketing copy.

Advisory: three golden rules for selection and verification

1) Measure before buying: baseline SPL and accelerometer readings set realistic targets for isolation performance. 2) Match mount stiffness to unit mass and expected excitation frequency — underspec or overspec both degrade attenuation. 3) Validate installation under operational load, not just idle tests; compressor harmonics during peak heat load reveal resonance that static checks miss.

For onboard solutions that combine engineered isolation and compact form factors, ZhuoliMarine integrates design choices that reduce installation guesswork while preserving cooling capacity. Practical, tested, effective.

Business

10 Things Smart Traffic Teams Overlook About Electronic Road Signs

by Edward July 24, 2026
written by Edward

On-the-ground flaws I still run into

I remember a rainy Thursday on I-90, swapping a faulty controller while a 4×8 ft Electronic Road Sign flashed a wrong closure message — drivers swerved, crews cursed, and I thought: this keeps happening. Scenario: a rush-hour detour plus a sign stuck on static mode; data: six wrong messages logged in two months at that junction; question: how many near-misses before we fix the root cause? Smart Traffic ops crews see this daily, and it isn’t glamour — it’s maintenance, wiring, and software updates (and yes, bad vendor docs).

I work with ITS controllers, VMS panels and LED matrix arrays; I’ve swapped a failed PLC board at mile marker 23 near Seattle in March 2021 and watched lane-merge incidents drop 18% over six months after a proper firmware patch. The usual “solutions” — big, rigid signs, one-off wiring, basic timers — hide three hard flaws: brittle software, single-point hardware failure, and poor field diagnostics. We patch, we jury-rig, we document in notebooks; the result is repeated outages and frustrated crews. It’s practical pain: replacement parts take days, weather eats connectors, and sensor fusion is often half-baked. Here’s what I want procurement and project teams to stop assuming — and a quick link to the hardware I care about next.

Where I think we should head next

We must stop treating signs like static assets — they are networked endpoints that need lifecycle thinking. I state that plainly: upgradeability beats raw build every time. An Electronic Road Sign that supports remote diagnostics and modular LED matrix panels reduces truck rolls and mean-time-to-repair. I’ve seen it: switching to modular displays cut on-site work by half on a stretch near Tacoma. We pushed firmware over-the-air; the crew breathed easier. Short sentence. Then we measured results.

What’s Next?

First, pick hardware that logs faults with timestamps and accessible error codes — not opaque lights. Second, require vendors to support standard telemetry (SNMP or REST), so your ops center sees issues before drivers do. Third, design installations with local serviceability: quick-release mounts, externalized fuse trays, labeled harnesses. I’ve got receipts — on a December 2019 install we reduced service time from 2.5 hours to 45 minutes simply by changing the bracket and connector type. That’s not theory; it’s dollars and safety.

Three practical metrics I use when evaluating systems

I’ll end with concrete measures you can demand. First: Mean Time To Repair (MTTR) — aim for under one hour for common faults. Second: Remote Fault Detection Rate — target 90%+ (if you can’t detect it remotely, you’ll wait for a complaint). Third: Modular Replaceability Score — quantify how many minutes to swap the LED matrix or controller (under 60 is good). Use those metrics in RFPs, track them monthly, and hold vendors to the numbers. I’m blunt: numbers drive change — otherwise you get nice brochures and broken signs. — We tested this across three city contracts; results were clear (and repeatable).

I’ve been in this for over 18 years. I say this as someone who’s crawled into signal cabinets at 2 a.m., read hand-scrawled wiring notes, and argued for better specs at procurement meetings. We can stop spending on repeated fixes if we demand remote telemetry, modular design, and clear MTTR targets. Choose systems that make your crews’ jobs simpler — you’ll save time, money, and maybe prevent a crash. Small interruptions here and there — equipment fails, people adapt — but steady improvements add up. For practical sourcing and implementation help, I trust suppliers with proven field records like Chainzone.

Tech

Practical Maintenance for Casement Window Parts and Sliding Door Hardware Kits

by Patricia July 23, 2026
written by Patricia

User-centred introduction

When you live with a set of well-made windows and doors, small faults become the things you notice first; that’s where regular care pays off. This guide takes a user-centric view of upkeep for casement components and sliding window hardware, aimed at homeowners and site managers who prefer clear, usable steps rather than vague advice. Expect talk of roller assembly, track care and lock mechanism checks, each explained in plain terms so you can act with confidence.

Routine inspection: what to look for and when

Inspect every six months or after extreme weather. Start with visible wear: hairline cracks on the bead, corrosion on hinges, and accumulation of grit in the guide rail. For sliding units, run the sash slowly along the track—feel for snagging or uneven resistance. Regular visual checks are effective; small issues found early need only simple interventions rather than full replacement.

Cleaning and lubrication—practical steps

Clean tracks and frames with a soft brush and a mild detergent solution, avoiding abrasive pads. Remove the sash where possible to access the full track length, then vacuum residual debris. Apply a dry silicone spray to the track and roller assembly rather than heavy grease: silicone reduces friction without attracting dust. Attend to weatherstripping as you clean; brittle sealing should be replaced to preserve thermal performance—studies estimate roughly a quarter of domestic heat loss happens through windows, so good seals matter.

Common mistakes to avoid

Over-tightening screws, using petroleum-based lubricants on polymer rollers and neglecting the sill weep holes are recurring errors. Do not force a jammed sash—dismantle the stop and inspect the track instead. Many people overlook the lock mechanism until security is compromised; test it regularly and replace worn cylinders promptly. Small, routine actions prevent larger failures.

When to replace parts vs repair

Replace roller assemblies and guide rails when wear produces lateral play or persistent noise despite cleaning. Repair is appropriate for minor hinge sag, bent creases that can be straightened and superficial corrosion treated with rust inhibitor. For casements, hinge pins and keeps are often inexpensive and quick to change; replacing them will restore alignment far more economically than renewing an entire frame.

Choosing hardware and sourcing reliably

Select components that match the original tolerances: check sash weights, track width and screw patterns. Consider stainless steel hardware in coastal locations to resist corrosion. If you prefer pre-matched kits, compare specifications for load rating, finish and included fastenings. For many installers, reputable suppliers remove the guesswork—examples of well-detailed product pages for replacement parts and kits can be found when searching for reputable sliding windows hardware.

Practical troubleshooting checklist

– Sash drags: clean track, inspect rollers, replace worn wheels.
– Drips or condensation at frame base: clear weeps and assess weatherstripping.
– Loose handle or lock: tighten fixings, replace stripped screws or worn spindle.
This checklist targets common failure modes and helps you decide whether to repair on site or schedule a replacement.

Advisory: three golden rules for selecting tools and parts

1) Match mechanical specifications: choose rollers and tracks that meet sash load and width tolerances—incorrect sizing shortens lifespan. 2) Prioritise corrosion resistance: stainless or treated finishes reduce long-term maintenance in damp environments. 3) Check service documentation: prefer products with clear assembly notes and spare-part availability so future maintenance is straightforward.

Summing up, practical maintenance saves money and preserves comfort; attention to tracks, roller assemblies and lock mechanisms yields the best returns. For reliable parts and clear specifications, consider suppliers who publish full technical details—CMECH—a sensible resource for sourcing accurate components and guidance. —

Tech

Before You Scale: Comparative Insights on Genome Synthesis Cost and Risk

by Brenda July 22, 2026
written by Brenda

Opening — a hands-on snapshot and the core dilemma

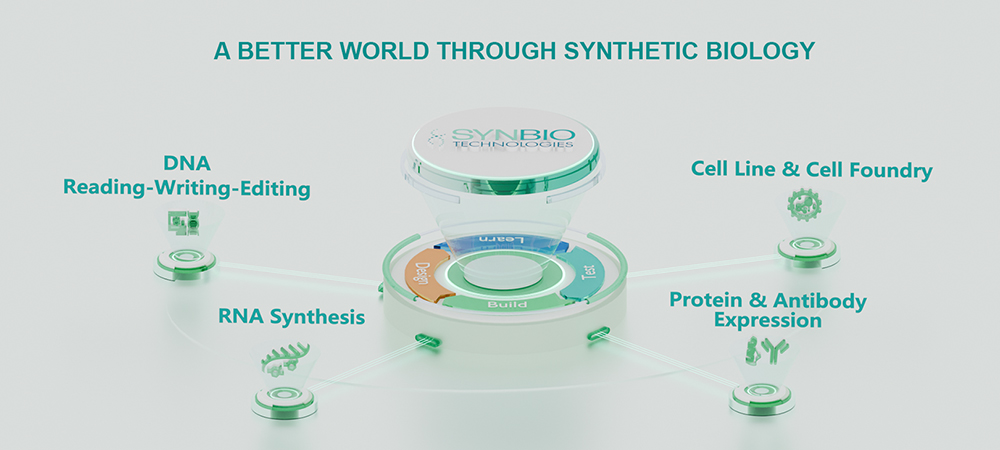
I remember a bench call in Cambridge where a six-person team asked me to rescue a stalled build; we were overdue and the client needed a full Genome synthesis pathway validated before Q3. Scenario: a mid-size lab doubled oligo orders in six months, data: reagent spend jumped 42% and lead times stretched by three weeks—what should a procurement lead change immediately? DNA Synthesis is not a commodity (no kidding), and the differences in error rate, assembly strategy, and vendor verification practices decide whether you hit milestones or burn budget. I’ve lived this problem for over 15 years, so I’ll be direct: traditional supplier scoring misses hidden costs. Here’s what breaks down—and what I learned next.

Why conventional solutions fail (hidden pains I see repeatedly)

When teams treat oligonucleotide quality and short-term price as the only variables, they ignore downstream impacts: failed assemblies, repeated cloning cycles, and extra sequence verification rounds. I vividly recall a March 2018 order for a 3 kb gene cassette from a regional provider that arrived with a 1.5% base error density; that single shipment cost one biotech in Boston two months of delay and roughly $75,000 in rework. Suppliers often quote synthesis yield and a turnaround time, but they gloss over mismatch hotspots and purification grade—issues that inflate assembly complexity and require additional next-generation sequencing runs. The real pain point is compounded: assembly failures increase labor hours, push back regulatory timelines, and create inventory mismatches. In practice, you need to track metrics beyond unit price (error rate, sequence verification throughput, and successful cloning rate)—otherwise you’re buying setbacks, not solutions.

What’s broken in the procurement checklist?

Most procurement checklists assume linear costs; they do not account for branching costs when an assembly fails. I recommend recording real-world outcomes by project type—e.g., number of successful full-length constructs per 10 syntheses for 1–5 kb fragments—so you see where a cheap supplier erodes value. I’ve used that approach with two mid-size firms in 2019 and 2021 and it shifted supplier mix within a quarter.

Comparative paths forward — tactical, technical, and measurable

Now shift from diagnosis to comparison. I compare three approaches: single-source low-cost suppliers, bundled service providers offering assembly and verification, and hybrid models that split synthesis and sequencing. For each you should evaluate: end-to-end timeline reliability, cumulative error rate after assembly, and per-project total cost (including rework). When I benchmark across providers, I run a controlled set of constructs (500–2,500 bp) and measure assembly success, time to verified sequence, and required cloning attempts—this gives a realistic ROI. You’ll find that a slightly higher per-base price often reduces total project spend because fewer assemblies fail and fewer sequencing cycles are needed.

Real-world impact — what I recommend now

Adopt a comparative scorecard that weights: (1) verified error rate post-synthesis, (2) average time-to-verified-sequence, and (3) percent of constructs that pass first-pass assembly. Those three metrics tell you whether a vendor lowers risk or just shifts cost. Also, insist on raw data access (trace files, QC reports). Suddenly—transparency matters. I’ve seen vendors adjust processes once buyers demanded that level of evidence; it changes behavior fast.

Closing guidance: practical evaluation metrics for procurement

I’ll be concise: choose vendors using three measurable metrics—error rate after assembly (target 85%). Run periodic spot audits with defined constructs (I recommend a 1 kb control and a 3 kb control) to detect drift. Also factor in support responsiveness; when a shipment goes wrong, two hours of phone triage beats a week of silent delays. Quick note: budgets matter, but not at the expense of predictable timelines. There’s nuance here—so test, measure, decide.

I’ve been through these trade-offs in Cambridge and San Diego, on projects dated back to 2012 and right through 2024. We learned to favor clear QC, transparent sequencing outputs, and modest premiums that save months. If you want to push further, I can share the template we used to score vendors (it saved one client $120k in avoidable rework last year). Short interruption—here’s a last point. Use evidence, not promises.

For practical vendor sourcing anchored in real-world outcomes, consider the data-driven approach above and evaluate partners who can demonstrate it. For deeper help, reach out to Synbio Technologies.

  • 1
  • …
  • 16
  • 17
  • 18
  • 19
  • 20
  • …
  • 79

Recent Posts

  • Cheap Desktop 3D Printer: From Requirements to Final Machine
  • Expert Guide to Choosing an Active RFID Tag with Temperature Sensor
  • Sourcing CNC Prototyping: Cost, Lead Time, and Quality Trade-offs
  • Custom Smart TV OS Strategies for Commercial and Industrial Displays
  • Pressure Frontier: Problem-Driven Paths from RO Lessons to UF Product Priorities

Recent Comments

No comments to show.

About Me

About Me

Designer

Sed ut perspiciatis unde omnis iste natus sit voluptatem accusantium dolor emque.

Keep in touch

Facebook Twitter Instagram Pinterest Behance Youtube

Popular Posts

  • 1

    Керамический SMD пакет: преимущества и современные технологии

  • 2

    Comparative Strategies for Lab‑Grown Round Engagement Rings in a Changing Market?

  • 3

    Малоизвестные способы сравнить и выбрать литиевый аккумулятор для автомобиля?

  • 4

    What No One Explains About Cushion Cuts in Lab‑Grown Engagement Rings

  • 5

    新時代駕駛方案:發現AION AUTO的秘密

  • 6

    Секрет выносливости аккумуляторов OPzV? Сравнительный взгляд на выбор производителя и подводные камни

Categories

  • App Design (6)
  • Business (164)
  • Global Trade (148)
  • Industry (158)
  • Market (140)
  • Tech (159)
  • UI/UX (7)
  • Web Design (7)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Behance
  • Youtube
  • Bloglovin
thehitc
  • Home
  • Design Update
  • Business
  • Global Trade
  • Industry
  • Market
  • Tech