The problem
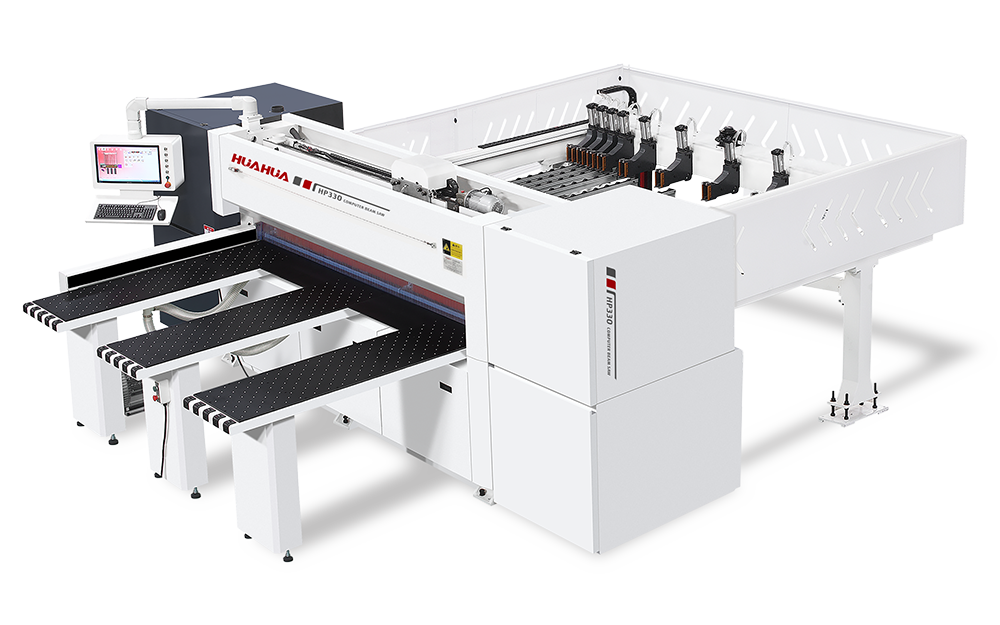
Local workshops that add automated tooling often expect immediate throughput gains; instead they find new bottlenecks — mismatched tooling, inconsistent material flows and operator confusion around equipment like the beam saw machine. This is a problem-driven diagnosis: the machine-level gains exist, but regional integration failures prevent those gains from showing up on the factory floor. The priority is clear — identify the integration gaps that turn capital investment into near-term waste.
Where integration breaks down
Three predictable failure modes cause the drag. First, process mismatch: layouts and material sequencing that fit legacy saws don’t match CNC cycle requirements. Second, data fragmentation: programs, cut lists and nesting files live in silos and get rekeyed, creating waste and errors. Third, skill mismatch: operators trained on manual methods struggle with CNC toolpath logic and maintenance. Each failure mode compounds the others and reduces achievable output.
Operational impacts you can measure
Expect measurable consequences: higher scrap rates, longer setup times, increased overtime to catch up on orders, and lower machine utilization. These aren’t abstractions — they show up as daily throughput variance, missed delivery windows and margin erosion. Quantify by tracking scrap per job, average setup minutes per shift and percentage of runtime under active cutting versus idle.
Fixes that work in the field
Fixes must be tactical and sequential. Standardize material kitting and staging so the beam saw and CNC cells receive consistent inputs; eliminate manual rekeying by using a single nesting-to-machine data flow; adopt a strict preventive-maintenance cadence for spindles, vacuum tables and linear guides. Train a small cross-functional team to own first-run validation and error resolution. Consider temporary outsourcing for peak loads while the in-house line stabilizes. Avoid piecemeal software swaps without workflow redesign; that’s a common trap that simply moves the bottleneck.
Evidence and practical authority
Years of deployment across regional furniture clusters show the same pattern: when a shop aligns material flow, digital nesting and operator routines, cycle times fall and yield rises. At major industry gatherings such as the International Woodworking Fair (IWF) in Atlanta, manufacturers demonstrate how CNC cells paired with disciplined layout reduce secondary handling. For hands-on comparison, examine a modern cnc cutting panel integration versus legacy line retrofits — the differences appear in setup frequency and downstream rework rates.
Common pitfalls to avoid
Don’t assume machine throughput equals plant throughput. Don’t defer training until after installation. Don’t let IT and production operate on different file standards. Don’t chase the highest spindle speed as the sole performance metric. Each misstep increases friction and masks the true return on equipment investment.
Practical checklist for regional projects
Map material flow and identify two points of touch per part; standardize file formats and enforce a single source of nesting; schedule preventive maintenance with measured KPIs; create a cross-trained pilot crew for the first 90 days; run acceptance tests that include scrap rate and setup time benchmarks rather than just cycle time. Measure, iterate, and lock successful routines into standard work.
Conclusion
Regional CNC adoption improves output only when integration is deliberate: align physical flow, unify digital files and build operator competence. The solution is operational, not purely technological, and it’s achieved through focused changes that reduce handoffs and clarify responsibility. For organizations building that bridge between machine capability and plant throughput, HUAHUA CNC represents a practical partner in aligning equipment selection with workflow realities.