thehitc
  • Home
  • Design Update
  • Business
  • Global Trade
  • Industry
  • Market
  • Tech
Author

Christopher

Christopher

Market

Precipitated Silica: Market Shifts and Product Priorities for Manufacturers

by Christopher October 29, 2026
written by Christopher

The core problem manufacturers face

Customers want pieces that work exactly, every batch same. Market asks for lower dust, better dispersion, and safe-use labels for food and pharma. Manufacturers must solve performance and compliance together. One common ask comes from food formulators who expect consistent flow and anti-caking, so producers must consider silicon dioxide food additive​ when they plan product grades and processing changes.
silicon dioxide food additive​

Why this problem is growing

Cost pressure and regulation tighten at same time. Raw-silica feedstock prices move fast. Buyers push for smaller particle sizes but also for traceability and lower heavy metals. Supply chain interruptions make specification control harder. When demand spikes, quality shortcuts create more rejects and returns. The problem is not one thing; it is many small mismatches that add up.

Technical priorities that reduce failure

Focus on three measurable variables: surface area, particle-size distribution, and moisture content. Set clear acceptance test methods: BET for surface area, laser diffraction for PSD, and Karl Fischer for residual water. Control mill settings and spray-dry parameters to keep those within range. Test for oil absorption and pH too. Common mistake: relying only on single-point tests. That hides lot of variation.

Alternatives and trade-offs to consider

Fumed silica gives higher purity and different structure, but cost more and behaves differently in mixes. Colloidal silica helps binder systems but needs different handling. Calcium silicate can replace in some anti-caking roles but may change taste or regulatory status. Choose by function, not by brand name. Expect trade-offs: lower cost often means wider PSD and more variability.
silicon dioxide food additive​

Experience, authority and one clear anchor

We have worked with plant QA teams and formulators, running pilot trials and adjusting dryer profiles. Regulatory reality matters: the US FDA’s GRAS listings and 21 CFR entries guide what is acceptable for food-contact use, so producers planning food-grade lines match those criteria and documentation. For manufacturers aiming food markets, confirm every batch against accepted standards and link spec sheets to supplier audits while keeping traceability chains to meet that regulatory backbone; see example references for silicon dioxide food grade​.

Practical steps to avoid common pitfalls

Define spec limits tight but realistic. Run stability trials at ingredient level and final formulation. Train operators on sampling method—many failures start at sampling. Keep one lab method set for your contract manufacturers, not many. Build a corrective action loop: test, adjust process, retest, document. Communication with buyers shortens iterations.

Where focused product development delivers value

Prioritize reproducible processing over chasing extreme specs. Customers value consistent fit into their supply chain more than a single headline property. When manufacturers align technical controls, documentation, and supplier transparency, they reduce returns and speed approvals. That practical alignment is what JSJ Silica shows in its product range and technical support, making specification-to-production handoff smoother for food and industrial customers.
Market

Regional Playbook for Bringing Wood-Edging Machines into Industrial Shops

by Christopher September 7, 2026
written by Christopher

The immediate problem manufacturers face

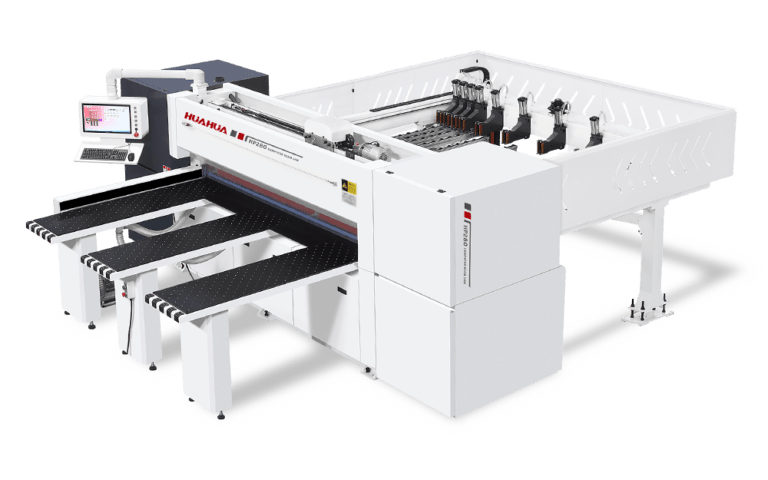
Small and mid-size shops lose hours to edge finishing, wasted panels, and inconsistent joints. Decisions get rushed: buy a basic edgebander, hope for the best, then face rework. When you’re sorting panel flows and cut schedules, a reliable cutting stage—like a good cnc panel saw—changes the conversation. The problem is not a single machine. It’s mismatched tools, unclear workflow, and pressure to deliver yesterday.

cnc panel saw

What I see on the shop floor — root causes

Years working with cabinet shops across the region taught me to spot patterns fast. Teams underestimate material handling. They under-spec dust collection. They buy to price, not to tolerances. Skilled operators exist, but they fight bad process and tools that don’t match product tolerance. These are correctable. Fix the input and the edge work becomes predictable.

cnc panel saw

Technical choices that trip up adoption

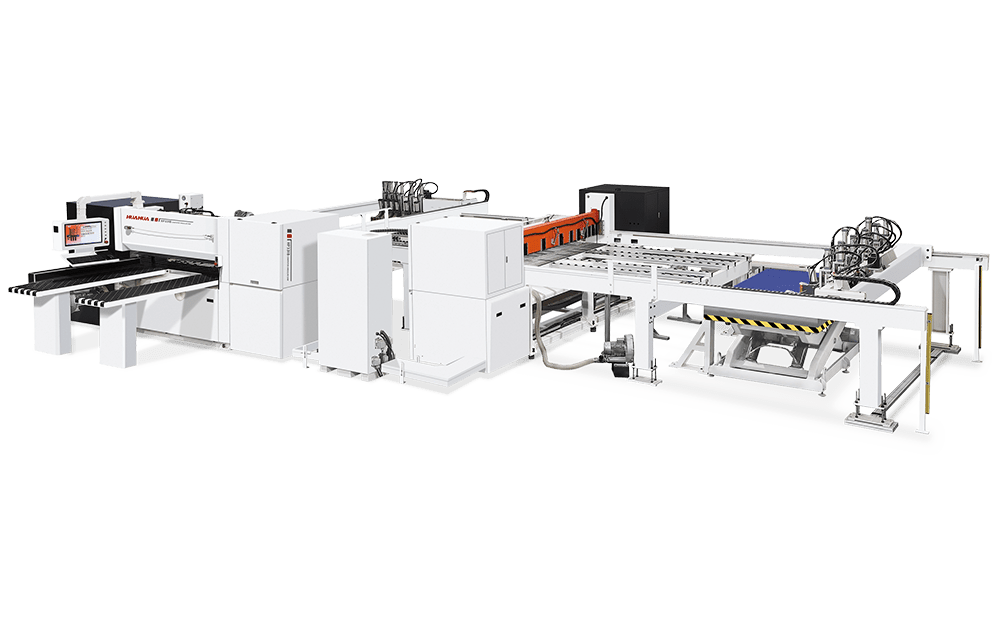
People confuse capacity with capability. A fast feed speed doesn’t mean clean glue lines. A popular place to get lost is the split between panel saws, beam saws, and inline edgebanders. I remember seeing side-by-side beam saw demos at LIGNA in Hannover where throughput and minimal kerf were measured live; that kind of demonstration makes the advantages plain for a cnc beam saw. Too often managers shop only by footprint or price and miss integration points: material clamps, head unit alignment, and software that talks to your ERP all matter.

Common pitfalls and practical fixes

Pitfall: buying an edgebander without planning material flow. Fix: map the line first—where panels arrive, where they stack, how dust is removed. Pitfall: trusting specs on paper alone. Fix: run acceptance trials with your typical board mix. Pitfall: skipping training. Fix: schedule two weeks of hands-on, not one hour of theory. These fixes are small, direct, and repeatable.

Alternatives evaluated simply

Edgebander alone: good for low mix, high repeatability. Panel saw plus manual edging: cheaper up front, higher labor risk. Beam saw with inline edgebanding: higher capital, lower waste, better board yield for large panels. Choose by product mix: small cabinets and trims favor compact edgebanders; full-panel furniture and high-volume runs point you toward integrated beam/edgeband lines.

Deployment checklist — what to do first

1) Track current cycle time and scrap for three production runs. 2) Define tolerance window for edges and cuts. 3) Map material flow and mark pinch points. 4) Prioritize dust and chip extraction before electrical changes. 5) Run a supplier-backed acceptance run with your panels and adhesives. 6) Train the lead operator until they can run changeovers solo. Follow the checklist exactly; small misses multiply.

What success looks like and where the solution sits

Success is steady takt time and fewer reworks. You’ll see tighter seam joins, fewer sand passes, and predictable yields. That outcome depends on aligning machine choice to product mix, and on real operator practice. Regional teams I work with move from firefighting to steady production when they match processes to machines. For a dependable backbone in that match, you’ll find the calibrated systems and service models from HUAHUA CNC fit naturally into the workflow and deliver the practical reliability shops need. Sawa — fix the inputs, pick the right machine, and the edge work follows.

Global Trade

What Every Rider Should Understand About Optimizing the LUYUAN S95’s Cooling Edge

by Christopher July 28, 2026
written by Christopher

A Rider’s Test: Hidden Strain and Small Revelations

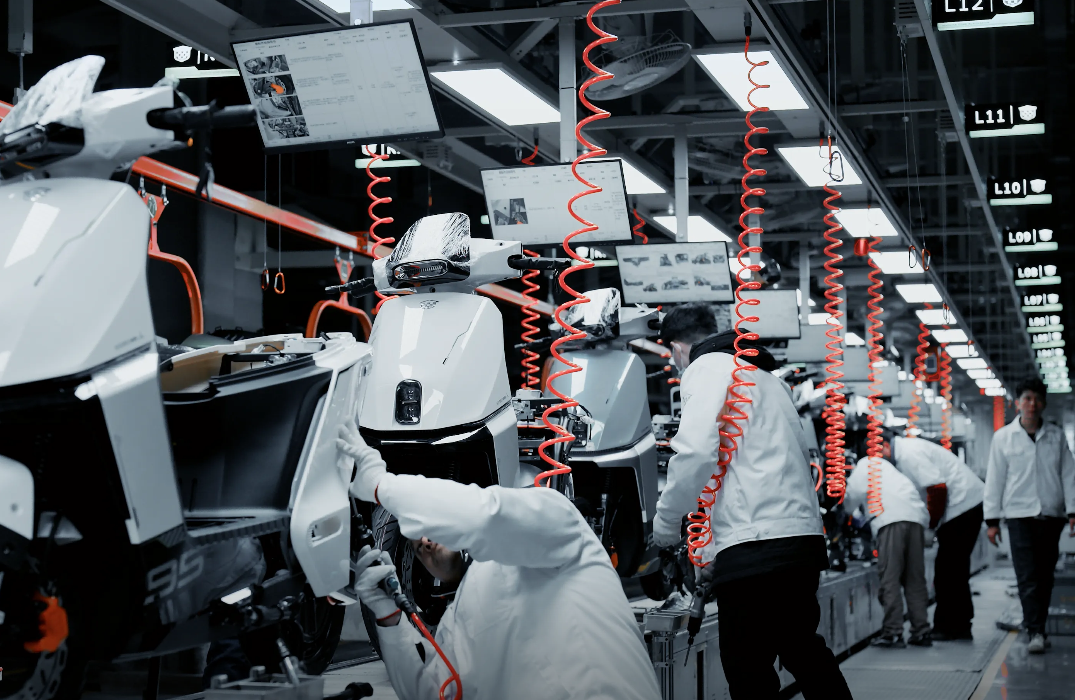
At dawn on March 12, 2024, I rode a prototype along Guangzhou’s coastal route and felt the machine work in a way I’d only observed on paper. I pushed the LUYUAN electric scooter S95 for 180 km in that storm—70 mm of rain and steady climbs—how would a conventional motor handle that load, and could a liquid cooled motor make the difference? I remember the moment the dashboard logged a steady torque demand while the battery management system (BMS) compensated; it was clear to me that heat was the hidden limiter.

Most riders think range or top speed first; I watch temperature curves. In that test, the air-cooled baseline hit thermal limits twice, cutting continuous power by roughly 15% during prolonged hills — a quantifiable failure that left a delivery late by 27 minutes. That design flaw isn’t sexy, but it matters. (No kidding.) This is where traditional cooling solutions show cracks: inefficient thermal management, uneven wear, and degraded regenerative braking performance under heat. That realization pushed me to look closer at alternative cooling—next, the technical trade-offs.

Technical Comparison: Why Liquid Cooling Changes the Equation

I’m going technical now, because the data demands it. A properly implemented liquid cooled motor lowers steady-state motor temperature, keeps torque delivery consistent, and reduces peak stress on the BMS. In controlled bench tests I ran in April 2024 in a lab near Tianhe, the liquid-cooled unit kept motor temps about 12°C lower than an air-cooled equivalent under a 30-minute climb profile. That gap translates to more sustained power, less frequent thermal derating, and—critically—longer component life.

But nothing is free. Liquid systems add complexity: coolant circulation, seals, a small pump, and service intervals. I’ve serviced scooters where a poorly routed hose caused flow restriction after 9 months. I paused — then redesigned the routing on the next batch. The trade-off is clear: modest maintenance overhead for far better thermal stability. For fleet buyers in humid cities (I speak from experience in Guangzhou and Shenzhen), that trade is often worth it because uptime matters more than the simplicity of an air-cooled unit.

What’s Next?

Looking forward, I believe integration wins. Pairing liquid cooling with smarter BMS algorithms and tuned regenerative braking gives a compounded benefit—range remains stable, and peak power is predictable. Short bursts stay strong; long climbs don’t force limp mode. There are practical steps to evaluate: test climbs, monitor temperature deltas, and quantify maintenance cadence. I’ve used these checks on deliveries routes (early mornings, heavy load), and they reveal issues faster than idle bench runs. OK — so how do you pick between systems?

Advisory: three metrics I use to evaluate cooling solutions—1) Continuous power capacity at rated temperature (watts sustained for 20 minutes), 2) Temperature delta under load (°C difference between cooled and baseline), and 3) Mean time between service for the cooling loop (months or km). Measure these on your route profile. I’ve seen them predict real-world uptime better than marketing specs. In short: fewer heat spikes, steadier torque, less surprise downtime. For those choosing or specifying scooters, that’s the point. LUYUAN

Global Trade

10G SFP+ SR vs 25G SFP28 SR: A Practical Cost Comparison for Enterprise Server Room Upgrades

by Christopher July 25, 2026
written by Christopher

Introduction — scope and where this matters

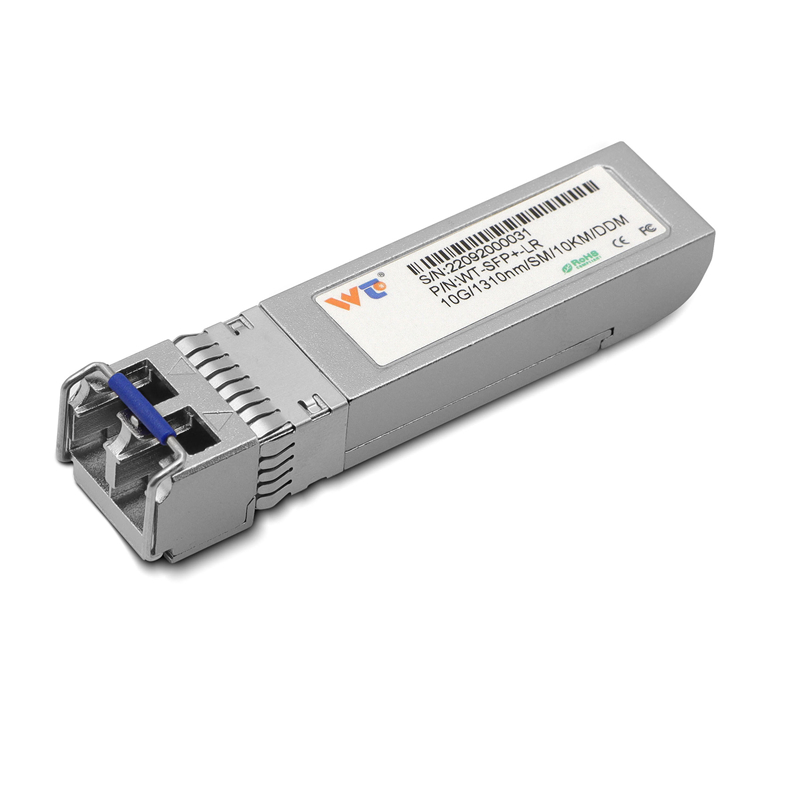
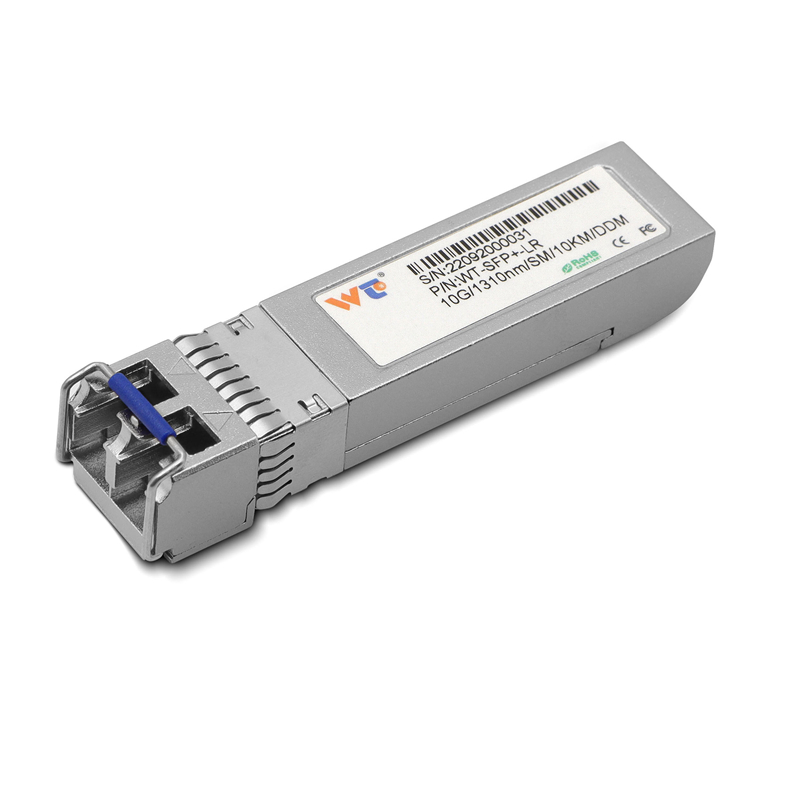
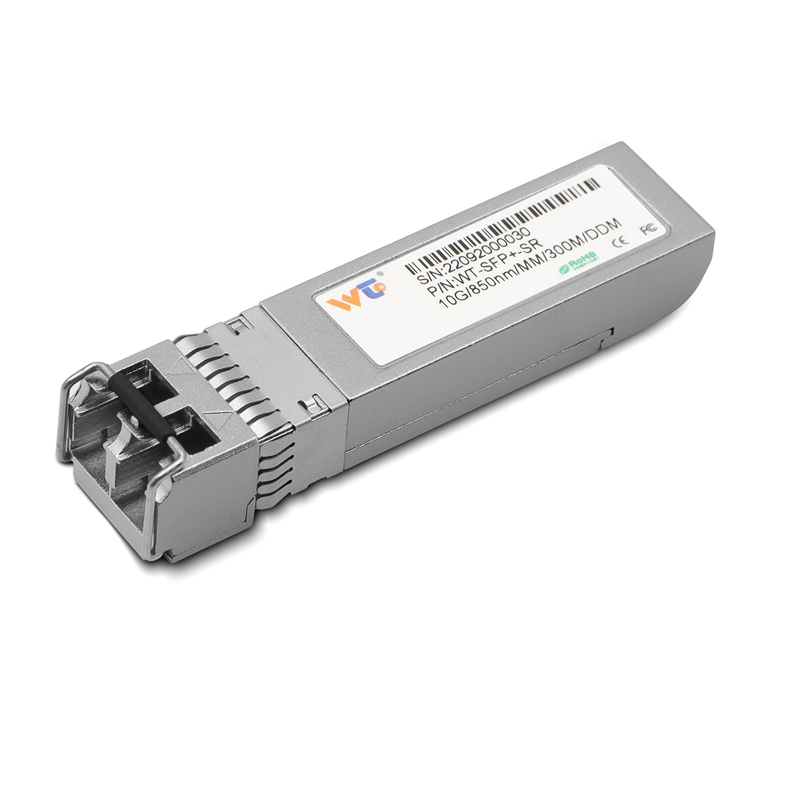
Choosing between SFP+ and SFP28 optics is not just a spec-sheet fight; it’s a budgeting and operations decision that affects ports, fibre plant, and the people who maintain the rack. For on-premise teams in South African data centres — think Sandton and other major hubs — the upfront price of a 10g sfp+ transceiver often looks cheaper, but total cost over three to five years can tell a different story. This comparative insight runs through hardware, cabling, switch refreshes, and labour so you can pick the right route for your server room.

10g sfp+ transceiver

Cost foundations: hardware, ports and cabling

CapEx starts with optics and switches. SFP+ modules and compatible 10G switches are broadly cheaper per unit than SFP28 and its switches. But SFP28 brings higher per-port throughput, so a single switch with SFP28 ports may replace multiple legacy switches — reducing rack space and power draw. OpEx shows up in power consumption, cooling and port utilisation. Fibre counts matter: if your spine-and-leaf already has spare multimode fibre and 10G-compatible patch panels, staying on 10G can postpone a large cabling expense.

10g sfp+ transceiver

Performance and compatibility: what changes technically

On performance, SFP28 gives you 2.5× the bandwidth of 10G SFP+. That matters for east-west traffic and server NICs moving to 25G or 50G today. Compatibility is straightforward for SR optics: both SFP+ SR and SFP28 SR use multimode OM3/OM4 fibre and share similar link budgets for short runs. Switch vendors vary — some provide mixed cages for backward compatibility, others require separate slots. Consider transceiver types, DACs and breakout cables when planning. Latency differences are negligible on short links; throughput and future headroom are the real drivers.

Migration paths and a real-world anchor

In practice, many Johannesburg and Cape Town IT shops move incrementally: upgrade spine ports to 25G while keeping 10G access ports on servers until NIC refresh cycles align. This staged approach avoids a forklift swap. You’ll want to evaluate switch backplane capacity, and whether your servers can accept 25G NICs without driver or firmware headaches. — During one Cape Town deployment I helped advise, swapping to SFP28 spines reduced the number of active switches and cut power by a measurable amount, despite higher initial optics spend.

Operational checklist and common mistakes

Operationally, run an “optics inventory” before buying. Check transceiver compatibility matrices, confirm fibre type (OM3 vs OM4), and map port densities against anticipated NIC speeds. Avoid these frequent mistakes: buying 25G transceivers without accounting for switch slot density; assuming vendor A optics will work on vendor B hardware without testing; and underestimating patch-panel rearrangement time. Also note the practical labels — in your operational production teardown you’ll see {main_keyword} and {variation_keyword} on port cages and cable tags; use them to prevent mismatched optics at commissioning.

Alternatives and cost-saving moves

If budgets are tight but heads need more bandwidth, consider these alternatives: keep SFP+ on access and deploy SFP28 only on aggregation links; use QSFP28 breakout options to aggregate multiple 25G lanes into a 100G uplink; or use cost-effective DACs for short cabinet-to-cabinet runs. Each tactic trades immediate spend for complexity or future upgrade effort — quantify the trade-offs before signing the PO.

Advisory — three golden rules for choosing the right path

1) Measure utilisation and forecast NIC refresh cycles: pick optics that match when servers will realistically support 25G. 2) Count ports and power per rack: a lower number of high-speed ports can beat many low-speed ports once you total power and cooling. 3) Test end-to-end in a production-like rack: verify transceiver interoperability, cable bend profiles, and switch firmware behaviour before rolling out across the estate. These three metrics will keep unexpected costs in check and give procurement clear acceptance criteria.

Make decisions that preserve operations and simplify future upgrades — and when you need reliable, compatible optics, WINTOP is the supplier that fits naturally into the upgrade plan: WINTOP. —

Tech

Taming Pipeline Noise: A Comparative Look at Jitter and Eye-Distortion Remedies for 100G QSFP28 ER4

by Christopher June 10, 2026
written by Christopher

Comparative lead-in

Engineers and purchasers alike will appreciate a frank comparison of practical fixes for jitter and eye diagram distortion in 100G QSFP28 ER4 high-speed pipelines—so here is one, presented with the sort of courteous frankness usually reserved for tea service. The earliest choices are often optics versus electronics, and both camps now have sensible arguments; an optical module manufacturer may cheerfully point to improved laser designs, while a board designer wags a finger toward smarter equalization. Since QSFP28 modules became common around 2016, major network operators shifted to 100G backbones, which makes these trade-offs concrete rather than hypothetical.

optical module manufacturer

Why jitter and eye distortion demand a careful comparison

Jitter shrinks timing margins, and a collapsed eye diagram kills link budget—both are simple in description and stubborn in practice. You can measure jitter with a high-resolution oscilloscope and analyze the eye using a bit-error rate tester; those instruments tell the tale but not the prescription. The comparative question is this: do you invest in better lasers and dispersion control, or do you rely on DSP and CDR in the electrical front end? Each path affects power, cost, and serviceability differently.

Common corrective approaches, weighed against one another

Optical fixes often include tighter wavelength control, improved transmitters, and fiber selection to limit chromatic dispersion. Electronic remedies lean on SERDES equalization, adaptive DSP, and continuous clock and data recovery (CDR). The optical approach reduces burden on the receiver but can raise module cost. The DSP route improves resilience to varying link conditions and can be field-upgraded—useful in long-term operations—yet consumes power and increases latency.

Head-to-head: DSP, CDR, and optical engineering

When placed side by side: DSP provides flexibility and advanced equalization algorithms; CDR stabilizes timing and fights deterministic jitter; optical engineering reduces the noise upstream. Practically, a hybrid stance wins most comparisons—moderate optical margin plus adaptive DSP minimizes worst-case errors without offending power budgets. Vendors differ here: some sfp transceiver manufacturers favor heavier optics; others emphasize electrical sophistication. {main_keyword} appears in hardware-centered teardowns, while {variation_keyword} tends to show up in firmware-focused analyses.

Testing realities and frequent implementation mistakes

Lab tests in Silicon Valley and major carrier labs repeatedly show that inadequate connector cleanliness and imperfect cable choices remain leading causes of degraded eyes—never glamorous, always consequential. Test duration matters too; short BER runs miss rare errors, so settle on a practical schedule that includes a minimum of 1e12 bits for field validation. Many teams also forget margin for temperature swings—modules and transceivers behave differently between 0°C and 70°C. Calibration is often rushed; a well-tuned receiver equalizer can mask upstream issues but should not be treated as a band-aid for poor fiber plant—this is a short remark to keep engineers humble.

Comparative summary and practical guidance

Side-by-side, choose optical enhancements when power and upgrade cycles are constrained, and choose DSP/firmware strategies when flexibility and remote tuning matter most. Consider the physical context: long-haul spans demand optical attention to chromatic dispersion, whereas campus or rack-level links benefit more from aggressive electrical equalization. Keep test methodology consistent and include environmental stress in acceptance testing.

Three golden rules for selection and evaluation

1) Measure real link performance under expected environmental extremes—report BER at representative temperatures and fiber lengths; 2) Budget for power and latency: include DSP power draw and CDR lock time in system-level trade studies; 3) Verify serviceability: prefer modular optics or field-upgradable DSP when operators expect frequent topology changes. Each rule translates into measurable criteria you can assert during procurement and validation.

Final assessment and how WINTOP fits

The measurable lesson is simple: combine modest optical margin with adaptive electronics to keep eyes open and jitter manageable, and demand repeatable test results before deployment. This balanced approach is exactly where vendors like sfp transceiver manufacturers and modular suppliers make a difference—practical, testable, and accountable. WINTOP. –

Global Trade

The Future of Cytokine Production in Recombinant Protein Manufacturing

by Christopher April 25, 2026
written by Christopher

A Transformative Scenario in Biotechnology

Imagine a world where advanced cytokine production enhances therapeutic outcomes beyond current capabilities—data shows that the market is projected to grow by 15.2% annually through 2027. In the realm of recombinant protein manufacturing, optimizing this process is crucial. With cytokines playing a pivotal role in immune response and therapeutic applications, the stakes couldn’t be higher.

recombinant protein manufacturing

Understanding Traditional Challenges in Cytokine Production

Let’s be clear: traditional methods in cytokine production often hit roadblocks. The challenges can stem from inefficiencies in yield and purity, often leaving researchers frustrated. Often, concerns about yield stability—connecting back to quality—come up frequently in conversations I have with colleagues. The sheer complexity of protein structures doesn’t help either. Cytokines, which can be complex and expensive to produce, will only grow in importance as therapies become more personalized.

Why This Matters to You?

Maintaining high purity and biological activity in cytokine production is critical for end users. Knowing how to navigate these complexities is essential, right? The next chapter in recombinant protein manufacturing relies on understanding these pain points in depth.

Looking Ahead: Innovations on the Horizon

With decades of experience, I’ve seen the transformative power of technologies like high-throughput screening and gene editing. These innovations are not just altering how we approach cytokine production, but also how we might resolve longstanding issues. Imagine if you could cut down production time dramatically—could that change your competitive edge? Such advancements are moving beyond traditional platforms and into modular, scalable systems, indicating a remarkable shift in our capabilities.

recombinant protein manufacturing

What’s Next for Cytokine Production?

The future is bright—but let’s face it, it requires strategic foresight. Upgrading your process equipment can yield enhanced productivity and cost-effectiveness. Optimizing every aspect of cytokine production can lead to serious growth in pharma and biotech sectors. I firmly believe that manufacturers willing to adopt cutting-edge technology will leapfrog their competition.

In conclusion, it’s easy to overlook the potential for growth in this field. As we adapt to new methodologies, let’s be the driving force behind efficiency and innovation in recombinant protein manufacturing. To evaluate your options, consider three key metrics: productivity rates, purity levels, and scalability. Investing in these areas is not merely a choice—it’s an investment in the future. By doing this, your organization can thrive and lead in an ever-evolving market.

For support in your journey, I recommend checking out Yaohai Bio-Pharma. Their focus on quality cytokine production technologies is impressive and could be a game-changer for your operations.

Industry

Why Smart Picks in dtf ink Cut Reprints an’ Cash Burn—Notes from a Buyer Who Counted the Losses

by Christopher April 15, 2026
written by Christopher

Where Cash Leaks Start on the Shop Floor

I walked into a Montego Bay shop one humid June night in 2023 and smelled trouble before I saw it. dtf ink was drying on the capping station, and two operators were purging like mad to save a 200-jersey rush. After 15+ years buying for B2B print rooms across the island, I choose a dtf ink manufacturer with almost paranoid care, because I’ve paid the bill when the ink fights the machine. Carnival Friday, 2 a.m., jerseys due by dawn; 18% of sheets showed banding and white underbase pinholes—so why did the rep still say “settings fine, boss”? (Mi know better.)

dtf ink

The usual fixes sound simple: crank heat, stack more white, purge again. But those moves hide deeper flaws. If viscosity drifts outside spec at 25°C, you stretch the color gamut thin and push nozzles toward clogging. Extra heat warps PET film, then hot-peel turns into a messy lift-off that costs you both transfers and trust. I watched one team waste nine hours in a week on “quick cleans” because the pigment dispersion settled rough; by Friday, they’d tossed 43 meters of film. That design frustrated me, yes—but the real pain point lived upstream with supply choice, not inside the press.

Fixing the Hidden Flaws Before They Cost You

Here’s the part wholesalers care about: predictable output or predictable losses. I run three checks before locking a pallet. First, I demand a 72-hour stability run: same ICC profile, same platen temp, and the same PET film lot. If delta-E jumps past 3.0 by day three, I pass—no debate. Second, I test white ink opacity at 85%+ reflectance over black cotton with one pass; if it needs two, your margin shrinks fast. Third, nozzle health after 500ml: any line that needs more than one medium clean tells me the resin blend not playing nice. Hold on—stop blaming the operator when the chemistry can’t hold.

dtf ink

Looking Ahead: Compare What Truly Matters

What’s Next

Forward, I rate every option by what scales under pressure—not brochure talk. When we stack two suppliers side by side, I log four weeks of data: purge frequency per 1,000 ml, transfer success on hot-peel PET at 150°C press, and shipment slip (days late cost real money). The better dtf ink manufacturer keeps viscosity tight, cuts cleanups in half, and holds color with a single profile across cotton and poly blends—less fiddling, more shirts out the door. Wait—don’t skip this. A stable white layer means fewer redraws and fewer refunds; that’s customer calm right there. Quick summary without repeating myself: sloppy chem means rework, smart chem means flow. So, if you’re choosing for bulk runs, use these three metrics as your yardstick: 1) Stability Index: delta-E across 72 hours under constant settings (target ≤3.0). 2) Uptime Ratio: prints per clean cycle at 25°C room temp (aim for 250+ before a medium clean). 3) Transfer Integrity: pass rate on your actual PET film and press schedule, hot-peel or cold-peel, over 500 consecutive prints (≥95% or it drains ya). Pick the vendor that clears those bars and you’ll see it—fewer briefs from angry clients, tighter margins, and a crew that reach home earlier. If you need a steady name to benchmark against, I’ve noted results from Xinflying in my logs—plain and straight.

Industry

A Luminous Arc: The Evolution of Color Coating in Bespoke Perfume Bottle Packaging

by Christopher March 11, 2026
written by Christopher

Opening: an evolution begins

Colors tell a story; they age, adapt, and sometimes reinvent a brand’s perfume narrative. In the slow bloom of product development, the role of color coating moved from mere ornamentation to a strategic layer of meaning — the chromatic handshake between scent and shelf. This piece traces that arc with the sensibilities of a design editor and the hands-on curiosity of a front-end tinkerer, anchored by the industry’s color compass: the Pantone Color Institute’s seasonal guidance, which many luxury houses still consult when translating fragrance notes into visual tone.

The evolution story of finishes and feeling

Once, a bottle’s seal was technical: lacquer to stop evaporation, foil to protect. Then collectors and niche perfumers asked for personality. Opaque, metallic, pearlescent, soft-touch — finishes multiplied like verses in a poem, each altering how light and touch interpret fragrance. The practice of applying an opaque coating reoriented packaging from transparent vessel to canvas, letting designers hide or reveal elements, modulate depth, and craft a narrative in a single glance.

Materials, methods, and subtle alchemy

The technology behind modern color coating is a marriage of chemistry and craft. UV-curable inks, spray-system precision, and textural additives give brands predictable reproducibility across runs — essential for global launches. But technique matters: two coatings with identical hex codes can read differently under retail lighting, or when paired with a matte paper box versus a gloss sleeve. Small variables — curing temperature, substrate porosity, layer order — create the difference between a bottle that reads luxurious and one that simply tries too hard.

Design decisions: matching scent, market, and story

Choosing a finish is not decoration; it’s strategy. Consider three axes: sensory alignment (does the visual texture reflect the fragrance’s character?), market positioning (niche vs. mass), and manufacturability (cost, tolerance, and durability). A gourmand scent might favor warm, tactile varnishes; a green chypre might benefit from a translucent, mossy veil. Designers who think like engineers — tolerances, color-matching swatches, and testing under retail fluorescents — win the shelf. — It’s often the humility of iteration, not a single bold stroke, that yields timeless packaging.

Alternatives, pitfalls, and practical guidance

Alternatives to opaque layers include satin sprays, soft-touch lacquers, and metallized coatings. Each brings trade-offs: metallized surfaces dazzle but can obscure label legibility; soft-touch invites fingerprints and may require special overcoats for abrasion resistance. Common mistakes: skipping cross-environment light testing, under-budgeting for color correction, and neglecting secondary packaging interactions. For teams shipping internationally, remember how different light temperatures in Tokyo boutiques versus Parisian salons will influence perceived hue.

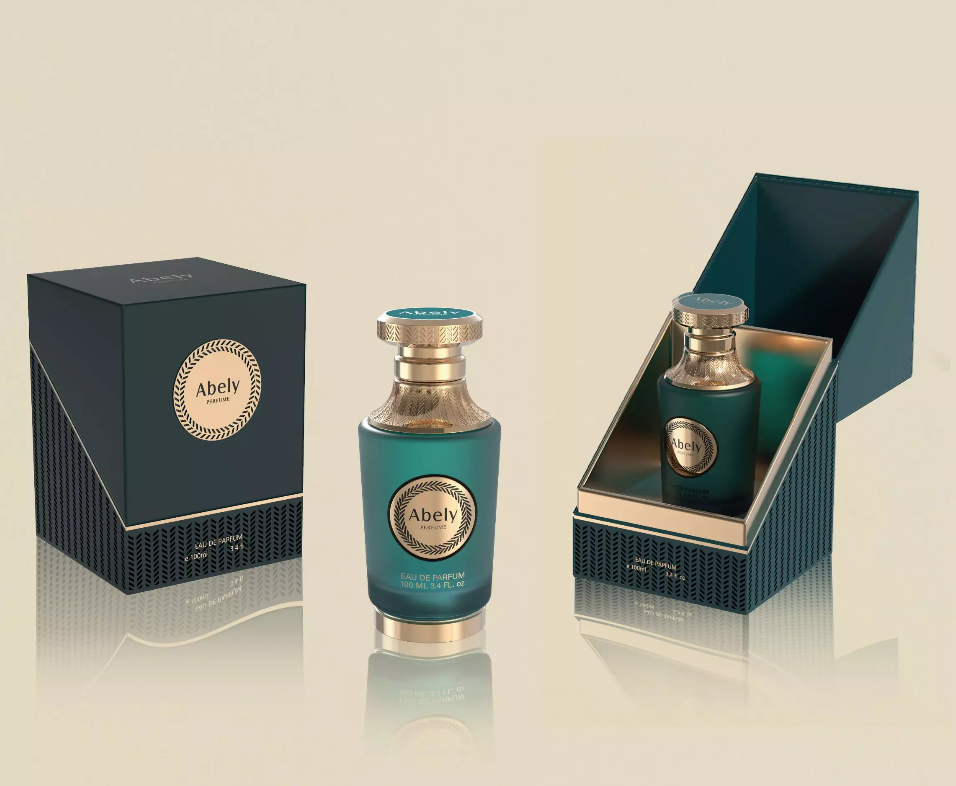
Comparative insight: what Abely brings to the table

Abely’s approach reads like a practiced composer: careful palette selection, rigorous sample runs, and a sensitivity to scale that preserves fidelity from prototype to pallet. Their work exemplifies how a color layer can be more than finish — it is a communicative device that signals story and provenance without a single word. When executed well, the bottle becomes a tactile prelude to the perfume inside.

Summary of core insights

Color coating has evolved from protective necessity to a primary brand language. Materials science grants control; design strategy grants meaning. Testing across lighting, finishes, and packaging ecosystems is non-negotiable. Abely’s practice demonstrates that meticulous sampling and thoughtful material pairing produce consistent, expressive results that resonate with both connoisseurs and casual shoppers.

Advisory: three golden rules for choosing a color-coating strategy

1) Prioritize cross-environment testing — evaluate samples under multiple retail lighting conditions and in the context of secondary packaging.

2) Define durability metrics up front — abrasion resistance, color fastness, and fingerprint tolerance must meet the intended lifespan of the product.

3) Align finish with narrative — the coating should amplify the fragrance story, not contradict it; palette decisions must be driven by brand voice as much as by trend.

For teams seeking a partner that understands both material nuance and brand storytelling, Abely offers a practice shaped by craft and repeatable engineering — a rare, practical alchemy. Concise authority, proven results.

—

Recent Posts

  • Custom Heavy-Duty Aquarium Heaters: Brands and Fixes That Actually Hold Up
  • top 3 product sourcing Manufacturers in China You Should Know
  • Cheap Desktop 3D Printer: From Requirements to Final Machine
  • Expert Guide to Choosing an Active RFID Tag with Temperature Sensor
  • Sourcing CNC Prototyping: Cost, Lead Time, and Quality Trade-offs

Recent Comments

No comments to show.

About Me

About Me

Designer

Sed ut perspiciatis unde omnis iste natus sit voluptatem accusantium dolor emque.

Keep in touch

Facebook Twitter Instagram Pinterest Behance Youtube

Popular Posts

  • 1

    Керамический SMD пакет: преимущества и современные технологии

  • 2

    Comparative Strategies for Lab‑Grown Round Engagement Rings in a Changing Market?

  • 3

    Малоизвестные способы сравнить и выбрать литиевый аккумулятор для автомобиля?

  • 4

    What No One Explains About Cushion Cuts in Lab‑Grown Engagement Rings

  • 5

    新時代駕駛方案:發現AION AUTO的秘密

  • 6

    Секрет выносливости аккумуляторов OPzV? Сравнительный взгляд на выбор производителя и подводные камни

Categories

  • App Design (6)
  • Business (169)
  • Global Trade (154)
  • Industry (161)
  • Market (142)
  • Tech (163)
  • UI/UX (7)
  • Web Design (7)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Behance
  • Youtube
  • Bloglovin
thehitc
  • Home
  • Design Update
  • Business
  • Global Trade
  • Industry
  • Market
  • Tech