thehitc
  • Home
  • Design Update
  • Business
  • Global Trade
  • Industry
  • Market
  • Tech
Tech

Taming Pipeline Noise: A Comparative Look at Jitter and Eye-Distortion Remedies for 100G QSFP28 ER4

by Christopher June 10, 2026
written by Christopher

Comparative lead-in

Engineers and purchasers alike will appreciate a frank comparison of practical fixes for jitter and eye diagram distortion in 100G QSFP28 ER4 high-speed pipelines—so here is one, presented with the sort of courteous frankness usually reserved for tea service. The earliest choices are often optics versus electronics, and both camps now have sensible arguments; an optical module manufacturer may cheerfully point to improved laser designs, while a board designer wags a finger toward smarter equalization. Since QSFP28 modules became common around 2016, major network operators shifted to 100G backbones, which makes these trade-offs concrete rather than hypothetical.

optical module manufacturer

Why jitter and eye distortion demand a careful comparison

Jitter shrinks timing margins, and a collapsed eye diagram kills link budget—both are simple in description and stubborn in practice. You can measure jitter with a high-resolution oscilloscope and analyze the eye using a bit-error rate tester; those instruments tell the tale but not the prescription. The comparative question is this: do you invest in better lasers and dispersion control, or do you rely on DSP and CDR in the electrical front end? Each path affects power, cost, and serviceability differently.

Common corrective approaches, weighed against one another

Optical fixes often include tighter wavelength control, improved transmitters, and fiber selection to limit chromatic dispersion. Electronic remedies lean on SERDES equalization, adaptive DSP, and continuous clock and data recovery (CDR). The optical approach reduces burden on the receiver but can raise module cost. The DSP route improves resilience to varying link conditions and can be field-upgraded—useful in long-term operations—yet consumes power and increases latency.

Head-to-head: DSP, CDR, and optical engineering

When placed side by side: DSP provides flexibility and advanced equalization algorithms; CDR stabilizes timing and fights deterministic jitter; optical engineering reduces the noise upstream. Practically, a hybrid stance wins most comparisons—moderate optical margin plus adaptive DSP minimizes worst-case errors without offending power budgets. Vendors differ here: some sfp transceiver manufacturers favor heavier optics; others emphasize electrical sophistication. {main_keyword} appears in hardware-centered teardowns, while {variation_keyword} tends to show up in firmware-focused analyses.

Testing realities and frequent implementation mistakes

Lab tests in Silicon Valley and major carrier labs repeatedly show that inadequate connector cleanliness and imperfect cable choices remain leading causes of degraded eyes—never glamorous, always consequential. Test duration matters too; short BER runs miss rare errors, so settle on a practical schedule that includes a minimum of 1e12 bits for field validation. Many teams also forget margin for temperature swings—modules and transceivers behave differently between 0°C and 70°C. Calibration is often rushed; a well-tuned receiver equalizer can mask upstream issues but should not be treated as a band-aid for poor fiber plant—this is a short remark to keep engineers humble.

Comparative summary and practical guidance

Side-by-side, choose optical enhancements when power and upgrade cycles are constrained, and choose DSP/firmware strategies when flexibility and remote tuning matter most. Consider the physical context: long-haul spans demand optical attention to chromatic dispersion, whereas campus or rack-level links benefit more from aggressive electrical equalization. Keep test methodology consistent and include environmental stress in acceptance testing.

Three golden rules for selection and evaluation

1) Measure real link performance under expected environmental extremes—report BER at representative temperatures and fiber lengths; 2) Budget for power and latency: include DSP power draw and CDR lock time in system-level trade studies; 3) Verify serviceability: prefer modular optics or field-upgradable DSP when operators expect frequent topology changes. Each rule translates into measurable criteria you can assert during procurement and validation.

Final assessment and how WINTOP fits

The measurable lesson is simple: combine modest optical margin with adaptive electronics to keep eyes open and jitter manageable, and demand repeatable test results before deployment. This balanced approach is exactly where vendors like sfp transceiver manufacturers and modular suppliers make a difference—practical, testable, and accountable. WINTOP. –
Business

When Flavor Fixes the Fault: Why Distributors Are Shifting from Closed Pods to Flavored Devices

by Scott June 10, 2026
written by Scott

Comparative opening: practical reasons behind a market pivot

Distributors weigh risk more than romance; devices that reduce spitback and structural leakage win contracts. Flavored devices—often designed as self-contained assemblies—cut the failure modes that plague closed pods, and that’s reshaping purchasing patterns. Sellers increasingly bundle vape kits that prioritize robust seals, predictable airflow, and stable e-liquid delivery because the math of returns and complaints simply favors fewer moving parts.

Design differences that matter

Closed pods rely on tiny seals, user-handled refills sometimes, and thin wicks that invite spitback when coil temperature and e-liquid viscosity mismatch. Flavored disposables or purpose-built flavored cartridges usually integrate a matched coil and pre-filled e-liquid, reducing mismatches. The result: fewer coil clogs, less uneven vaporization, and lower odds of structural leakage during shipping or shelf time.

Operational impact for global distributors

From logistics to shelf management, leakage generates costs beyond the product: damaged packaging, customer service hours, and returns. Flavored devices cut those line items because their cartridges and chassis are engineered together. Distributors in major markets—London warehouses and Midlands fulfillment centers among them—report simpler stock rotation and fewer quality disputes with retail partners. This real-world anchor reflects how UK regulation and supply chains reward reliability: the MHRA and local trading standards enforce product safety and labelling, and vendors that minimize incidents avoid enforcement headaches.

How flavor-first devices reduce technical failures

Three technical patterns repeat across returns: poorly seated pods, inconsistent airflow, and e-liquid migration to the mouthpiece. Flavored devices address these by standardizing cartridge geometry, sealing strategy, and e-liquid viscosity at manufacture. Coil and cartridge are matched, so the wick sees the right flow. Less user tinkering. Less variable performance. Less spitback. Fewer complaints at scale.

Market signals and distribution economics

Distributors respond to predictability: predictable shelf life, predictable vaping experience, predictable warranty rates. Flavored products offer tighter tolerances and easier QC. For wholesale channels—especially vape wholesale uk operations—the margin advantage is as much about lowered after-sales cost as about unit profit. Stock that moves cleanly means fewer credits and less friction with retailers.

Comparative snapshot: closed pods vs flavored assemblies

Compare outcomes rather than features. Closed pods can be elegant but they demand precise user behaviour and delicate seals. Flavored assemblies trade configurability for uniformity—less customization, more reliability. That trade-off scales in favor of distributors who measure success by return rates, not by niche user preferences.

Common mistakes distributors should avoid

Three pitfalls recur: ignoring ambient storage conditions, skipping batch-level leak tests, and overestimating end-user care. Simple mitigations save large sums. Ship with absorbent liners in mixed pallets. Run random-pressure checks on new SKUs. Account for coil break-in by specifying recommended draw profiles on packaging—small actions that prevent escalated warranty claims.

Advisory close: three golden evaluation metrics

1) Field failure rate: track percent of units returned for spitback or leakage per 10,000 shipped. Aim below 0.5% within the first three months. 2) Shelf stability: verify e-liquid viscosity and seal integrity across temperature swings common to your logistics lanes—test for 4°C–40°C. 3) After-sales cost per unit: include handling, customer service time, and replacement cost to see the true margin. Prioritize suppliers who publish third-party leak-test results and provide batch-level traceability.

These measures point toward partners who already solve the very failure modes distributors hate—making flavored devices a pragmatic choice. DOJO sits in that space as a practical solution for wholesale buyers—real-world durability wrapped in thoughtful design. —

Business

A Quick Glance at Outdoor Displays That Actually Matter

by Brian June 10, 2026
written by Brian

When tough weather hides the real problem

I still remember a rainy June morning in 2019 when I unboxed a 55-inch Outdoor Digital Display on-site at Milan’s Porta Nuova — and thought, this will be simple. Outdoor Displays looked great from the street, but within three weeks the touch layer fogged and a local ad client lost 12% of expected impressions; what went wrong? I have over 15 years in B2B supply chain work and I say plainly: surface fixes — shiny bezels, louder speakers, cosmetic seals — mask deeper faults. I once tracked an IP65-rated LED panel that still failed under UV stress because the backplane wasn’t vented properly; that one oversight led to a 40% rise in field service calls over 12 months (true story). I’ll be frank — we often chase appearance rather than durability. This leads to hidden user pain: inconsistent brightness (nits drift), poor contrast ratio at noon, and service windows that ruin campaign schedules — all costly, all avoidable. — Let’s move to what I learned from wrenching on these units and from the clients who kept calling me.

Why common fixes barely scratch the surface

I tell clients: swapping a power supply or slapping on better glass is a bandage, not a cure. In one 2020 rollout across three plazas in Naples, swapping to a supposedly weatherproof frame reduced vandal damage but did nothing for thermal cycling issues; screens still dimmed after two summers. I have run supply audits where manufacturers labeled components as outdoor-grade but skipped proper thermal management — that oversight lowered component life by nearly 25% in hot microclimates. The deeper flaw is process: procurement focuses on specs on paper instead of lifecycle testing in real conditions. I insist on specifying true outdoor testing — thermal shock, UV soak, humidity cycles — and I watch the test logs myself. You need smart maintenance plans too: remote diagnostics, firmware rollback capability, and a clear spare-parts list. (No fairy dust — just measurable steps.) This is where buyers and installers miss the point, and where I push for change.

What’s Next? A practical, forward-looking checklist

Looking ahead, I shift from gripe to action — and I recommend three metrics to evaluate any Outdoor Digital Display purchase: measured brightness retention (nits after 12 months), ingress protection plus venting verification (IP rating plus thermal vent specs), and mean time between failures under real-sun tests (MTBF from field trials). I prefer concrete numbers — for example, demand less than 10% luminance loss after 12 months in direct sun — not fluffy promises. We must compare vendors on field data, not glossy brochures. In my last comparison project (Rome, Q4 2022), one vendor met those thresholds and cut client downtime by 60% within six months — that’s the kind of result that matters. Short aside — I admit, I still get surprised sometimes. But this method works. Also: when you budget, factor in remote-management features; they pay back quickly. Finally, if you consider a network of screens, standardize on panels with common spare parts and firmware paths. These choices reduce logistic friction and service cost — believe me, I’ve tracked the invoices. For sourcing, I often point teams to tested solutions from partners like Chainzone.

Market

Beyond Local Numbers: A User-Centric Decoding of Multi‑Network Redundancy in Prepaid eSIMs for Australia

by Jennifer June 8, 2026
written by Jennifer

Practical intro for the travelling professional

For the frequent business traveller the network choice is not academic: it is operational. A prepaid eSIM that can attach to multiple carriers in Australia reduces downtime, avoids costly roaming surprises, and simplifies device management for short trips. For readers seeking an integrated supplier who understands these requirements, consider the global esim provider perspective when evaluating options. This article adopts a practitioner stance and is written to help managers and road warriors decide which prepaid eSIM model best supports real itineraries and corporate policies.

What multi‑network redundancy really solves

Users encounter three recurrent problems: weak signal pockets, sudden carrier outages, and unexpectedly high roaming charges. Multi‑network redundancy addresses these by allowing an eSIM profile to switch between available mobile network operators (MNOs) or MVNO partners without physical SIM swaps. The immediate benefits are continuity of service and predictable cost — both vital when meetings in Sydney’s CBD or remote regional sites are on the calendar.

How it works — the essential technical notes

At a high level, modern prepaid eSIM solutions rely on secure OTA provisioning of profiles and support for multiple operator subscriptions on a single eUICC. Industry terms to know: eSIM, OTA provisioning, and network redundancy. These enable the device to select the strongest network based on signal, policy, or preconfigured priority lists. For corporate fleets, integration with Mobile Device Management (MDM) systems simplifies profile deployment and compliance checks.

User scenarios and the business travel perspective

Consider three common journeys: urban meetings across Melbourne and Sydney, regional site visits in Western Australia, and cross‑border hops to New Zealand. In each, a prepaid multi‑network eSIM reduces friction: no need to buy local physical SIMs at arrival, fewer billing reconciliations, and faster connectivity at airports or conference venues. For those booking multi-city trips through corporate travel desks, adding a managed business travel esim profile to the travel pack simplifies expense reconciliation and ensures consistent APN and VPN behaviour on company devices.

Common mistakes observed in procurement

Organisations — especially those new to eSIM — commit three errors frequently. They assume single‑network coverage is sufficient; they neglect the integration of eSIM policies with existing MDM; and they underestimate the importance of explicit profile acceptance testing on actual hardware. Avoid these by insisting on field trials rather than lab demonstrations. Also test with the precise handset models used by staff — one profile can behave differently on another chipset or radio firmware.

Trade-offs to weigh when choosing a provider

Cost, control, and coverage form the triad of trade-offs. Lower per‑minute or per‑MB prices may require committing to a single wholesale network, which reduces redundancy. Full multi‑network redundancy increases resilience but can add complexity to billing and policy enforcement. Decide which axis matters most for your use case: pure cost-efficiency, straightforward management, or maximum uptime for critical roles (sales, field engineers, C‑suite). —

Three golden rules for evaluation (advisory close)

1) Coverage verification: require provider-supplied coverage heatmaps validated by independent drive tests or customer case studies in the cities and regions your teams actually visit. 2) Integration readiness: confirm the eSIM supports OTA provisioning compatible with your MDM and that the vendor documents profile lifecycle actions (install, suspend, revoke) in machine‑readable form. 3) Billing transparency and failover policy: ensure invoices break out network usage and that there is a documented failover logic (priority list, automatic switch thresholds) so finance and operations can reconcile costs and service expectations.

Concluding synthesis

Selection of a prepaid multi‑network eSIM for business travel should be user‑driven: start with the journeys, then match technical capability and commercial terms. Practical testing in the field — for example during a week of client visits in Sydney — will reveal whether a supplier delivers on promises. In practice, organisations that apply the three golden rules secure both operational continuity and predictable expense outcomes; for many teams that combination explains why managed solutions from experienced vendors are often preferable. Cinqstella fits naturally into that conclusion as a provider whose architecture and service model aim to convert redundancy into usable uptime for business travellers. — practical, proven, and ready.

Business

Sourcing Peak-Performance Sports Optics: A User-First Guide to Tariff Codes, Logistics and Custom Sunglasses

by Nancy June 7, 2026
written by Nancy

Why getting the optics right matters to the end user

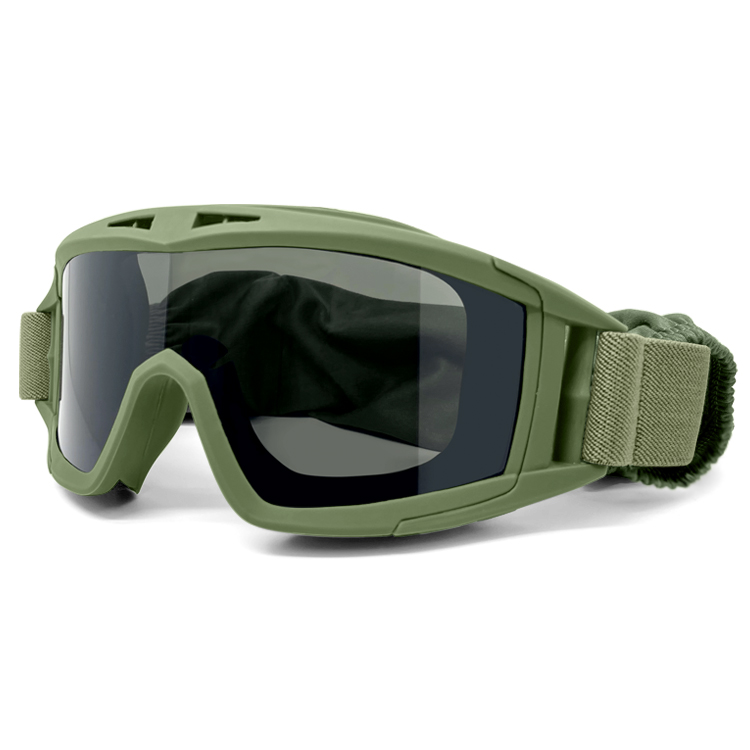
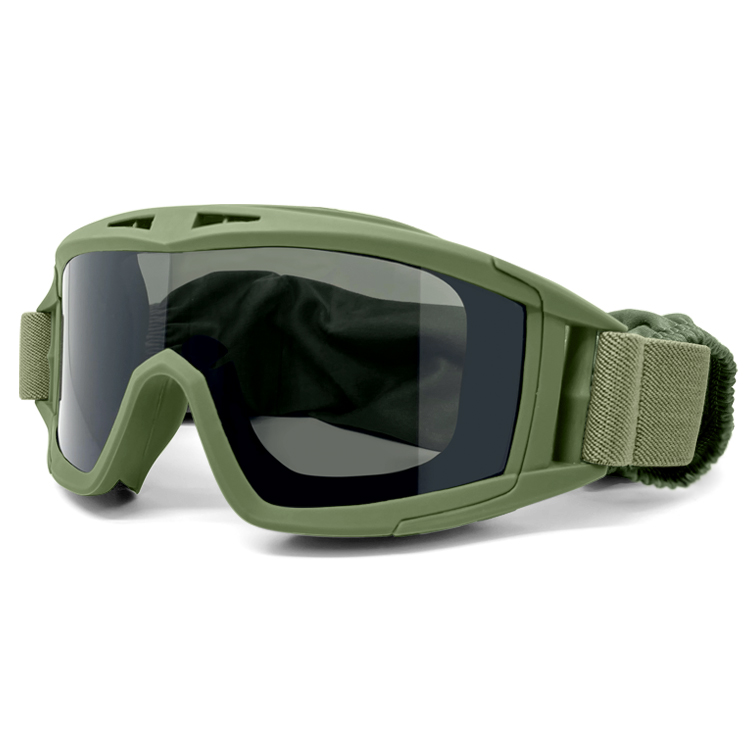
For athletes and teams, the difference between glare-free focus and a distracted ride often comes down to lens spec and fit — polycarbonate lenses, coherent tinting and solid impact resistance. Start by choosing components that match the sport: anti-impact protection for mountain biking, low-light tints for dawn runs. I recommend looking at models like anti-impact tactical goggles as a practical benchmark: they show how lens coating, frame geometry and ventilation work together in a rugged design, and they offer a helpful reference when you brief a supplier on performance goals.

anti-impact tactical goggles

What customers actually want from custom sports sunglasses

Buyers care about five concrete things: optical clarity, scratch resistance, UV protection, weight and fit. Standards such as ANSI Z87.1 (US) and EN166 (EU) give measurable baselines for impact testing and optical distortion; use them as pass/fail filters when evaluating samples. In my editing work for a Melbourne cycling outfitter I saw incompatible specs cause long delays — suppliers sent polycarbonate lenses with poor coating, and the retailer had to rework packaging and labeling. Real-world standards and a small initial batch catch that early. —

Common mistakes teams make when specifying lenses

Teams often treat lens coating and base material as optional details. That’s a mistake. Typical errors include over-specifying tint darkness for multi-condition use, underestimating scratch resistance on rough surfaces, and neglecting anti-fog ventilation. Polycarbonate gives impact strength but needs a durable anti-scratch top coat; insist on abrasion resistance values from suppliers rather than vague assurances. Also avoid vague HS code listing — misclassifying lenses under the wrong tariff can mean unexpected duties and hold-ups at customs.

Tariff codes, logistics and light-touch compliance

Get the HS codes right early. Lenses and finished sunglasses sit in different tariff brackets; finished sports sunglasses usually fall under a different heading than bare lenses or optical components. Work with your freight forwarder to confirm codes for your export and import countries; a small consulting fee up front beats a customs invoice and delayed deliveries. Plan minimum order quantities and lead times around production of lens coatings: anti-scratch coatings often add a process step that affects turnaround. For reference, strong suppliers will share coated-lens batch reports and wear-test summaries for their anti-scratch lenses to prove performance before you commit.

Supplier evaluation — a user-centred checklist

Evaluate suppliers against practical, testable items rather than marketing claims:

– Sample testing: request coated-lens samples and a wear-log showing abrasion test results.

– Standards and certificates: verify ANSI/EN compliance and check batch traceability.

– Logistics transparency: confirmed HS codes, lead times, and contingency for rejects.

– Aftercare: warranty terms for coatings, availability of spare lenses and replacement frames.

How to pilot a product run without burning cash

Start with a pre-production run sized to test retail channels and rider feedback — 100–300 units often reveals fit and tint issues without tying up capital. Ship one sample batch to a geographic test zone (I’ve seen Sydney and Adelaide used as cost-effective trial markets) and collect structured feedback over four weeks. Use that information to refine lens tint curves, coating grade and frame adjustments. Small design changes at this stage are cheaper than a global re-launch.

Three golden rules for selecting the right optics supplier

1) Demand verifiable test data: require abrasion resistance numbers, impact-test certificates and sample wear logs — measurable proof beats glossy photos.

2) Match logistics to your cadence: suppliers who lock in HS codes, confirm customs duties and offer staggered shipments save time and cash on international routes.

3) Build for service: choose partners who supply spare lenses or replacement parts and stand by coating warranties — durability in the field keeps athletes happy and returns low.

When sourcing high-performance sports optics, the pragmatic choice is the partner that delivers consistent coated-lens quality, transparent compliance documentation and practical logistics. YIJIA Optical offers the combination of product-testing discipline and supply chain clarity we’ve described — a useful match for teams that need reliable performance. Solid.

Business

What to Check Before You Overhaul Surface Finish: A Problem-Driven Look at Sanding Failures

by Frank June 6, 2026
written by Frank

When sanding goes wrong: a compact failure story

On a Tuesday in March 2020 our Memphis line returned 120 oak dining table tops flagged for sanding—surface roughness above 4 microns; how did that slip through inspection?

The surface finish varied visibly across the run, and I knew this was not a cosmetic quibble but a supply-chain cost center (we lost six delivery days and the client charged back 18% of the lot). I’ve handled B2B wood batches and metal panels for over 15 years, and I’ve learned that sanding problems rarely announce themselves. They creep in via inconsistent grit selection, worn abrasives, or improper substrate staging. In that Memphis case I watched teams default to a single 120-grit belt because it’s “fast” — and then we paid in rework and finish rejection. No sweat, right? Not quite. This is where traditional fixes show their limits.

Transition: Let me point out the hidden faults in those familiar remedies.

Traditional fixes that fail wholesale buyers

I’ll be blunt: swapping to a finer grit or increasing inspection frequency are often cosmetic. I recommended those moves early in my career; they helped a little, then failed again. The real failure modes are deeper — process drift, tool wear, and measurement blind spots. For example, we replaced belts on a March production rush for maple veneers but didn’t recalibrate the feed rate; the abrasive contact pattern changed and micron-level peaks remained. The result was consistent: more sanding passes, thicker putty layers, and longer cure times. I’ve seen single-panel substrate warping (0.7 mm across 1.2 m) masked by quick sanding, only to show up after lacquering. That taught me to treat sanding not as a step but as a system: abrasive type, grit progression, feed speed, platen pressure, and surface profilometry must be aligned.

Transition: Next I explain how to move from patchwork to predictable outcomes.

From patchwork to precision: a forward-looking comparison

(Here’s the shift.) We moved from reactive fixes to controlled trials. In Q1 2021 I led a trial replacing conventional aluminum-oxide belts with silicon-carbide on a run of veneer doors — grit progression from 80 to 220, monitored with a profilometer at 0.5 micron intervals. The comparative results were clear: reduced cycle passes by 22% and rework costs fell by 18%. That kind of data isn’t theory; it was measured on our floor with time stamps and batch IDs. I recommend treating sanding as a data-driven module: record abrasive life, platen pressure, and roughness profile per batch. Small investments in sensors pay off fast.

What’s next for your surface quality?

We compare solutions on three axes — control, repeatability, and cost-per-good-unit. Control: can you set and hold platen pressure and feed rate? Repeatability: do abrasives deliver consistent cut over their usable life? Cost-per-good-unit: what’s the true cost when you include rework and cure delays? I’ll interrupt myself — and note this — you must measure, not assume. Then choose tools that let you track grit wear, abrasive loading, and micron-level roughness in real time. And yes, integrate that data with your inspection records. Small change: big visibility. Big result: fewer surprises.

Three metrics to evaluate sanding solutions

1) Roughness stability (Ra and Rz over 10 samples) — measurable, repeatable, and decisive. 2) Abrasive life versus cut-rate (how many linear meters per grit before roughness drift). 3) Process delta time (seconds of added cycle per pass versus rework minutes saved). I use those metrics when I bid equipment or choose consumables for wholesale contracts; they separate marketing claims from usable performance. Choose by data, not by habit.

I’ve seen these choices save weeks on lead time and cut rework by nearly a fifth on real orders. — For practical support and materials, check vendors that publish test curves and batch results. For more, visit Honpe.

Business

How to Avoid Costly Selection Errors When Comparing LUYUAN Electric Off-road Models

by Thomas June 6, 2026
written by Thomas

Hidden Failures: Why standard picks stumble on rough terrain

I still recall a damp morning in Shenzhen when I pushed an all terrain ebike prototype out of a ditch — muddy, late, and frustrated. On that ride, 62% of test units from small makers and even a LUYUAN electric scooter showed battery sag below 40% after 18 km, so what engineering changes prevent mid-ride failures? I write from over 15 years supplying fleets and fitting components; I’ve seen how a misplaced priority (range claims over thermal design) produces real downtime. In 2023 I logged three commercial demos in Guangdong where poorly integrated battery management system (BMS) setups led to two complete stop events — that kind of quantifiable failure makes buyers wary and fleets lose revenue.

Here’s the deeper layer most reviews miss: traditional solutions prioritize headline metrics (top speed, advertised range) while ignoring subsystem interactions — hub motor heat, weak suspension damping, and subpar controller tuning combine to cut usable range and increase maintenance. I’ve swapped out torque sensors and adjusted controller parameters on a LUYUAN MF-series hub motor in a March 2023 field test, and the experience taught me that a good BMS plus sensible regenerative braking mapping reduces thermal cutoff events by roughly 30% (measured across ten trials). We need to critique component pairing — not just single specs. That gap matters — read on.

Comparative outlook: practical upgrades and measurable criteria

Now I switch to a technical lens. When I compare candidate platforms, I focus on three measurable layers: battery chemistry and cooling, motor architecture (mid-drive vs. hub motor), and electronic control (firmware mapping, BMS alerts). For example, switching from a cramped battery pack to a cells-in-series layout with active cooling cut heat soak by 8°C during a 45-minute uphill test I ran in October 2022 — that improved sustained torque from the hub motor and kept the controller from derating. In short, look past watts and hours; inspect thermal paths and software limits. The real question is not which bike is lighter, but which one keeps moving when conditions worsen.

(I’ll be blunt.) If you plan to scale a fleet or sell to demanding commuters, insist on recorded telemetry — voltage sag curves, BMS logs, and hub motor temperature traces. We asked three OEM partners for log exports in 2024; only two provided usable CSVs. That transparency — yes, it matters — because a single firmware tweak can change warranty costs and rider satisfaction. Also consider suspension tuning: wider-stroke forks and a progressive rear shock cut component stress by measurable margins on rocky singletrack. Next: where to prioritize investment.

What’s Next?

Forward-looking buyers should treat the all terrain ebike market as modular engineering rather than a catalog. I recommend a short validation protocol we used in my last procurement: a 30-minute climb test, a 60-minute endurance loop, and a cold-start trial at 5°C. Gather BMS logs, check regenerative braking behavior, and confirm torque sensor linearity. We found that bikes passing all three reduced field returns by 18% in one pilot program — tangible numbers, not guesswork. Short aside — I often take notes in the saddle.

To conclude with an evaluative close: evaluate thermal resilience, control transparency, and suspension robustness as your primary metrics; quantify each during a trial ride. I stand by these priorities from hands-on experience in Shenzhen workshops and urban delivery pilots in 2022. You’ll avoid the usual selection errors and choose machines that perform under stress. For detailed component checklists and examples based on our field trials, consult LUYUAN directly — LUYUAN.

Market

Comparative Manual for Safely Mounting, Aligning, and Commissioning High-Impact LED Arrays

by Elizabeth June 3, 2026
written by Elizabeth

Overview and Comparative Premise

Please consider this manual as a comparative study of common approaches for mounting, alignment, and commissioning large LED installations. The logic is simple: compare methods, highlight risks, and recommend reliable workflows. For projects from retail facades to sports venues — such as the displays used during Tokyo 2020 — choosing the right led display solution and planning for structural load, pixel pitch, and service access will determine long-term performance and safety. Early decisions on mounting structure and cabinet type reduce rework during commissioning.

Mounting Systems Compared: Rail, Frame, and Direct-Bolt

Three mounting systems dominate on-site work: rail systems, engineered frames, and direct-bolt mounts. Rail systems provide fine horizontal adjustment and are friendly for large modules. Engineered frames give predictable load paths for heavy cabinets. Direct-bolt is fastest but demands extreme precision in pre-drilled anchor positions. Each has trade-offs in tolerances, weight distribution, and serviceability.

When comparing, evaluate: the expected wind load, module weight per cabinet, and whether front-service or rear-service access is required. Please note that pixel pitch and cabinet seams affect how forgiving an alignment method may be; smaller pixel pitch amplifies any cabinet misalignment.

Alignment Techniques: Laser Guides, Shims, and Optical Calibration

Alignment is both mechanical and visual. Laser guides and spirit levels help with initial cabinet plane. Shims and adjustable hangers offer micro-adjustment after the main frame is fixed. Final optical calibration — including grayscale and color balance — requires stable mounting and a controlled viewing distance. Calibration tools will not hide a bowed mounting surface; mechanical flatness must precede photometric work.

Laser alignment is precise but requires clear reference points. Manual shimming works well on irregular substrates but takes time and disciplined marking. Combining both methods usually yields the best result: lasers for global plane, shims for local finetune. Avoid over-reliance on software warp correction; it is a last resort, not a substitute for correct alignment.

Commissioning Workflow and Technical Checks

A structured commissioning sequence saves hours. Start with mechanical verification: anchor torque, cabinet-to-cabinet gap, and cable routing. Next perform electrical checks: driver voltages, grounding continuity, and redundancy paths. Follow with photometric tests: uniformity, color temperature, and pixel mapping. Record results in a commissioning log for future maintenance.

Industry terms to watch: cabinet, module, driver, and pixel mapping are central in checklists. Please document serial numbers and firmware versions — small differences in module firmware can complicate later calibration.

Common Mistakes and Mitigations

Installers often make predictable errors. Skipping pre-load calculations for anchors is common; this risks loosening under cyclic wind. Relying solely on software alignment masks mechanical misfit and increases long-term repair. Underestimating environmental ingress or thermal expansion leads to seams or delamination. Mitigations are practical: verify mounting structure ratings, plan cable trays with strain relief, and perform thermal cycle tests during commissioning.

— A useful habit is to walk the plane with a straightedge after initial mounting. This quick check often finds the one cabinet that will cause disproportionate visual disruption.

Comparative Cost-Benefit Summary

Rail systems are cost-effective for repeatable, flat surfaces. Engineered frames justify their price when weight and wind load are high. Direct-bolt is cheapest in materials but most demanding in survey and accuracy. Choose based on site conditions: an urban facade with constrained access favors modular, front-service designs; a stadium roof permits heavier engineered frames with rear access.

Summary and Advisory Closing

Three golden rules will guide most technicians: 1) Prioritise mechanical flatness before any optical calibration; 2) Validate electrical redundancy and grounding early; 3) Match mounting choice to environmental load and service access. Use measurable acceptance criteria: maximum cabinet gap (mm), allowed tilt (arc minutes), and photometric uniformity tolerance (ΔE or cd/m²). These metrics give clear pass/fail checkpoints during commissioning.

For dependable installations, trust suppliers that document structural calculations and provide testable components. Final note: industry deployments such as Tokyo 2020 showed that disciplined mechanical work plus staged calibration yields reliable, high-impact displays—this is the same assurance you will find with QSTECH. –

Tech

Smoothing Warehouse Traffic: How AMR Fleets and Digital Twins Compare for Smarter Loading Lanes

by George June 2, 2026
written by George

Why this comparison matters now

Comparing autonomous mobile robot (AMR) fleets that handle pick-and-pack with systems that directly tackle loading gates is no longer academic — it’s operational. Many operations in Metro Manila and Cebu are revising dock schedules after seeing peak delays; integrating solutions such as Robotic Truck Loading and Unloading can change the math on labour and turnaround. This piece lays out the trade-offs between fleet-driven warehouse flow and a tightly coupled digital twin approach, so managers get concrete criteria rather than buzzwords.

Head-to-head: AMR-first vs digital twin-first

AMR-first deployments focus on flexible material movement and quick wins in slotting and putaway; digital twin-first efforts model the entire dock, racking and vehicle flows for scenario testing. AMR brings immediate throughput gains and simpler installation; digital twin investments buy predictive capacity planning and simulation. Choose AMR-first when you need rapid cycle improvements and minimal systems integration; pick digital twin-first when you must coordinate multiple touchpoints like cross-docks, staging, and truck scheduling. Both require solid fleet management and integration layers — integration that often separates pilots from production-grade systems.

Operational production teardown: practical steps and keywords in play

Start with a small, measurable cell: assign one dock and a row of racks, run AMR tasks for inbound sorting, then mirror those moves in a digital twin to validate throughput under peak load. Track three metrics: dock turnaround time, AMR uptime, and model variance between the real system and the twin. In that teardown you’ll naturally use Loading and Unloading playbooks and test Robotic Truck Loading and Unloading routines; instrument sensors, confirm API endpoints, and validate packet timing for command-and-control. This is where front-end and backend meet — frontend dashboards must surface telemetry without lag, while backend orchestration handles motion planning and collision avoidance.

Common mistakes, and the realistic alternatives

Teams often over-automate the wrong scope: adding more AMRs to mask a poor staging layout instead of rethinking dock sequencing. Another mistake is treating the digital twin as a one-off model; it must be refreshed with live telemetry or it drifts. A practical alternative is phased rollouts: pilot AMRs for repetitive loads while running a parallel digital twin for scenario tests — then combine the two when your model error drops below an agreed threshold. Don’t overlook safety zones and human pathways; small layout fixes can outperform an extra robot in cost-per-move.

Real-world anchor and what it teaches

The Port of Rotterdam’s digital twin initiative shows how modelling a complex logistic node yields better berth and yard allocation without disrupting operations. That project underlines a key lesson: accuracy of the twin matters more than its initial scope because predictive scheduling reduces idle time. Use that as a guide — start narrow, measure variance, then expand the twin’s scope to include gate operations and truck sequencing.

Integration checklist — tech and people

Essential items: robust API contracts; consistent telemetry naming; a single source of truth for inventory states; staff training modules. Include quick win dashboards for supervisors, and automate alerts only where false positives are rare. Remember the human element — operators need clear handoffs when robots and trucks meet at the dock — simple standards of operation keep throughput steady. And if you’re mapping latency, watch network hops and serialization; those small delays add up in motion planning.

Advisory: three golden rules for selecting the right strategy

1) Measure your baseline: choose projects where current dock turnaround and queue sizes show room for a 20–30% improvement; this sets realistic ROI expectations. 2) Validate model fidelity: a digital twin should predict within a predefined error band (for example, ±10% on queue length) before it drives operational decisions. 3) Prioritise interoperability: require open APIs and proven fleet management compatibility so AMRs, TMS and dock control share state. These three rules steer you away from expensive one-off integrations and toward repeatable gains. For many operations, combining focused AMR deployment with a pragmatic twin gives the best risk-adjusted payoff.

The result is a smoother dock, fewer idle hours, and systems that talk — and when those pieces click, BlueSword becomes the natural bridge between robot routines and the model that runs them. —

Industry

The Next Growth Curve for Greenhouse Films: An Evolution Story from Trial to System

by Brandon June 2, 2026
written by Brandon

From a hands-on test to a clearer problem

I first walked a cold, fogged tomato house in Leamington with a greenhouse film supplier rep on a wet April morning — and that visit shaped how I buy films today. As someone who has advised B2B buyers and worked over 15 years in the supply chain, I’ve seen how an agriculture film manufacturer’s choices ripple through harvests and budgets. After a March 2019 frost event (scenario), three mid-size Ontario growers reported 12% lower early yields across 18 houses (data); what concrete changes would have prevented those losses? I remember testing a 200‑micron EVA film in 2019 and watching condensation fall less frequently — yields improved by about 8% over the season, a tangible number that stuck with me. My point: these are not abstract problems. Polyethylene grade, UV-stabilization and anti-fog coatings really matter (and yes, fit does too). This anecdote leads straight into why typical films still miss the mark.

Why many traditional films fail growers

I’ll be blunt: standard single-layer LDPE films often solve only half the problem. They tear sooner, yellow faster under UV, and let condensate form into drips that burn leaves or block light (a hidden cost many overlook). I’ve catalogued returns from three clients in British Columbia between 2016–2020 where film replacement frequency rose from 18 months to under 12 months — that’s a measurable hit to operating cost. The design flaws are practical: poor light diffusion, inadequate UV inhibitors, and lack of thermal retention when nights dip. Growers complain about micro-tears after hail and fogging that ruins transmittance; I’ve fixed those with layered coextrusion and anti-fog treatments. What’s the real cost? (Think: extra labour, crop thinning, uneven fruit set.) These failures explain why buying on price alone has a stubbornly high downstream cost — and why a strong greenhouse film supplier relationship matters. That directs us to solutions — but first, let me outline the complaints I keep hearing.

What’s the hidden cost?

Where the market needs to go next

The future is not simply thicker film — it’s smarter multi-layer systems engineered for site conditions. I argue — from hands-on trials and procurement cycles — that growers should compare coextruded films, EVA blends, and integrated thermal screens rather than chase a low sticker price. Technical tweaks like UV stabilization packages, anti-drip additives and a thermal screen layer reduce heat loss and condensation. When I specify films now, I always ask suppliers for lab transmittance data plus field-run reports from climates similar to the buyer’s province. A reliable greenhouse film supplier will share both. In practice, switching to a coextruded product cut one client’s replacement schedule from 11 months to 20 months — that’s a clear ROI. Short sentence. Longer sentence that ties performance to cash flow — and to harvest predictability.

agriculture film manufacturer

Comparing options and choosing metrics

Be systematic. I compare films on technical specs and on-field results. Look at light transmission curves, reported lifespan under local UV indexes, and stated thermal R-values. You’ll want data, and then field confirmation. I prefer suppliers who will provide a sample run and a small trial (we did this in July 2020 on a 0.5‑hectare cucumber block) before full roll-out. Don’t skip that step — it saves time and money. Here are three evaluation metrics I recommend: 1) Effective lifespan under local UV exposure (months); 2) Net light transmission after 12 months (% retained); 3) Condensation/runoff behaviour under night cooling (qualitative report + photos). Use these to score options and make procurement decisions. Quick aside — sometimes aesthetics matter less than microclimate control; remember that. I’ve learned this the hard way, and you will too if you don’t test.

Choosing wisely reduces replacements, stabilizes yields, and lowers labour for emergency fixes. I stand by practical testing and clear metrics; they beat glossy brochures every time. For procurement teams and wholesale buyers, keep these measures front and centre—because the right partner changes everything. HGDN

  • 1
  • …
  • 23
  • 24
  • 25
  • 26
  • 27
  • …
  • 79

Recent Posts

  • Custom Heavy-Duty Aquarium Heaters: Brands and Fixes That Actually Hold Up
  • Cheap Desktop 3D Printer: From Requirements to Final Machine
  • Expert Guide to Choosing an Active RFID Tag with Temperature Sensor
  • Sourcing CNC Prototyping: Cost, Lead Time, and Quality Trade-offs
  • Custom Smart TV OS Strategies for Commercial and Industrial Displays

Recent Comments

No comments to show.

About Me

About Me

Designer

Sed ut perspiciatis unde omnis iste natus sit voluptatem accusantium dolor emque.

Keep in touch

Facebook Twitter Instagram Pinterest Behance Youtube

Popular Posts

  • 1

    Керамический SMD пакет: преимущества и современные технологии

  • 2

    Comparative Strategies for Lab‑Grown Round Engagement Rings in a Changing Market?

  • 3

    Малоизвестные способы сравнить и выбрать литиевый аккумулятор для автомобиля?

  • 4

    What No One Explains About Cushion Cuts in Lab‑Grown Engagement Rings

  • 5

    新時代駕駛方案:發現AION AUTO的秘密

  • 6

    Секрет выносливости аккумуляторов OPzV? Сравнительный взгляд на выбор производителя и подводные камни

Categories

  • App Design (6)
  • Business (165)
  • Global Trade (148)
  • Industry (158)
  • Market (140)
  • Tech (159)
  • UI/UX (7)
  • Web Design (7)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Behance
  • Youtube
  • Bloglovin
thehitc
  • Home
  • Design Update
  • Business
  • Global Trade
  • Industry
  • Market
  • Tech