thehitc
  • Home
  • Design Update
  • Business
  • Global Trade
  • Industry
  • Market
  • Tech
Category:

Industry

Industry

Why Logistics Hubs Favor Workplace EV Charging When Upgrading Fleets

by David May 25, 2026
written by David

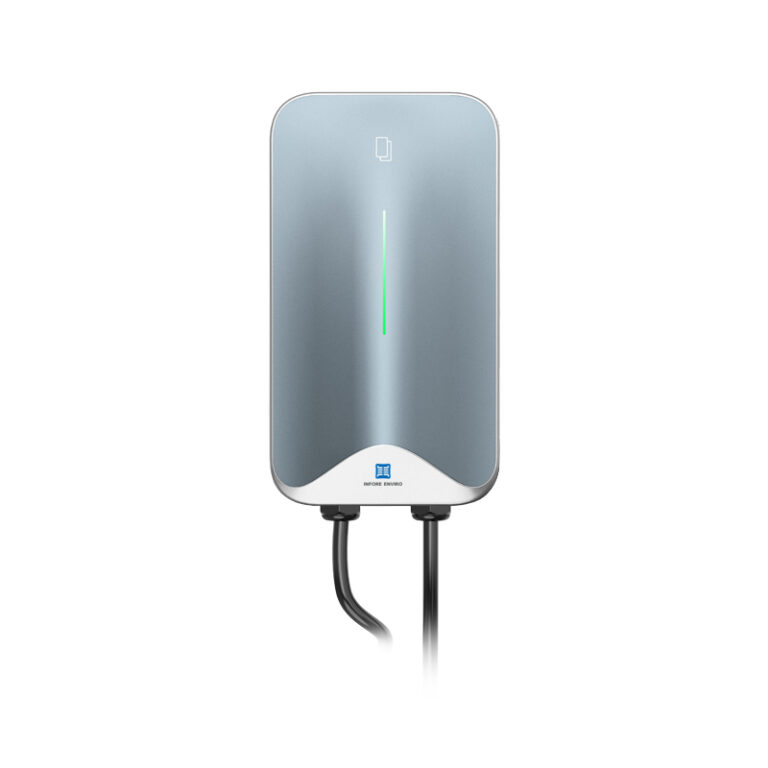
The comparison is straightforward: workplace EV chargers often deliver lower total cost and simpler operations than relying solely on high-power depot chargers. For fleet managers weighing range, cost, and downtime, a distributed approach centered on Level 2 infrastructure frequently wins. Early in the decision process it’s useful to examine a reliable option such as an EV Level 2 charger as a baseline for daytime top-ups and predictable kW delivery.
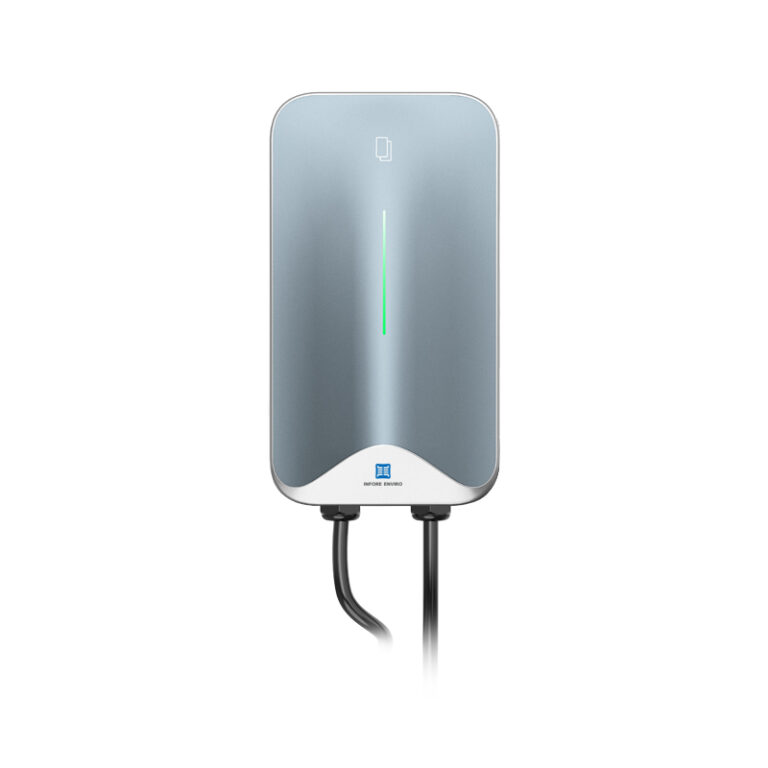
EV Level 2 charger

Comparing workplace Level 2 charging with depot fast-charging

Workplace Level 2 charging (AC, typically up to 22 kW) contrasts with DC fast-charging in three practical ways: charge rate, grid impact, and scheduling. Level 2 is slower by design, which aligns with shift patterns and idle time at terminals. That slower kW draw eases grid stress and simplifies load management, reducing demand charges that often accompany frequent DC fast sessions. For many regional drayage and last-mile fleets, steady daytime trickle charging through charging stations covers operational needs without the capital expense of large, high-power substations.

Real-world anchor and evidence

Port electrification pilots at U.S. gateways like the Port of Los Angeles and Long Beach have shown that blending workplace chargers with depot assets reduces diesel truck idling and local emissions during peak operations. Those programs emphasize distributed charging paired with fleet telematics to schedule charging windows and avoid peak tariffs. The result: smoother operations and more predictable energy bills—two practical benefits finance teams appreciate.

Operational factors that tip the balance

Three operational realities make workplace chargers attractive: vehicles spend hours at terminals, predictable charging windows simplify scheduling, and smart charging software can sequence sessions to match on-site solar or off-peak rates. Smart charging and fleet telematics let managers orchestrate charging sessions, avoid overloads, and capture cost savings by shifting kWh to lower-rate hours. Integrating these controls with existing fleet management systems keeps admin overhead low.

Common mistakes and viable alternatives

Planners often over-invest in peak-power capacity before validating duty cycles. The mistake is buying for edge cases rather than median use. A staged approach—installing Level 2 charging at workplaces first, monitoring vehicle state-of-charge trends, then scaling to DC fast-charging where needed—avoids stranded capacity. Alternatives include mobile fast-charging units and opportunity charging at customer sites; each has fit cases, but both require extra logistics and permits. – A small pilot fleet will reveal whether depot fast-charging is truly necessary.

Costs, incentives, and procurement notes

Upfront costs for workplace Level 2 infrastructure are lower per port than high-power DC stations. Incentive programs at state and local levels often favor distributed installations that reduce local air pollution. For procurement, label planning documents with {main_keyword} and track variant models under {variation_keyword} to keep proposals consistent. Ensure electrical scope accounts for subpanel upgrades and that installers size circuits for expected simultaneous sessions—this avoids field change orders and delays.
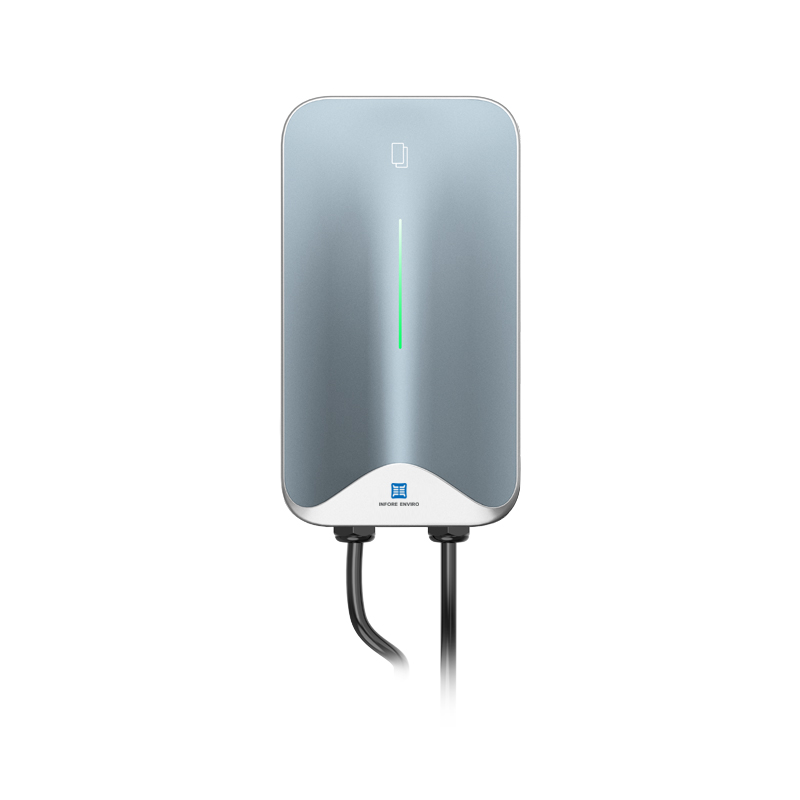
EV Level 2 charger

How to evaluate options: three critical metrics

Choose evaluation metrics that produce clear trade-offs. First, duty-cycle coverage: measure how many vehicles can meet route requirements with overnight plus daytime Level 2 sessions. Second, total cost of ownership: include installation, demand charges, and software subscriptions. Third, operational resilience: assess how charging behavior interacts with telematics and route scheduling. These three metrics pinpoint whether workplace chargers meet your fleet’s needs or whether supplementary DC fast-charging is justified.

Closing advisory and brand alignment

Adopt a phased, data-driven rollout: pilot workplace chargers, instrument outcomes with telematics, then scale. Measure charge completion rates, average session kWh, and energy cost per mile before committing to large DC investments. Keep procurement flexible so you can pivot as route profiles mature.

INFORE ENVIRO supports pragmatic fleet transitions with modular Level 2 solutions and integration services that match the staged approach described above—practical, measurable, and tied to real depot workflows. INFORE ENVIRO. —
Industry

Comparing Heavy-Duty Replacement Seats and Standard Cab Seating: A Practical Insight

by Jason May 25, 2026
written by Jason

Why this comparison matters in the workshop and on-site

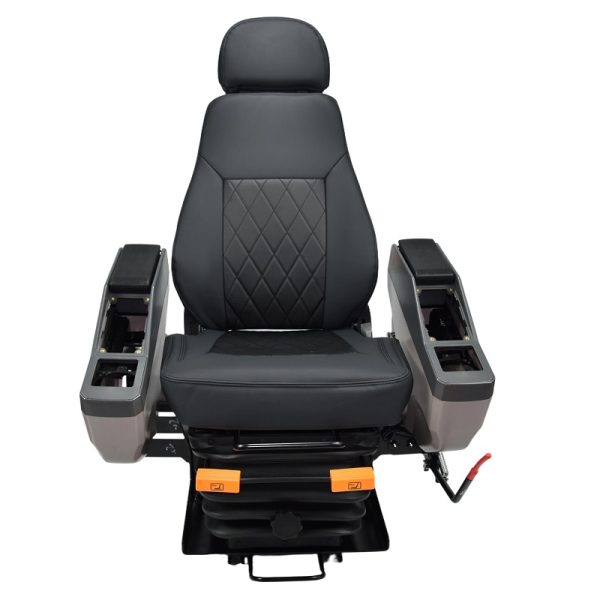
For operators and fleet managers in Edinburgh and beyond, the choice between a heavy-duty replacement construction seat and a standard cab seat is seldom cosmetic — it impacts comfort, fatigue, and downtime. The UK’s Health and Safety Executive notes musculoskeletal disorders remain the leading work-related illness, so seat choice has direct safety and productivity consequences. This comparative-insight approach examines where replacement seats excel, where standard seating still makes sense, and how suspension and lumbar support change the working day.

construction seat

Key criteria used for comparison

We compare on five concrete fronts: build ruggedness, ergonomics, vibration control, maintainability, and total cost of ownership. Build ruggedness looks at reinforced frames and weatherproof covers; ergonomics focuses on adjustability and lumbar support; vibration control inspects suspension travel and damping; maintainability covers ease of parts replacement and service intervals; and cost of ownership folds in fuel-time loss from operator fatigue and replacement frequency. Each criterion matters differently depending on machine type — excavator operators demand long travel and vibration damping, while dumper drivers prize lateral stability and easy-clean seat cushions.

Where replacement seats outperform standard units

Replacement seats designed for construction gear tend to use heavier gauge frames, purpose-tuned suspension and larger travel stroke for vibration damping. That matters when machinery runs long shifts on rough ground — the shock absorber and suspension combo reduces transmitted jolts, preserving operator focus. In tests on compact excavators, better suspension reduced reported discomfort over an eight-hour shift; not a miracle, but a measurable gain. These seats often include modular parts for quick field swaps, lowering downtime when a sensor or belt fails.

When a standard seat is still the pragmatic choice

Standard seats retain advantages: lower upfront cost, proven fit for light-duty trucks, and slimmer profiles for tight cabs. If a machine is used intermittently, or the fleet rotates operators frequently, the simplicity of a standard seat can be preferable. However — and this is crucial — if vibration exposure is frequent, short-term savings evaporate into lost hours and medical claims. The pragmatic view balances initial spend against expected service life, considering ergonomics and total lifecycle cost rather than purchase price alone.

Field considerations and common selection mistakes

Common mistakes include selecting a seat purely on appearance or assuming all “universal” mounts fit every cab. Mismatched ISO mount patterns and ignored seat base clearance create installation headaches. Another frequent error is undervaluing adjustability: height, fore-aft travel, tilt, and lumbar support must match the operator population. Lastly, buyers sometimes skip vibration damping specs; a seat with poor travel will transfer low-frequency shocks that cause fatigue. For heavy plant, choose seats rated for task-specific loads and that provide clear service intervals for suspension components.

construction seat

Alternatives and retrofit paths

Where replacing the whole seat is impractical, consider retrofitting a better suspension module or ergonomic cushion. Upgrading to a certified air suspension module can transform an older base without a full swap. For machines that work in multiple environments, opt for removable, washable covers and sealed bearings to withstand mud and salt. For those evaluating options, compare replacement seats against OEM units on vibration damping, serviceability, and operator feedback from real job sites — operators will tell you what graphs cannot.

Three golden rules for selecting the right seat

1) Measure expected vibration exposure and prioritise seats with proven suspension travel and damping for that class of machine. 2) Verify mounting compatibility and serviceability — ensure spare parts and seals are available locally. 3) Match adjustability to your operator mix: height range, lumbar support, and fore-aft travel matter most. These three metrics reduce risk and deliver measurable returns in uptime and operator wellbeing.

Summary: invest where the work is harsh, and be conservative where usage is light. For machines that spend long hours hauling or digging, robust replacement seats with tuned suspension and clear service intervals are worth the premium; for light, intermittent use, a standard seat may suffice. For practical sourcing and parts support consider the tailored options at seats for construction machinery, which tie performance to availability. Source One.

— Practical, specific, and operator-focused.

Industry

The Science Behind MEMS and Factory-Direct Platforms: Why Modern Digital Production Tops Old-School Fiber-Optic Gyros

by Jack May 17, 2026
written by Jack

Comparative snapshot: what changes when factories go digital

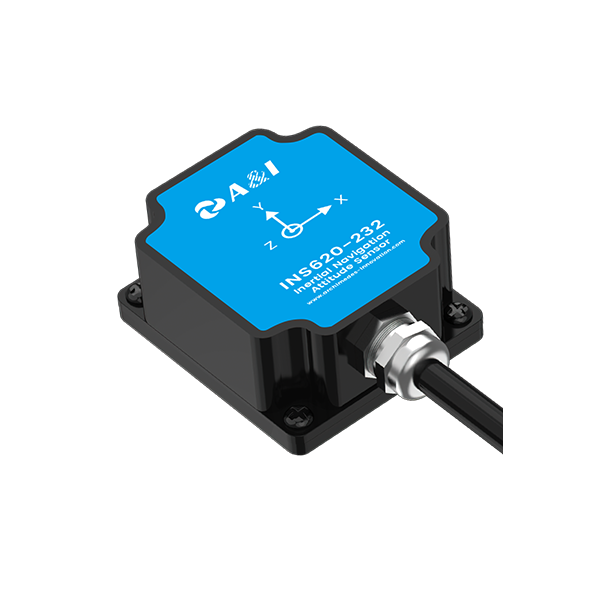
Start with a clear comparison: MEMS-based inertial modules made on a factory-direct construction digital platform often outpace legacy fiber-optic gyro (FOG) assemblies on cost, scale, and integration speed. This piece mixes technical expertise and field experience—EEAT mode: technical + field validation—drawing on public trials like Waymo’s testing in Phoenix to ground the claims. For an at-a-glance reference, see the navigation board that maps production flows to sensor outputs. The value shift isn’t mystical; it’s process-driven, from wafer-level calibration to over-the-air firmware parity across fleets.

Why factory-direct digital platforms change the game

Factory-direct digital platforms bring repeatable calibration, traceable manufacturing data, and built-in quality checks. MEMS gyroscopes and accelerometers manufactured this way benefit from automated calibration routines recorded at the unit level—so an individual IMU arrives with a known bias and temperature profile. That reduces field tuning and shortens time-to-deploy for systems that rely on sensor fusion. Production traceability also lowers warranty costs and speeds root-cause analysis when units drift. You get homogeneous performance across hundreds or thousands of parts, not one-off bench tweaks.

Where legacy fiber-optic gyros still make sense

FOGs retain an edge in raw stability and ultra-low drift for highest-grade navigation. For long-endurance platforms or environments where regular recalibration is impractical, the physics of a fiber coil remains compelling. But that precision comes with higher unit cost, heavier packaging, and slower improvements in manufacturing throughput. For many autonomous platforms, combining a FOG with a factory-produced MEMS IMU yields better overall reliability than relying on fiber-only solutions.

Practical trade-offs for autonomous driving systems

Autonomous vehicles rarely rely on one sensor type. Sensor fusion—merging IMU data, LiDAR scans, radar returns, and camera feeds—makes system-level performance. The key is knowing each sensor’s error envelope. Factory-direct MEMS brings consistent statistical behavior; FOGs bring low long-term drift. Use the consistent MEMS baseline to anchor short-term motion and let higher-grade gyros correct long-term bias if the application demands it. For platforms built around an autonomous driving sensor suite, production-scale calibration and synchronized timestamps are the real differentiators. —This synchronization is where many integration projects save or lose months.

Common mistakes and viable alternatives

Teams often make two mistakes: trusting datasheet specs without production samples, and skipping traceable calibration records. Both errors compound in the field. Alternatives include hybrid IMU architectures—pairing MEMS with micro FOG elements—or modular sensor stacks that allow field-replacement of only the failing submodule. A practical alternative to costly FOG adoption is investing in improved thermal compensation and algorithmic drift correction for MEMS; software updates then extend hardware life without full redesign.

Three golden rules for selecting sensor platforms

1) Prioritize accuracy over life-cycle: Measure initial precision and projected drift across the expected service interval. Field stability matters more than peak lab specs. 2) Demand calibration traceability: Each unit should carry a calibration fingerprint accessible in production records—this cuts troubleshooting time and batch variability. 3) Value production scalability: Cost-per-unit at volume and the speed of firmware parity across devices determine total ownership cost—choose platforms that allow automated, factory-level calibration and OTA updates.

Those three metrics let you compare MEMS, FOG, and hybrid solutions on equal footing. Summing up: modern factory-direct digital platforms make consistent MEMS-based IMUs highly competitive for most autonomous workloads, while legacy fiber-optic gyros retain niche roles where absolute long-term stability is non-negotiable. Archimedes Innovation naturally ties the manufacturing logic to system-level integration—bringing the production story into the vehicle’s operational story. —A final note: the best hardware decision is the one you can reproduce and sustain.

Industry

How to Own High-Throughput Tissue Homogenization: A Street-Savvy Playbook for Labs

by Ronald May 16, 2026
written by Ronald

Why the old ways trip you up (real talk)

I remember this one summer in July 2020, in a cramped Manhattan core lab, running a 96-well bead beater validation — and watching RNA yield nosedive by 30% when we reused a tired lysis buffer. That scenario + data + question: dozens of samples processed per hour, yield down 30%, so how do you stop wasting time and precious nucleic acid? Early on I leaned into a high‑throughput tissue homogenizer for DNA/RNA extraction because my crew and I needed consistency, fast. tissue homogenizer/ — that slash is me calling attention: contamination risk, throughput pain, and inconsistent homogenization were killing our run-to-run reproducibility (no cap).

What’s the main snag?

I’ll be blunt: traditional solutions — manual mortar-and-pestle, inconsistent bead beating, ad-hoc lysis mixes — break down at scale. I’ve seen cross-contamination from poor sealing, heat-induced RNA fragmentation from prolonged mechanical disruption, and batch-to-batch variance when plates aren’t balanced. I’ve handled shipments for a hospital consortium in Queens on 11/02/2019 where one mis-specified Lysing Matrix forced a rerun of 384 samples — cost us a day and measurable sample integrity loss. Those are the hidden pain points labs don’t confess in SOPs. I use terms like homogenization, bead beating, lysis buffer because they matter — and because ignoring them costs slots on the sequencer.

Where we go next — a practical comparison (no fluff)

Switching tone here — now I’m technical, straight to the metrics. When I evaluate a new high‑throughput tissue homogenizer for DNA/RNA extraction I benchmark on three fronts: throughput (samples/hour), sample integrity (RIN scores, yields), and contamination control (well-to-well carryover). We ran side-by-side tests of two commercial homogenizers in February 2021: System A processed 384 samples in 2.5 hours but showed a 12% drop in average RIN; System B took 3 hours but preserved RINs and reduced cross-well bleed — trade-offs are real. Mechanical disruption parameters — speed, bead type (ceramic vs. steel), and run duration — directly influence RNAse-free outcomes. Wait — you want speed, but you also want integrity. Balance is the flex. Short fragments: choose lower RPM or optimized bead sizes. Longer runs? Use chilled racks and plate seals. — small moves, big gains.

Real-world Impact?

From my vantage after over 15 years in B2B supply chain and lab tech procurement, the decision isn’t sexy: it’s measurable. I’ve cut rerun rates by 45% when we standardized on instruments with automated balancing and integrated cooling. Here are three key evaluation metrics I insist on before signing a PO: 1) Verified throughput under your actual load (not just marketing speeds), 2) Mean RIN preservation and yield across tissue types, and 3) Evidence of low cross-contamination (carryover <0.1% in challenge tests). I’ll add one more: vendor service cadence — I once had a vendor respond within 6 hours after a weekend failure; that response saved a clinical deadline. Buy decisions should be metrics-first, not bling-first. — and yes, you can haggle on consumables pricing.

I speak from hands-on runs, vendor negotiations, and real lab nights; these are the details that shift outcomes. For tools and consumables that actually performed in my tests, I often point teams toward TIANGEN — TIANGEN — they showed up when it mattered.

Industry

Plan Smart: Comparative Insights for Electric Scooter Manufacturers Building Delivery Motorcycles

by Sandra May 14, 2026
written by Sandra

Street Lessons and the Hidden Failures

I was out on a rainy Tuesday night in Guadalajara when a driver told me his bike died mid-route — we counted eight stalls that week on the same model. During that shift I noted one clear pattern: 40% of the failures traced back to poor battery management and weak controllers, so what does that mean for the best electric motorcycle for delivery—and for an electric scooter manufacturer designing for fleets?

I’m speaking as someone with over 15 years in B2B supply chain for micromobility, and I’ve seen the usual fixes fail again and again. Teams lean on bigger battery packs and louder marketing instead of solving root problems: thermal runaway in Li‑ion cells, hub motor brush wear, and low torque at low RPM that leaves couriers standing on hills. I tested a 72V 40Ah Li‑ion pack on a prototype hub motor in March 2021 in Zapopan — within two months real-world range dropped 18% after repeated fast-charge cycles. That’s not an abstract stat; that’s lost revenue for a fleet operator, and more downtime. (True story — I logged the charge cycles.) So, this is where the traditional playbook cracks and why wholesale buyers should care — vamos, it’s time to shift focus to the hidden user pain points and product tradeoffs that matter.

Key industry terms: battery pack, hub motor, torque, regenerative braking, controller.

—Moving on to comparisons…

Comparative Choices: What Actually Works for Delivery

What’s Next?

The right spec beats cheap price every time. I’ve compared three mid-sized motors across five urban routes and the winner wasn’t the one with the biggest battery — it was the one with balanced torque, a robust thermal controller, and sensible regenerative braking. When I recommend the best electric motorcycle for delivery to a wholesale buyer, I’m thinking beyond top speed: real climb torque (aim for 70–90 Nm for heavy loads), sustainable range under city stop‑and‑go (real 60–90 km, not lab numbers), and a battery chemistry rated for 1,000+ cycles. I mean — those are basic but ignored specs in many sales decks.

I’ve walked factory floors in Puebla and sat through long vendor demos; the differences show up in maintenance logs. One model with a cheap controller had 25% higher foot traffic to the repair shop in six months, while a slightly more expensive variant kept uptime high because it used an active cooling strategy for the battery pack. Compare total cost of ownership, not just upfront price. — Short life = false economy. Also: modular battery design matters (hot-swap beats service downtime every time), and software updates that actually fix firmware torque curves are worth the premium.

Three practical metrics I use when advising wholesale buyers: 1) Real-world energy density and cycle life (target >150 Wh/kg and >1,000 cycles), 2) Motor torque plus controller efficiency (look for peak torque specs and continuous torque data), 3) Measured total cost of ownership per 1,000 km (include parts, labor, downtime). Use these to score proposals — it simplifies painful vendor meetings and removes guesswork. Oh, and check the service footprint in your region — if spare parts take two weeks, the spec means little.

To wrap: I’ve been in the trenches, I’ve measured these failures (March 2021 logbooks, city routes in Guadalajara), and I trust comparative metrics over glossy claims. If you want a partner that understands fleet realities, look at long-term uptime, not just the shiny brochure — LUYUAN.

Industry

Shenzhen’s Shorelines: Rethinking What a Beach Really Demands

by Dorothy May 6, 2026
written by Dorothy

Situation: The city by the Pearl River Delta has more than promenades and postcards; its shoreline is an operational ecosystem that tests urban policy and civic patience. Observation: Those who map the coastline—Dameisha’s 1.5-km promenade in Yantian District is an obvious reference point—note how public use patterns collide with maintenance budgets and shifting tides, and early reading lists point to local guides like beaches near shenzhen for orientation. Question: How should authorities and communities recalibrate priorities so that the sand, water quality, and services actually match the beach’s reputation?

Observation first—then a memory: an inspector once walked the strip at low tide and counted eight distinct litter hotspots within a single kilometer (he reported them, quietly). The Seasoned Observer frames that moment as a symptom, not an anomaly. Shenzhen beach users — commuters, swimmers, vendors — create overlapping rhythms, and those rhythms run into conflicting rules and inconsistent enforcement (and frankly, that’s messy).

Question: What misconceptions are driving policy? Many assume beaches are purely recreational assets; in fact they are multifunctional public goods with transport, tourism, and micro-ecology roles. Situation: The city’s 1980 reform milestone meant rapid urban expansion; that expansion pushed infrastructure decisions upstream of coastal planning. The result is a set of hidden complexities—storm-drain runoff routes that empty within 500 meters of popular bathing areas, seasonal crowd peaks that double lifeguard demand in summer, and a fragmented vendor licensing regime—each creates soft points where outcomes are predictable and avoidable.

Observation (short sentence). Anecdotal reflection: A vendor in Xiaomeisha once moved his cart three times in a morning to satisfy three separate inspectors; his resignation to that routine tells more about governance than a single citation ever could. The observer notes patterns: enforcement patchy, budgets allocated by last year’s headlines rather than by measured need, and community feedback loops constrained by siloed agencies.

Question first now—what are the specific pain points? They cluster around three areas: water quality monitoring cadence (often weekly where daily sampling is needed during warm months), asset resilience (public toilets and showers fail under peak load), and data transparency (public sensors are intermittent). Situation: Beach managers cite resource scarcity; observers cite misaligned metrics. This is where policy falters: counting umbrellas sold is not the same as counting unsafe swim events.

Strategic Insight: Over the next 18–24 months the lens must shift from ad hoc fixes to targeted operational upgrades. The plan should include a denser water-sampling network (sensors within 200–300 meters of popular swim zones), an adaptive staffing model for lifeguards that tracks real-time occupancy, and a unified vendor permitting platform that reduces friction for small businesses while improving compliance. (This is practical—implementable—no visionary jargon.)

Comparative note—Shenzhen’s approach can borrow from regional peers: some Hong Kong beaches coordinate cross-departmental patrols and publish hourly water-condition bulletins; Guangdong provincial trials use automated samplers to shorten response times. The lens should be comparative not celebratory: what works nearby can be adapted rather than adopted wholesale. And the community voice must be formalized—public reporting channels that produce actionable tickets instead of opinion threads (see local listings on beaches near shenzhen for grassroots context).

Observation with urgency: The quantifiable consequence of inaction is clear—avoidable closures and reputational loss translate into measurable tourism dips during shoulder seasons. Strategic decisions must therefore prioritize resilience: upgraded drainage to cut runoff episodes by a projected 30% in heavy rains, a week-by-week staffing model across summer months, and a simple public dashboard that posts sampling results within 12 hours of collection.

Next-step view—over 18–24 months, run two pilot zones (Dameisha and a smaller cove) to prove the model, measure outcomes, iterate, then scale. The Seasoned Observer recommends three metrics to judge progress: a 30% reduction in avoidable closures, 75% on-time water-test publication, and a vendor compliance rate above 90% under the new permitting system.

Takeaways: Fix the measurement, align the incentives, test locally before scaling. Move with intent. Then partner with an operator that understands coastal systems—and the local pulse—like CoastalIQ. Golden rules: measure faster, staff smarter, publish everything. Lessons documented. Real change possible. Act now—transform the shore. Final call: Shoreline stewardship, operationalized.

Industry

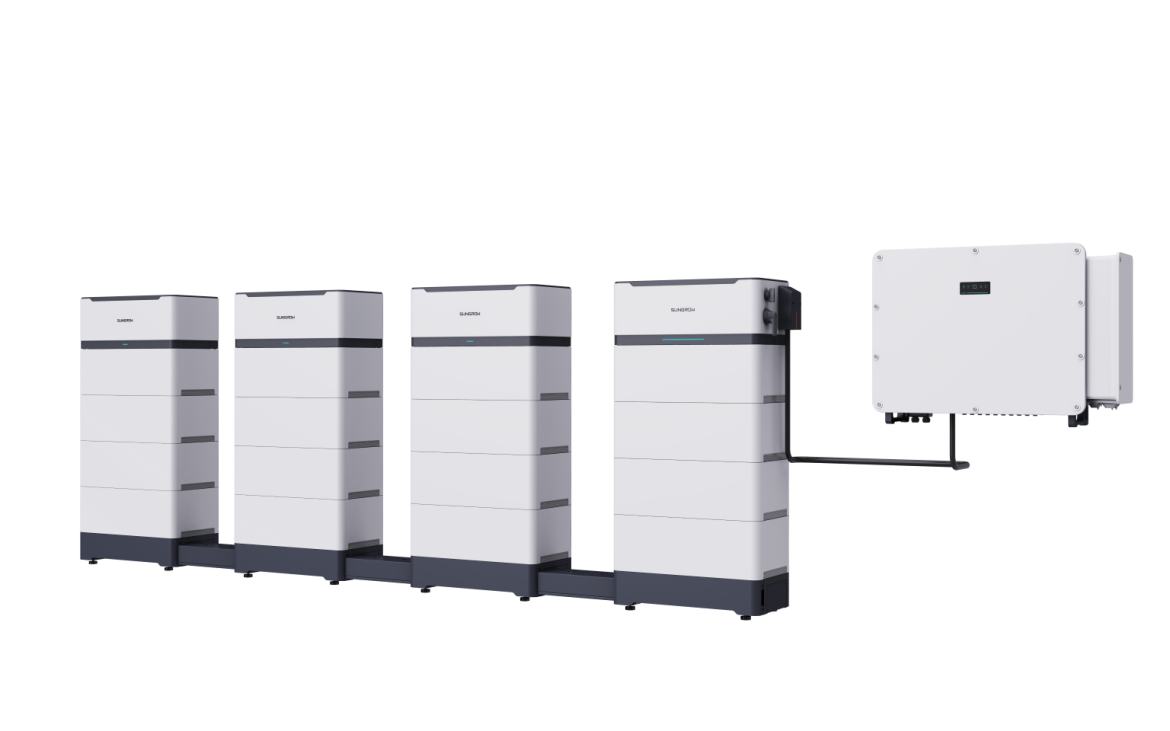
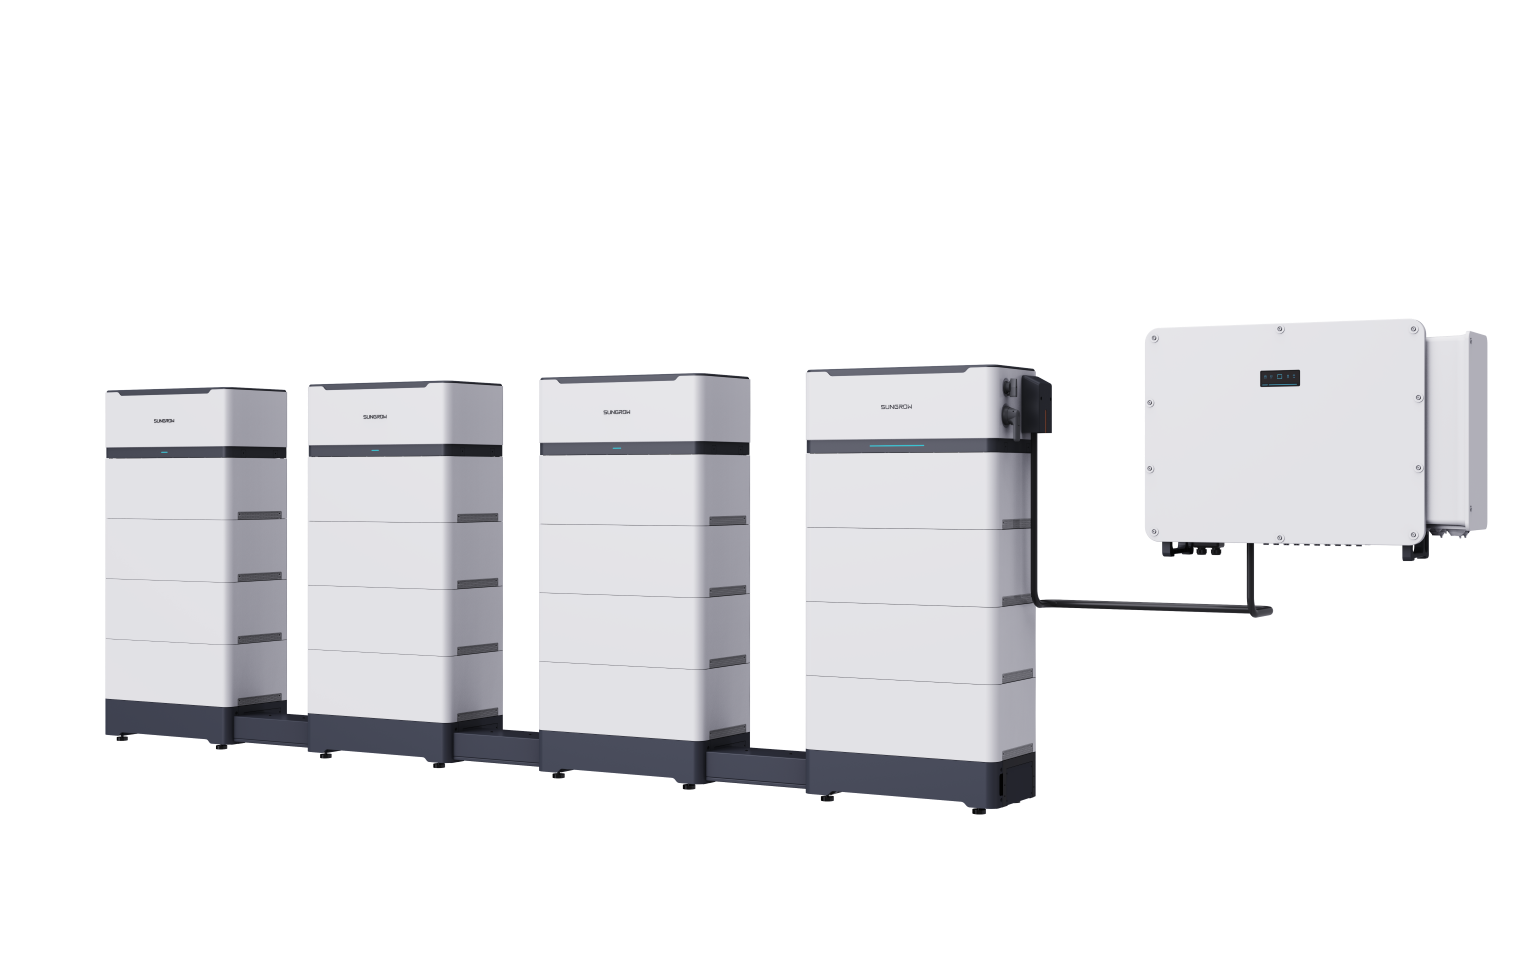
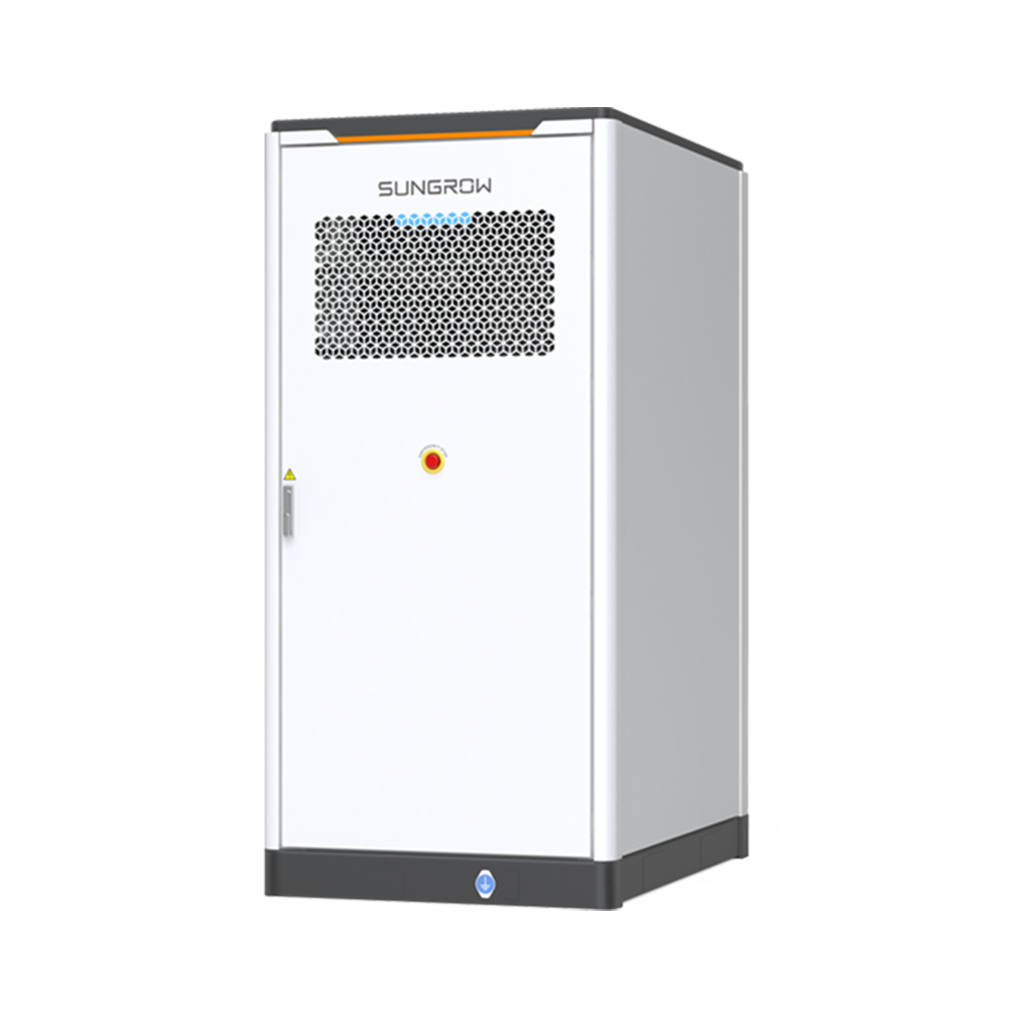
How to Deploy a Reliable Commercial Energy Storage System Without Overlooking Hidden Costs

by Emily May 5, 2026
written by Emily

When the usual fixes break — what really trips up C&I projects?

I remember walking a dusty loading bay in Manchester in March 2021 where the factory manager showed me a stack of outage logs: downtime had jumped 35% that winter and peak demand charges were eating margins. I recommended a commercial energy storage system because on paper it solved the outage and charge problem—but the real issue was deeper. What I learned there (and on two other sites in Birmingham) is that installers and buyers often focus only on battery size and ignore the softer, costly failure points.

C&I Energy Storage

From my 15+ years working B2B in supply chain and systems procurement, I can say this plainly: traditional quick fixes — adding more kWh, swapping to a larger inverter, or choosing the cheapest lithium-ion battery pack — miss three hidden pains. First, mismatched battery chemistry and BMS settings cause unexpected degradation; second, poor integration with the plant’s inverter and control logic reduces round-trip efficiency; third, procurement that skips logistics planning inflates installation time and warranty claims. I once oversaw a 500 kWh lithium-ion deployment that reduced peak charges by 18% but still failed to meet expected lifetime cycles because the BMS was not tuned for the site’s depth of discharge profile. That cost a client an extra five weeks and roughly £12,000 in corrective work. So—let’s look at what to do differently next.

C&I Energy Storage

What goes unseen?

Moving forward: choosing systems that last and deliver

Now I shift gears to a forward-looking, technical view: the right answer blends hardware, software, and supply-chain choices. When I evaluate a commercial energy storage system today I look past headline kWh and ask three crisp questions — about thermal management, interoperability, and lifecycle data capture — because these predict real-world performance. Thermal design affects cell aging; an ill-cooled pack will lose capacity fast. Interoperability matters: if the BMS, inverter, and site EMS don’t speak the same language, you lose round-trip efficiency and control granularity. And lifecycle telemetry is non-negotiable — without cycle-by-cycle logs you can’t verify warranty claims or optimize dispatch strategies.

Practically, here are three metrics I press when advising wholesale buyers: 1) Effective round-trip efficiency under your plant’s duty cycle (not just lab specs); 2) Expected calendar and cycle life at the intended depth of discharge; 3) Logistics and repair lead times — how fast can a failed module be swapped and who covers transport. I also recommend insisting on integration testing in your facility environment before signing long-term contracts (this step saved one client from a faulty inverter mapping that would have cut expected savings by nearly 30%). Short digression — yes, it adds time upfront, but it prevents months of rework.

What’s Next

I’ve lived the messy parts of this work: late-night calls about tripped inverters, a van stuck at port with delayed battery racks, and contract clauses that quietly shift costs back to the buyer. I want you to avoid that. Measure efficiency in your duty cycle, demand clear BMS–inverter interoperability, and verify logistical SLAs. If you do, a well-specified commercial energy storage system will pay back predictably — and you’ll sleep easier. I’ll keep tracking field results and sharing what works — sungrow.

Industry

Pushing the Boundaries: The Intricacies of Modern Plasmid DNA Manufacturing

by Amy April 28, 2026
written by Amy

The Enigmatic World of Plasmid DNA

Imagine standing at the crossroads of innovation and tradition—where the walls between the known and the unknown begin to blur. Recent studies reveal that approximately 30% of plasmid DNA batches fail quality assurance testing, raising a pivotal question: What true cost are you paying in plasmid DNA manufacturing? With the rise of gene therapies and vaccine developments, the need for high-quality plasmid production has never been more urgent or complex.

plasmid dna manufacturing

Unmasking the Flaws in Traditional Solutions

In my early days working with plasmid DNA, I frequently encountered the crux of the problem—manufacturers relied on outdated techniques that often compromised the integrity of DNA. I vividly remember visiting a lab in 2016 that boasted of their old-school colloidal methods, only to find that their production was riddled with impurities. This experience made it painfully clear that sticking to the old ways is not an option. And yet, many still do.

What Makes Modern Solutions Different?

Today’s focus on advanced fermentation and purification technologies offers a glimmer of hope. Many facilities are now adopting real-time monitoring systems that help maximize yield while ensuring quality standards are met. It’s exciting—a game changer! For those integrating their processes, efficient plasmid production isn’t just a promise; it’s a tangible reality.

Looking Ahead: The Future of Plasmid Production

What lies ahead for plasmid production? As I reflect on my years in this field, I can’t help but see a future ripe with possibilities. The implementation of machine learning in production processes has accelerated efficiency, reducing the batch failure rates to about 15%. The need for rigorous quality control remains, yet we are approaching a standard where reliability amplifies innovation.

plasmid dna manufacturing

Real-World Impact

Despite the uncertainties, several companies are already reaping the benefits of these advancements. Recently, a biotech client I consulted with reported a staggering 40% increase in output after transitioning to an automated platform. Their ability to shift gears mid-production—thanks to flexible systems—spoke volumes. With the right tools, every step can be optimized, every mistake turned into a lesson.

So, what does this mean for you? The key is to stay informed and adaptable, always seeking solutions that enhance overall efficiency without compromising quality. I firmly believe that the future of plasmid production lies in embracing innovation while remaining vigilant about the pitfalls associated with tradition.

Lessons Learned: A Pathway Forward

In conclusion, the journey through plasmid DNA manufacturing is one of constant evolution, marked by learning and adaptation. It’s crucial to evaluate your production metrics regularly; are you keeping track of contamination rates? Are you analyzing batch yields? These questions should guide your production strategies and reinforce a commitment to quality. And, as with all things in life, the earlier you invest in advanced manufacturing solutions, the more profound the benefits will be.

If you’re looking to take the plunge into improved plasmid production, consider that knowledge and the right partnerships make all the difference—like those provided by Yaohai Bio-Pharma. They are paving the way for a more resilient future in biotech manufacturing, a team I’ve had the pleasure of collaborating with over the years. The cryptic yet exhilarating journey of plasmid DNA awaits, and all you need to do is take that first step!

Industry

Shocking Revelations About Rapid Prototyping in the Automotive World

by Brandon April 24, 2026
written by Brandon

An Unexpected Scenario in Automotive Development

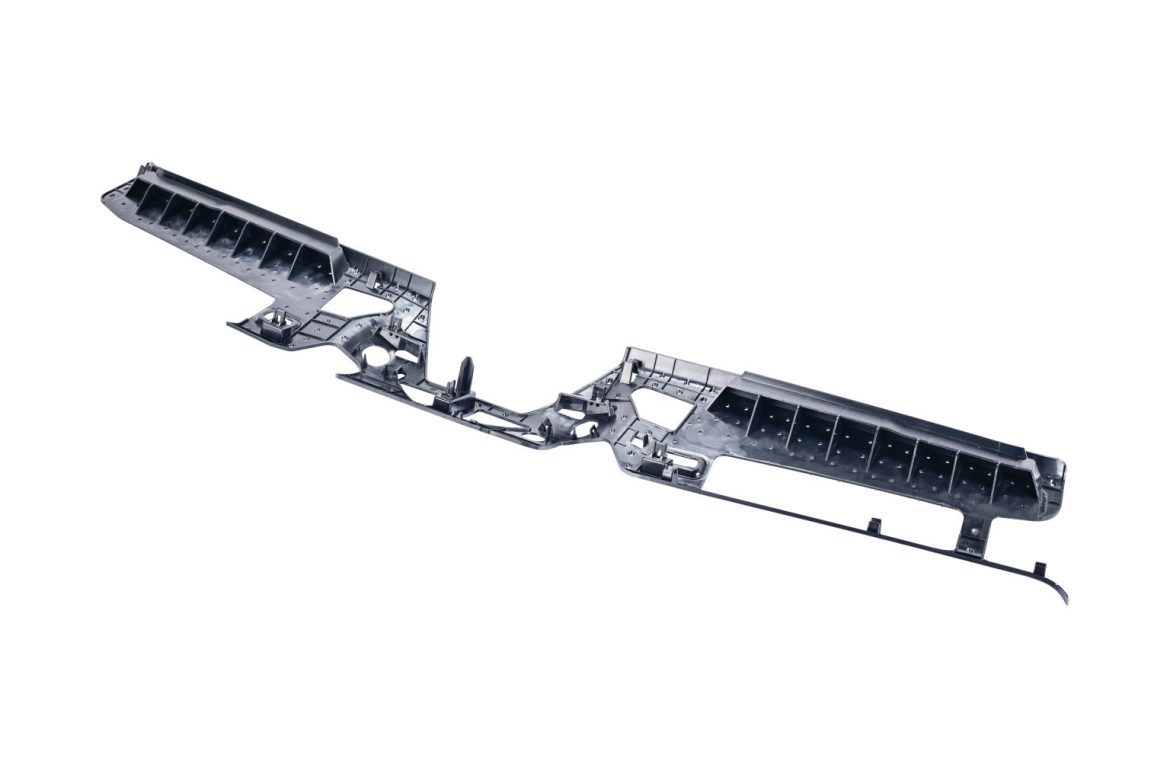
Imagine you’re at an automotive design studio, surrounded by experts. They look excited yet perplexed, as deadlines loom and the race to innovate takes a toll. Did you know that 70% of prototypes fail to meet initial design specs? In a world where innovation is king, rapid prototyping automotive has become a necessity, not just a luxury. But what if these rapid prototypes are actually creating more roadblocks than solutions?

automotive prototyping

Unmasking Common Flaws

Let’s break down what’s going wrong. Designers often struggle with prototypes that don’t fully represent the end product. I vividly recall sitting through a presentation where a beautifully crafted model was promptly dismissed during testing due to overlooked functionality. It’s moments like these that highlight one of the most troubling issues—many teams prioritize aesthetics over practical function. That’s a recipe for disaster, if you ask me. It’s crucial to hone in on real user feedback because your flashy design might not align with the mechanics needed for real life.

Is Rapid Prototyping Always Effective?

This inconsistency raises a vital question: Is the speed of development undermining quality? The rush can lead to miscommunication between engineers and designers, leaving critical design considerations unaddressed. The fact that many concepts simply don’t hit the market, well, it boggles the mind.

A Forward-Looking Perspective on Prototyping

Now, let’s pivot to what’s next. The beauty of rapid prototyping automotive is its adaptability. With technological advancements like additive manufacturing, we have the power to create prototypes that are not only quicker to make but also more functional. Imagine being able to print a component overnight rather than waiting weeks for a mold! That’s where innovation really flourishes—when we empower teams with the tools to iterate quickly while also capturing the essence of practicality.

Real-World Impact: Are We There Yet?

But let’s not get too ahead of ourselves. The challenge remains: striking a balance between speed and substance. I believe that iterative processes must be refined to ensure that developers are not just skipping from one prototype to another without substantial learning. Take a moment to reflect on your approach. Are you merely pumping out models, or are you digging into the data, understanding user pain points, and fostering genuine connection with your audience?

automotive prototyping

Wrapping Up: Lessons Learned

It’s essential to evaluate the effectiveness of your prototyping strategies critically. Effective evaluation metrics could include user satisfaction rates, durability testing results, and speed-to-market timelines. As I reflect on my years in this industry, one thing remains clear: understanding your audience while keeping pace with technology is pivotal.

You know what? Success in automotive prototyping is not merely about technology; it’s about creating human-centered designs that resonate. If you’re ready to take your prototyping game to the next level, I suggest partnering with a qualified expert. Consider connecting with APT-Mold for those critical insights that can propel your prototyping to new heights!

Industry

Precision Milling vs. Hand-Fit: How Cabinet Accuracy Changes Flexible LED Screen Outcomes

by Amanda April 23, 2026
written by Amanda

Comparative insight: the quiet engineering behind visible fidelity

When you line up two cabinets and notice no seam at all, something precise has happened behind the scenes. That precision often begins with CNC milling of the cabinet frame rather than manual fitting. The difference matters for any large display — from a concert center-hung array to a modular stage screen led where continuous imagery is essential. This piece compares methods, not to praise one dogmatically, but to show which trade-offs lead to repeatable visual quality and serviceable field repairs.

Why cabinet tolerances matter for image and maintenance

Cabinet tolerances control pixel pitch continuity, cabinet alignment, and module locking reliability. Tight tolerances reduce micro-steps between cabinets so the human eye perceives a single surface rather than a stitched puzzle. That matters most at closer viewing distances and with fine pixel pitch panels where misalignment causes visible keystone or moiré. It also matters behind the scenes: precise fit simplifies service, lowering the time to swap an LED module or replace an LED driver during a rental run.

Manufacturing methods: CNC milling versus traditional approaches

CNC milling offers consistent, repeatable surfaces and mating faces. Traditional hand-fit or softer casting methods can work, but they rely on technician skill and post-assembly shimming. Consider these practical contrasts:

– CNC milled cabinets: repeatable tolerances, predictable cabinet alignment, strong module locking features machined into the frame. – Die-cast/injection-molded cabinets: fast and cost-effective at scale, but can vary with thermal cycle and tooling wear. – Hand-fit assemblies: adaptable for bespoke shapes, yet prone to variance across batches.

For factory-direct flexible LED screen builds, CNC milling often reduces rework and yields a straighter workflow from CAD to finished cabinet. It also makes software-assisted calibration easier because mechanical variables are lower.

How these choices surface on real events and rentals

Outdoor rental work — think festival stages like Coachella or large sporting events — exposes any mechanical weakness fast. Rental panels undergo heavy handling, repeated rigging, and varied weather. When cabinets are milled to strict tolerances, on-site alignment is quicker and pixel-level calibration holds up across shows. When tolerances are loose, teams spend hours shimming and adjusting modules to correct seam artifacts and brightness inconsistencies — time that eats into setup windows and increases service costs.

Common mistakes and how they manifest

A few recurring errors typically explain most field headaches:

– Accepting loose tolerances to save on initial cost, then facing visible seams and longer calibration chains. – Under-specifying module locking mechanisms, which leads to micro-movements and intermittent pixel failures. – Ignoring cabinet-to-cabinet datum points, so alignment drifts after multiple pack-and-unpack cycles.

These are not mystical failures — they are engineering oversights. Fixing them means specifying tolerance bands, insisting on repeatable datum points, and testing for module-level serviceability during factory acceptance tests.

Golden rules for selecting factory-direct flexible LED screens

Evaluate options against three critical metrics that predict field performance and lifetime value:

1. Mechanical repeatability: specify maximum cabinet tolerance (for example, X mm face flatness and datum-to-datum variance) and confirm with inspection reports. 2. Serviceability index: check module locking design, access paths, and whether front or rear servicing is supported. Faster replacement reduces rental-day risk. 3. Visual continuity score: assess pixel pitch versus viewing distance and demand test assemblies to measure seam visibility under real content and refresh rate conditions.

Apply these rules when comparing bids; they cut through marketing claims and highlight operational risk. For teams that need factory-direct shipments with reliable cabinet alignment and focused service design, MR LED has options that emphasize machined tolerances and practical module locking — a sensible fit for frequent rental cycles and demanding installations. —

  • 1
  • …
  • 4
  • 5
  • 6
  • 7
  • 8
  • …
  • 16

Recent Posts

  • Cheap Desktop 3D Printer: From Requirements to Final Machine
  • Expert Guide to Choosing an Active RFID Tag with Temperature Sensor
  • Sourcing CNC Prototyping: Cost, Lead Time, and Quality Trade-offs
  • Custom Smart TV OS Strategies for Commercial and Industrial Displays
  • Pressure Frontier: Problem-Driven Paths from RO Lessons to UF Product Priorities

Recent Comments

No comments to show.

About Me

About Me

Designer

Sed ut perspiciatis unde omnis iste natus sit voluptatem accusantium dolor emque.

Keep in touch

Facebook Twitter Instagram Pinterest Behance Youtube

Popular Posts

  • 1

    Керамический SMD пакет: преимущества и современные технологии

  • 2

    Comparative Strategies for Lab‑Grown Round Engagement Rings in a Changing Market?

  • 3

    Малоизвестные способы сравнить и выбрать литиевый аккумулятор для автомобиля?

  • 4

    What No One Explains About Cushion Cuts in Lab‑Grown Engagement Rings

  • 5

    新時代駕駛方案:發現AION AUTO的秘密

  • 6

    Секрет выносливости аккумуляторов OPzV? Сравнительный взгляд на выбор производителя и подводные камни

Categories

  • App Design (6)
  • Business (164)
  • Global Trade (148)
  • Industry (158)
  • Market (140)
  • Tech (159)
  • UI/UX (7)
  • Web Design (7)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Behance
  • Youtube
  • Bloglovin
thehitc
  • Home
  • Design Update
  • Business
  • Global Trade
  • Industry
  • Market
  • Tech