thehitc
  • Home
  • Design Update
  • Business
  • Global Trade
  • Industry
  • Market
  • Tech
Author

Sarah

Sarah

Business

Preclinical Contract Research: A Manufacturer’s Handbook for OEM and Project Buyers

by Sarah October 12, 2026
written by Sarah

Problem — when a study tastes off

The kitchen of preclinical work should smell of precision: calibrated balances, crisp SOPs, a clear endpoint. Instead, many OEMs and project buyers find results that taste flat—misaligned protocols, shifting inclusion criteria, missing raw data. Teams working across pharmacology disciplines, from small molecules to veterinary pharmacology, hit the same stubborn problem: expectations that weren’t spelled out become technical debt, and timelines curdle into delays. The problem is straightforward and fixable, but only if you diagnose it like a chef testing seasoning at every stage.
veterinary pharmacology

Diagnosis — the undercooked causes

Samples mishandled. Assays validated on paper but not in practice. Contract terms that leave data ownership ambiguous. These are the undercooked elements that ruin a study. Sensory cues show up as data noise: inconsistent controls, unexpected variability, endpoint drift. The root causes are operational and contractual — poor handoffs between lab and client, vague acceptance criteria, inadequate chain-of-custody. Fix the basics first: crisp specs, transparent methods, and someone responsible for tasting the batch at every milestone.

EEAT — experience anchored to regulatory reality

Decades in lab benches teach one lesson: reproducibility is earned. That practical eye comes from repeat runs, third-party audits, and aligning methods with regulators. Guidance from the FDA’s Center for Veterinary Medicine (CVM) on toxicology assessments shapes expectations for study design and safety margins, and that regulatory frame reduces guesswork. For teams focused on safety and dose selection, veterinary toxicology​ resources and standards matter — they set the sensory baseline for acceptable variability and tolerated impurities. Trust comes from published validation, documented chain-of-custody, and sample traceability; expertise shows in how quickly a lab spots an outlier and reruns the assay without drama.
veterinary pharmacology

Common pitfalls — sharp knives to handle with care

Relying on a single pilot run. Skipping matrix-specific validation. Vague acceptance criteria that leave interpretation to the lab’s convenience. Each pitfall is avoidable. Require triplicate runs, demand matrix-matched calibrators, and codify acceptance thresholds in the contract. Insist on raw data delivery in machine-readable form. Ask for a decision tree for deviations so a stray value doesn’t become a hidden rework later. These steps are practical: they stop small errors from tasting like complete failure.

Alternatives — choosing the right method to simmer

You have three sensible routes: build in-house capability, partner with a full-service CRO, or work with specialized OEM manufacturers. In-house gives control but costs time and capital. CROs offer breadth and process maturity; specialized manufacturers bring niche platforms and bespoke instruments. Compare on three tangible measures: turnaround reproducibility, audit trail clarity, and contractual data ownership. Don’t chase the cheapest menu item; pick the partner that consistently plates the same dish to spec.

Synthesis — the recipe that delivers

Start with a clear brief, season with validated methods, and insist on transparent data from day one. Fix the contract language so responsibilities are crisp, require pre-agreed acceptance criteria, and bake in third-party review points. When these elements are arranged, projects stop smelling of uncertainty and begin to taste reliable. That practical, methodical approach is exactly what experienced partners like KCI Biotech bring to the bench: steady technique, traceable processes, and outcomes you can measure against your original specification.
Business

Automotive Battery Automation: Layout, Capacity, and Process Fixes

by Sarah September 25, 2026
written by Sarah

Quick problem snapshot

Too many battery plants look great on paper and choke on the floor. I’ve seen lines stop because of layout guesses, wrong capacity math, or a process step nobody automated right. If you’re staring at cell handling, stack flow, and takt mismatches, start by studying how people actually build throughput — that’s where battery manufacturing automation matters most. I’ve run floor audits and built simple dashboards that make the real issues obvious within hours.

battery manufacturing automation

Layout pain points and fixes

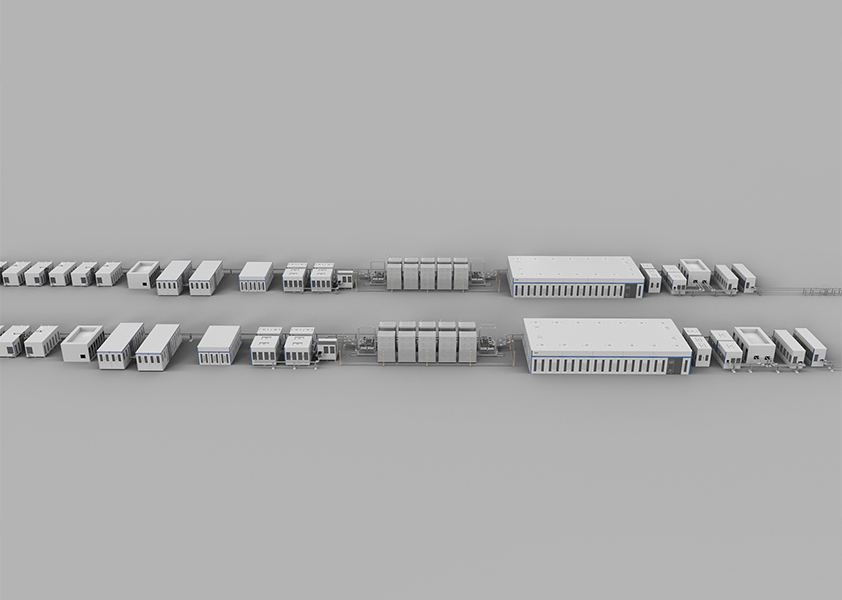
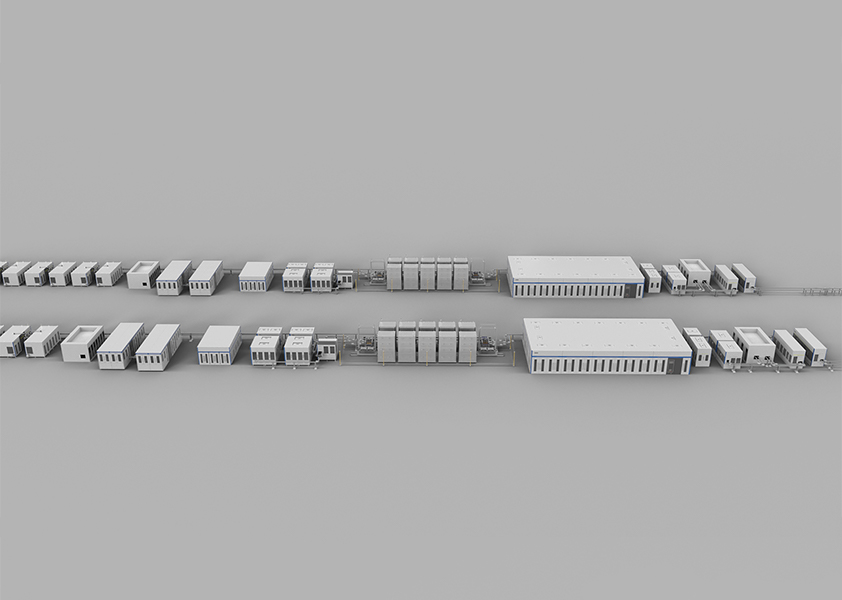
Problem: congested flow and mixed functions in the same cell. Fix: split stages and create clear material lanes. Short list of practical moves you can apply now:- Move heavy prep (incoming inspection, kitting) out of the main line so the line stays pure assembly. – Use modular islands for high-variance steps; swap a module instead of redesigning a whole line. – Place buffers where cooling or test cycles happen to avoid halting upstream cells. These cuts reduce handoffs and make automation predictable. Keep tool footprints lean—don’t bury robots in 3D mazes. I’ve measured cycle time drops after converting snaking layouts into straight feedlines during on-site reviews.

Capacity mismatches: predictable causes and remedies

Problem: designed peak capacity doesn’t match real takt. Start by locking target takt time to demand, not equipment specs. Typical fixes:- Parallelize the slowest station rather than pushing everything faster. – Add short-term surge buffers sized for one production shift’s max variance. – Plan for incremental capacity: design extra space and a simple power hookup before populating it. If you skip surge planning you end up with idle lines or desperate retrofits. Real sites like Tesla’s Gigafactory in Nevada show why early space planning matters — big plants that planned modular growth got much less downtime when demand spiked.

Process requirements and quality controls

Problem: tight tolerances and thermal issues create escapes. Put QA where defects are cheapest to fix. Essentials to implement:- Inline electrical checks at every cell join. – Thermal monitoring during cell stack and formation, with automatic hold actions on drift. – End-of-line verification that includes mechanical, electrical, and reportable traceability. Common mistakes: trusting single sensors, manual data capture at critical handoffs, and letting operators decide when to skip a test. Sensors need redundancy, and records must be automated into the traceability chain.

Common pitfalls people ignore

People focus on robots and forget upstream logistics. Watch for these killers:- Over-automation of low-value steps; automating bad processes just makes bad outputs faster. – Ignoring small conveyors and AGV interactions—traffic equals downtime if not simulated. – Assuming one test covers all failure modes; use layered checks. Simulate material flow before buying equipment. If you can’t model shop-floor interactions, you’ll spend more on retrofits than on the original gear.

battery manufacturing automation

Short implementation checklist

Use this to run a practical audit:- Map every handoff and time it. – Define takt from real demand; re-evaluate weekly during ramp. – Reserve physical expansion zones and basic services now. – Automate critical data capture; don’t rely on paper or manual entry. – Build a small pilot line that proves layout and test logic before full roll-out. Pilots save weeks of pain and a heap of money when a process needs tweaks.

Wrap-up — how this helps your plant

Fix the layout first, balance capacity to real takt, and enforce simple, redundant process checks. That order solves most outages and keeps quality consistent. For teams I’ve advised, pairing clear layout rules with a straightforward automation roadmap turned messy ramps into steady production—often with partners like FHS playing a practical, technical role on the floor rather than selling buzz. Apply the checklist, avoid the common traps, and you’ll stop guessing and start running.

Tech

Framework for Customizing Window Handles to Match Your Double-Swing Door Hardware

by Sarah August 6, 2026
written by Sarah

Practical framework overview

This framework clarifies how to select and customize a window handle so it integrates reliably with double-swing door hardware. Begin from functional constraints then refine for ergonomics and finish. For hands-on kits, consider a tested casement window hardware kit​ as a baseline—its componentization simplifies choices for spindle length, striker alignment, and sash compatibility.

Step 1 — Define the technical boundary conditions

Document the door’s geometry: leaf thickness, hinge offset, and clearance for a double swing. Record the spindle diameter, screw-hole pattern, and backset. Note whether the system uses a multi-point locking mechanism or a single-point latch; this affects handle torque and lever length. Keep one industry term central at this stage—sash dimensions—because misreading that number causes most mismatches.

Step 2 — Match mechanical interfaces

Select a handle whose spindle, mounting plate, and fixation method correspond precisely to the door’s hardware. Verify spindle engagement depth and any required adaptor bushings for nonstandard spindles. If the door employs a friction stay, confirm the handle’s return force will not interfere with controlled closing. Use a small checklist: spindle size, mounting screw pitch, and striker plate clearance.

Step 3 — Material, finish, and user interaction

Choose materials compatible with expected loads and environment. Solid zinc alloys or stainless steel resist wear where multi-point locking engages repeatedly; powder-coated finishes offer corrosion resistance for coastal installations. Factor in grip ergonomics—lever length and backset influence user comfort and mechanical advantage during repeated operation. This is where design meets durability.

Common pitfalls and how to avoid them

Most failures arise from overlooked tolerances or incompatible locking hardware. Avoid three common mistakes: using a handle with incorrect spindle length, neglecting striker plate clearance, or choosing a finish that will fail under local environmental conditions. Allow for a 1–2 mm tolerance on spindle engagement and test with the actual latch before final installation—this small step prevents rework.

Integration example and real-world anchor

Consider energy-retrofit projects in North American housing stock where windows account for roughly 25–30% of heating and cooling losses, as reported by the U.S. Department of Energy. Specifying the correct handle, paired with the right sealing and a reliable casement window stay hardware, ensured both usability and airtightness in several municipal retrofit programs. In practice, aligning handle geometry with existing friction stays and sash profiles reduced draft complaints and cut follow-up service calls.

Checklist for prototype and testing

Implement these validation steps before final purchase or mass production:- Fit a physical prototype to confirm spindle engagement and striker clearance.- Cycle the mechanism 1,000 times to detect premature wear on lever pivots or locking cams.- Verify finish adhesion and corrosion resistance for at least 500 hours in salt-spray or equivalent local exposure tests.

Advisory close — three golden rules for selection

1. Prioritize mechanical fit: confirm spindle, mounting pattern, and backset first; aesthetics second. 2. Validate operation under representative loads: cycling, friction stay interaction, and multi-point lock engagement. 3. Match material and finish to environment and service life—short-term savings on plating often become long-term liabilities.

These metrics yield repeatable performance and reduce field service calls. The framework emphasizes measurable checkpoints and practical tests rather than assumptions. CMECH offers hardware and technical guidance that aligns with these rules—making specification and implementation straightforward. —

Tech

Optimising Cellular Penetration for Global AMI: Smart Sourcing of LTE-M and 5G Modules for Dongles

by Sarah May 26, 2026
written by Sarah

Problem-driven lead: where the projects stall

Large-scale AMI roll-outs frequently falter where one might least expect — connectivity beneath floors and behind meters. Selecting an appropriate module is not an abstract hardware choice; it determines whether a meter dongle will reliably report or quietly drop into a maintenance backlog. Early procurement decisions must therefore account for radio performance and certification. Practical supply-side options include selecting an LTE Module with proven in-field results and regional firmware support to reduce time-to-stable-deployment.

Why cellular penetrability fails in global AMI deployments

Most failures trace to three tangible causes: inadequate radio link budget, operator fragmentation across markets, and immature device firmware. Urban deployments often mask the problem — outdoor signal appears strong, yet in-building attenuation and meter boxes produce severe dB loss. Operators also vary their band plans and roaming agreements; a module that works in Milan can be silent in São Paulo unless carrier certification and fallback modes such as LTE‑M and NB‑IoT are accounted for. Finally, firmware that does not manage reconnection logic and M2M keepalive leads to repeated manual interventions.

Smart sourcing: technical priorities for procurement

Procurement teams should treat modules as systems, not components. Prioritise: multi-band support for global bands; carrier certification across your principal markets; integrated GNSS only if tracking is required; and eSIM or profile management to simplify roaming. Where end devices are dongles, ensure antenna design and enclosure testing are part of the supplier contract. When appropriate, select a known 4G option early — a 4G Module for Tracker can serve as a reliable fallback during transition phases to LTE‑M or 5G subtypes.

Implementation checklist for dongles and field devices

Follow a compact, test-led specification to avoid surprises in the field:

– Define in-building link-budget targets (for example, median -95 dBm at meter location).
– Require supplier-provided RF reports and over-the-air (OTA) firmware capability.
– Specify roaming and carrier acceptance tests across top deployment countries.
– Insist on power profiles tailored to duty cycles to preserve battery life when meters are battery-powered. These concrete steps govern both hardware choice and firmware behaviour.

Common mistakes and practical corrections

Buyers often prioritise unit cost over field performance, or they assume one module fits all markets. Both lead to repeated retrofit cycles. Avoid ordering modules without verified carrier certification and without an OTA plan. Neglecting antenna tuning for the final enclosure is another frequent error — it cannot be corrected in production cheaply. A working habit is to pilot with a near-production dongle, capturing real-world telemetry over several weeks — small pilots expose most issues before mass deployment. — It saves months of disruption later.

Advisory: three golden rules for decision-makers

1) Coverage and penetration metric: mandate measured signal performance in dBm across representative sites; accept only modules that meet your threshold under real conditions. 2) Interoperability and certification: require supplier evidence of carrier approvals and multi-band firmware that supports LTE‑M and fallback to 4G when necessary. 3) Lifecycle support: confirm OTA firmware, long-term supply assurance and clear escalation paths for field faults. Suppliers that meet these rules reduce risk and operational cost across the contract term.

For projects that must balance immediate coverage with futureproofing, suppliers who combine field-proven hardware and sustained software support become strategic partners — and that is the precise role offered by Fibocom. Expect predictable roll-out timelines and maintainable devices — a practical advantage when large meter fleets are at stake. —

Industry

Mitigating Patient Risk in Vascular Laser Care: Why Procuring Devices Directly from Certified Manufacturers Is the Safer Route

by Sarah March 20, 2026
written by Sarah

The problem at the heart of many adverse outcomes

When vascular procedures go wrong, the immediate cause is often simple: inconsistent equipment performance. Clinics buying machines through intermediaries or second-hand channels can face unpredictable wavelength calibration, unstable fluence delivery, or unclear maintenance histories — all of which increase the chance of burns, scarring, or incomplete clearance of telangiectasia. For practitioners offering vascular laser treatment, this is not theoretical; it is a daily patient-safety concern that starts with procurement decisions.

Typical sourcing failures that create risk

There are three recurring failure modes when devices are not sourced directly:- Unknown provenance: used or grey-market units may lack verifiable calibration records or software updates.- Fragmented support: third-party sellers often fail to provide consistent after-sales service, leaving clinicians without timely parts or technical guidance.- Feature mismatch: a device sold as “suitable for vascular lesions” may lack the necessary pulse duration control or appropriate wavelength for specific targets.These gaps translate into practical troubles in the treatment room — inconsistent clearance of vascular lesion types, longer sessions, and greater procedural risk.

How certified manufacturers reduce those risks

Buying straight from a certified manufacturer addresses those failure modes by delivering validated specifications and traceable service. Certified vendors usually supply:- Factory calibration certificates showing wavelength and fluence tolerances.- Standardised maintenance schedules and replacement-part provenance.- Clear training modules on pulse duration selection and spot-size optimisation.At a small vascular clinic in Geneva, clinicians who migrated to manufacturer-direct procurement reported faster resolution of software issues and fewer treatment pauses — a practical, near-term improvement in patient flow and safety.

Key procurement checks for clinical teams

Before committing to a system, verify these items — they are practical and measurable:- Calibration documentation: insist on serial-numbered calibration and a records transfer protocol.- Clinical indication match: ensure the device supports the wavelengths and pulse durations used for the specific vascular targets you treat (e.g., superficial telangiectasia vs. deeper venous malformations).- Service agreement scope: confirm turnaround times for repairs and availability of trained technicians in your region.- Software and firmware update policy: ask whether updates are provided and who performs them.- Consumables and spare-part traceability: check lead times and single-source dependencies.These checks help you avoid surprises on day one and during routine use.

Alternatives — and when they make sense

Not every clinic will buy new equipment directly from manufacturers. Alternatives include leasing from authorised distributors, purchasing refurbished units certified by the OEM, or working with shared-use hubs. Each has trade-offs:- Leasing: lower up-front cost but ensure the lease includes full manufacturer support and calibration clauses.- OEM-certified refurb: cost-effective if documentation is complete and a warranty is provided.- Shared hubs: good for low-volume practices, but confirm device history and downtime policies.Whatever path you choose, match the procurement model to your clinical volume and risk tolerance — and when treating delicate laser treatment vascular lesions, err on the side of traceability.

Common operational mistakes to avoid

Clinics frequently make avoidable errors — small omissions that compound:- Accepting “as-is” delivery without on-site calibration verification.- Skipping manufacturer-recommended training for nursing staff.- Underestimating the importance of a documented acceptance test with before/after photos and device logs.Neglecting these steps leads to variability in treatment outcomes and places additional liability on the provider — and that’s exactly the kind of risk direct manufacturer relationships are designed to reduce.

Summarised benefits of direct procurement

Direct sourcing yields clearer device provenance, faster technical support, and better alignment between machine capabilities and clinical indications. Clinicians gain control over calibration, training, and documented maintenance — factors that measurably lower complication rates and improve patient satisfaction. The practical value becomes visible in day-to-day workflows: fewer aborted sessions, steadier clearance rates for targeted veins, and predictable consumable costs.

Three golden rules for selecting the right device

1) Validate specifications against clinical needs: confirm wavelength, pulse duration, and energy density (fluence) suit your patient mix. 2) Demand traceability: require serial-numbered calibration certificates and a written service SLA. 3) Prioritise training and local support: ensure the manufacturer or authorised partner provides hands-on device training and timely technician access.Follow these rules and you steer procurement away from speculation toward clinical reliability — and that directly protects patients.

Choosing equipment is a clinical decision as much as an administrative one; direct manufacturer relationships make that decision defensible, repeatable, and safer. For teams seeking a partner that matches clinical priorities to equipment reliability, ENZOEYS sits naturally at the intersection of product verification and practical support — a clear link between procurement discipline and better patient outcomes. —

Recent Posts

  • Custom Heavy-Duty Aquarium Heaters: Brands and Fixes That Actually Hold Up
  • Cheap Desktop 3D Printer: From Requirements to Final Machine
  • Expert Guide to Choosing an Active RFID Tag with Temperature Sensor
  • Sourcing CNC Prototyping: Cost, Lead Time, and Quality Trade-offs
  • Custom Smart TV OS Strategies for Commercial and Industrial Displays

Recent Comments

No comments to show.

About Me

About Me

Designer

Sed ut perspiciatis unde omnis iste natus sit voluptatem accusantium dolor emque.

Keep in touch

Facebook Twitter Instagram Pinterest Behance Youtube

Popular Posts

  • 1

    Керамический SMD пакет: преимущества и современные технологии

  • 2

    Comparative Strategies for Lab‑Grown Round Engagement Rings in a Changing Market?

  • 3

    Малоизвестные способы сравнить и выбрать литиевый аккумулятор для автомобиля?

  • 4

    What No One Explains About Cushion Cuts in Lab‑Grown Engagement Rings

  • 5

    新時代駕駛方案:發現AION AUTO的秘密

  • 6

    Секрет выносливости аккумуляторов OPzV? Сравнительный взгляд на выбор производителя и подводные камни

Categories

  • App Design (6)
  • Business (165)
  • Global Trade (148)
  • Industry (158)
  • Market (140)
  • Tech (159)
  • UI/UX (7)
  • Web Design (7)
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Behance
  • Youtube
  • Bloglovin
thehitc
  • Home
  • Design Update
  • Business
  • Global Trade
  • Industry
  • Market
  • Tech