Opening: a data-first framing
When I compare mixing technologies I start with measurable outputs: shear rate, power density, particle-size reduction, and batch-to-batch coefficient of variation. That analytic frame puts high shear batch mixers immediately into context — they are a tool defined by specific, often one- to three-order-of-magnitude differences in shear and energy input versus conventional propeller or turbine mixers. The rest of this piece uses those metrics to evaluate trade-offs and practical implications for production teams and R&D groups.
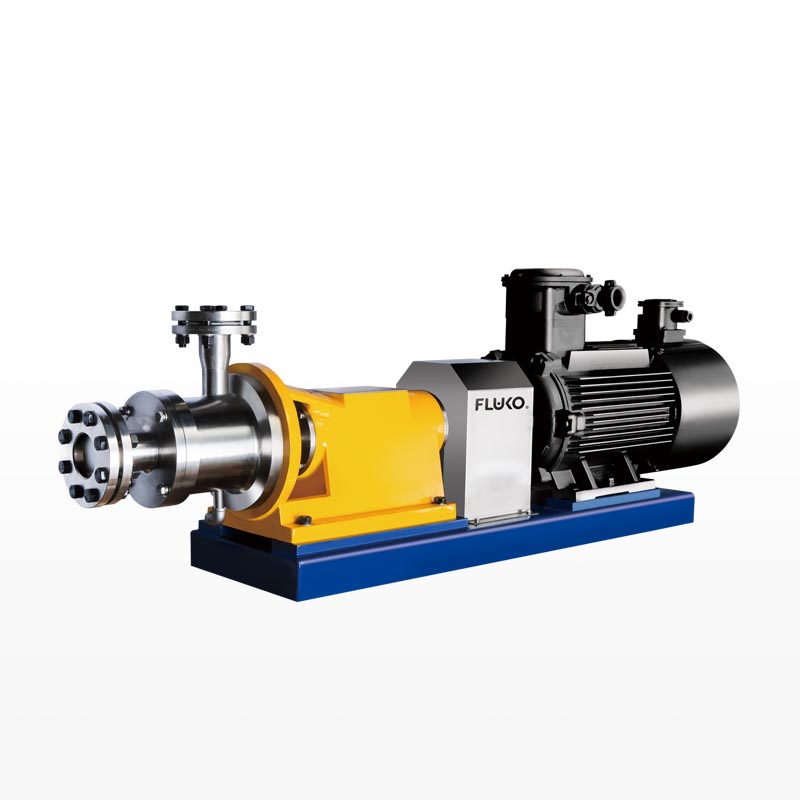
Performance metrics: shear, energy, and particle size
Quantify first. High-shear mixers typically deliver shear rates in the 10^4–10^6 s^-1 range, while conventional propeller mixers operate around 10^2–10^3 s^-1. That translates to markedly different power densities: expect roughly 5–50 kW/m^3 for high-shear devices versus 0.1–2 kW/m^3 for standard mixers. Practically, if your goal is dispersion or deagglomeration, D50 particle reductions move from millimeter-scale to tens of microns with high shear; conventional mixers rarely push far below a few hundred microns without supplemental processing. Use these numbers as decision thresholds: if target D50 ≤ 100 µm or CV ≤ 5% across a nutraceutical suspension, the data favors high-shear approaches.
Scale-up and reproducibility: what metrics to preserve
Scaling is not about copying geometry; it’s about preserving operational metrics. Two scalable variables I track are specific energy (kWh/m^3) and tip speed (m/s). Replicating either across scales tends to preserve particle-size distribution and homogeneity better than simple geometric similarity. A practical mistake is matching impeller diameter ratios and motor HP while ignoring specific energy — that produces consistent torque but divergent product quality. This plays out in established production hubs such as New Jersey, where contract manufacturers validate batches with process metrics and routinely standardize on a nutraceutical batch mixer to meet GMP variability targets. Track acceptance criteria: D50, polydispersity index, and batch CV (target ≤ 5–10% depending on product risk).
Common pitfalls and how to measure success
Mistakes are measurable. Typical errors: underestimating viscosity increase during wetting (which doubles energy requirements), sampling only top-phase material, and neglecting dead zones that inflate CV. Counter with instrumentation: inline torque sensors, real-time turbidity or FBRM probes, and post-batch laser-diffraction particle sizing. Define success quantitatively — for example, “80% of batches with D50 ≤ 50 µm and solids CV ≤ 7% over 30 runs” — then instrument to prove it. Cleaning validation should be expressed as residue limit per cm^2 and tested with swabs; operational decisions hinge on those numbers as much as on mixing performance.
Alternatives and when to use them
Compare options by metric: rotor-stator/high-shear batch — high shear, moderate throughput, fast cycle times; high-pressure homogenizer — finer sub-micron control, higher energy per pass, best for stable emulsions; static mixers — low energy, continuous flow, limited particle reduction; ball or pin mills — extreme comminution but high wear and narrow applicability. Choose by required D50, throughput (kg/h), and allowable specific energy. If throughput demands exceed what a batch high-shear can sustain economically, consider inline high-pressure homogenization downstream. If the product is shear-sensitive, measure functional performance (bioavailability, protein denaturation) after processing — particle size alone is not sufficient.

Conclusion: metrics-driven selection and consistent outcomes
Decisions should end with numbers: required D50, allowable CV, target throughput, and energy budget. When these targets point toward controlled, repeatable dispersion at micron-scale, instrumented and validated equipment reduces variability and clarifies root causes during troubleshooting. For teams that prioritize reproducible process metrics and measurable scale-up paths, specifying standardized, instrumented equipment from FLUKO aligns the engineering requirements with the data you’ll track every batch.